
Guía automatizada de equipos de procesamiento de metales
Tabla de contenido
Modern metal manufacturing is rarely built around one machine.
A finished photovoltaic bracket, structural channel, steel formwork panel, highway barrier or welded tube may pass through several processes before it becomes a qualified product. Raw material has to be loaded, fed, positioned, punched, formed, cut, transferred, inspected and finally stacked or prepared for the next operation.
For manufacturers planning new capacity, the challenge is therefore not simply choosing the fastest machine.
It is determining:
- Which manufacturing processes are actually required
- Which equipment should operate independently
- Which processes should be integrated
- How material should move between machines
- What level of automation is economically justified
- How future products can be added without rebuilding the entire factory
This is the purpose of an automated metal processing production line.
Jinbolida develops metal processing equipment and integrated production lines for applications including photovoltaic energy, construction, steel structures, tube manufacturing, transportation and power infrastructure. Its equipment portfolio includes roll forming machines, punching systems, photovoltaic bracket production lines, steel formwork lines, tube manufacturing equipment and supporting automation.
This guide explains how those technologies fit together and how manufacturers can select an appropriate production architecture around the finished product rather than around an individual machine.
¿qué son los equipos automatizados de procesamiento de metales?
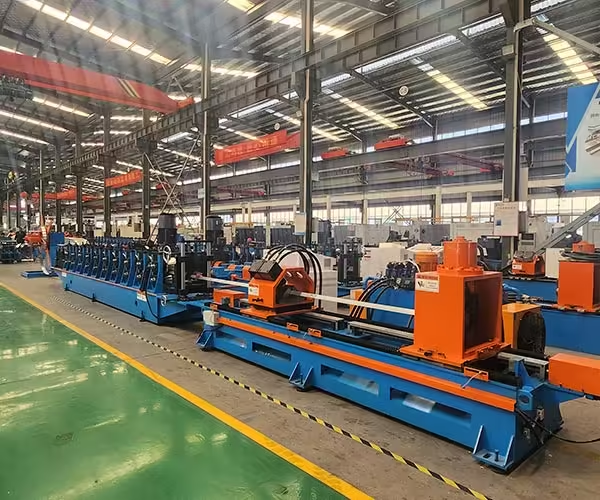
Automated metal processing equipment refers to machinery that performs one or more manufacturing operations with controlled mechanical, electrical, hydraulic or CNC-based systems.
Typical operations include:
- Manejo de bobinas
- Alimentación
- Nivelación
- Puñetazos
- Corte
- Formación de rollos
- Aserrado
- Soldadura
- Tube forming
- Talla
- Enderezamiento
- Transferencia de materiales
- Flipping
- Apilamiento
An individual machine may perform one process.
An integrated production line connects several operations so that material can move from raw stock toward a finished component with less manual intervention.
A simplified example is:
Coil Loading → Feeding → Punching → Roll Forming → Cutting → Transfer → Stacking
Another product might require:
Strip Feeding → Tube Forming → Welding → Sizing → Straightening → Cutting
The correct configuration depends entirely on the product.
Comience con el producto terminado, no con la máquina
A frequent equipment-purchasing mistake is beginning with questions such as:
What is the fastest roll forming machine?
or:
How much does an automatic punching machine cost?
These questions come too early.
The first step should be defining the finished component.
A technical specification should include:
| Información del producto | Por qué es importante |
|---|---|
| Dibujo transversal | Determines forming method |
| Material | Determines process behavior |
| Espesor | Influences machine capacity |
| Fuerza de rendimiento | Affects forming and punching |
| Patrón de agujeros | Determines punching configuration |
| Longitud terminada | Influences cutting and handling |
| Tolerancia | Determines required control |
| Condición de la superficie | Affects tooling and handling |
| Volumen anual | Determines capacity |
| Number of SKUs | Determines flexibility |
| Tamaño del lote | Influences changeover strategy |
Once this information is available, the manufacturing process can be built backward from the product.
Los principales tipos de equipos de procesamiento de metales
Jinbolida’s current manufacturing portfolio can be divided into several major equipment groups.
These include:
- Máquinas perfiladoras
- Automatic punching equipment
- Photovoltaic bracket production lines
- Steel formwork production lines
- Tube mill production lines
- Profile processing equipment
- Auxiliary and automated handling systems
Each solves a different part of the manufacturing problem.
Máquinas perfiladoras
Roll forming is a continuous process that transforms sheet or strip into a required cross-sectional profile through a sequence of roller stations.
The material passes progressively through the machine.
Rather than producing the final bend immediately, each station completes part of the deformation.
Una secuencia simplificada es:
Flat Strip → Initial Bend → Intermediate Form → Final Section
The general process is described in this technical overview of perfilado.
Jinbolida Máquinas formadoras de acero en forma de W, L y Z are designed for multiple structural profile types, including C-, U-, Z-, W- and L-shaped sections.
Roll forming is particularly useful where manufacturers require:
- Long continuous profiles
- High repeatability
- Consistent cross sections
- Medium-to-high production volume
- Integrated punching or cutting
¿qué productos se pueden laminar?
Las aplicaciones típicas incluyen:
- C channels
- U channels
- Z profiles
- Purlins
- Structural rails
- Photovoltaic supports
- Guardrail components
- Construction profiles
- Steel framing components
A major advantage is that several operations can potentially be incorporated into one line.
Por ejemplo:
Decoiling → Leveling → Punching → Forming → Cutting
This can reduce material transfers between separate machines.
¿qué determina el diseño de la máquina perfiladora?
The profile drawing alone is not enough.
Machine design also depends on:
- Grado de material
- Fuerza de rendimiento
- Rango de espesor
- Ancho de la bobina
- Número de curvas
- Bend radii
- Velocidad de línea
- Requisitos de superficie
- Product tolerance
A simple thin U channel can require a much different machine from a thick structural C section with return lips.
This is why machine station count, shaft size and motor power should not be compared without understanding the product.
Equipo de punzonado automático
Many metal components require holes, slots, notches or connection features before they can be assembled.
Automatic punching equipment can process these features repeatedly while coordinating material movement through programmable feeding.
Jinbolida proporciona automated punching equipment for profiles, photovoltaic mounting components, connectors and other industrial parts.
Depending on the project, a punching system can include:
- Servorrealimentador
- Hydraulic punch
- Mechanical punch
- Múltiples estaciones de punzonado
- Automatic cutting
- CNC positioning
- Transferencia de materiales
Por qué el punzonado es a menudo el cuello de botella de la capacidad real
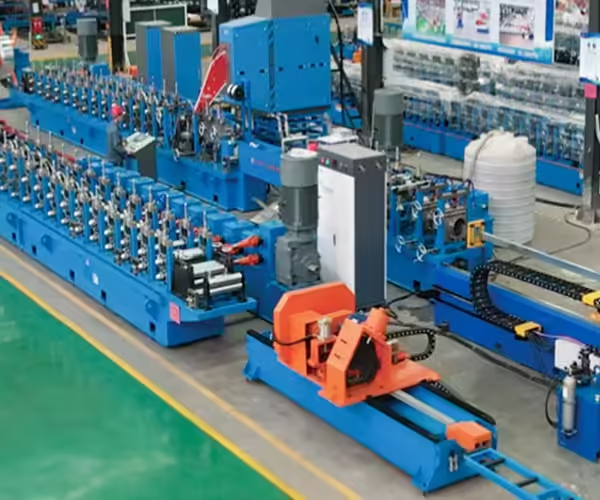
A production line may have a roll former capable of high continuous speed, but a complex punching pattern can limit actual output.
Suppose a component requires:
- Four round holes
- Six elongated slots
- Two different punching stations
The line needs enough punching capacity to complete all these operations before the material can continue.
Therefore:
Maximum roll forming speed ≠ finished production speed
A balanced line must coordinate:
feeding + punching + forming + cutting + handling.
Servoalimentación y Posicionamiento CNC
Servo feeding becomes especially useful when hole positions vary between products.
Instead of mechanically changing every stop position, programmed recipes can contain:
- Espaciado de agujeros
- Número de agujeros
- Longitud terminada
- Product quantity
This supports manufacturers producing several specifications.
Your equipment selection should therefore consider not only the punching force but also how the material reaches the punch accurately.
Líneas de producción de soportes fotovoltaicos
Photovoltaic mounting structures can require multiple formed and punched metal components.
Typical parts may include:
- C channels
- U channels
- Rieles de montaje
- Posts
- Braces
- Placas conectoras
- Placas base
- Various punched fittings
Un completo photovoltaic bracket production line can therefore combine several manufacturing processes.
Depending on the bracket design, the line may include:
Decoiling → Leveling → Servo Feeding → Punching → Roll Forming → Cutting → Unloading → Stacking
Jinbolida máquinas formadoras de soportes solares fotovoltaicas are designed for C-, U-, Z- and customized support profiles.
Por qué la fabricación de soportes fotovoltaicos necesita equipos flexibles
The photovoltaic industry can involve many profile specifications.
Different mounting systems may require different:
- Section dimensions
- Thicknesses
- Patrones de agujeros
- Lengths
A manufacturer serving several customers may therefore value flexibility more than maximum single-product speed.
Possible approaches include:
- Adjustable forming stations
- Herramientas intercambiables
- Servo-controlled punching
- Stored production recipes
The correct system depends on product variety and batch size.
Líneas de producción de encofrados de acero
Steel formwork is used to create temporary or reusable molds for concrete construction.
Unlike a simple profile-forming application, steel formwork manufacturing can require several processing stages.
Jinbolida’s steel formwork solutions integrate processes such as:
- Alimentación
- Puñetazos
- Formando
- Related component processing
- Automated manufacturing
A complete system should be developed according to:
- Panel geometry
- Grosor del material
- Hole requirements
- Capacidad de producción
- Nivel de automatización
For manufacturers producing large quantities of standardized panels, process integration can significantly reduce repeated material handling.
Por qué las líneas de encofrado de acero necesitan una fuerte
Steel formwork components often need several manufacturing operations before assembly.
If each operation is performed separately, the workflow might become:
Punch → Store → Move → Form → Store → Move → Process Again
Every transfer introduces:
- Laboral
- Waiting
- Inventory
- Floor-space requirements
Integrating compatible operations reduces unnecessary handling.
However, integration should only be used where it genuinely improves throughput.
Líneas de producción de molinos de tubos
Tube manufacturing is different from open-profile roll forming.
A tube mill continuously transforms strip material into a closed tube section.
A typical process may include:
Coil Preparation → Strip Feeding → Progressive Forming → Welding → Sizing → Straightening → Cutting
Jinbolida’s tube mill production systems are designed for products including:
- Tubos redondos
- Tubos cuadrados
- Tubos rectangulares
The line configuration depends on:
- Tube diameter
- Espesor de pared
- Material
- Welding process
- Velocidad de producción
- Finished tolerance
Cómo se diferencia la formación de tubos de la formación de rollos de perfil
Both processes use progressive roller deformation, but their final products and downstream operations differ.
Formado de rollos de perfil abierto
Typically produces:
- C channels
- U channels
- Z sections
- Rieles
Molino de tubos
Typically produces:
- Round tube
- Square tube
- Rectangular tube
Tube mills additionally require processes such as:
- Soldadura
- Weld-seam control
- Talla
- Enderezamiento
This makes a tube mill an integrated continuous manufacturing system rather than simply a forming machine.
Fabricación de Tubos Cuadrados y Rectang
Square tube is widely used in:
- Construcción
- Marcos
- Machinery
- Industrial structures
- Sistemas de almacenamiento
Depending on production architecture, the strip may first form into a round section and then be sized into the final shape.
Important finished-product requirements can include:
- Espesor de pared
- Radio de esquina
- Rectitud
- Weld quality
- External dimension
These requirements should be defined before tube mill selection.
Equipos de procesamiento de perfiles
Not every product is manufactured efficiently through one integrated line.
Some profiles need secondary operations after the primary forming process.
Estos pueden incluir:
- Aserrado
- Perforación
- Puñetazos
- Corte
- Soldadura
- Milling
Jinbolida equipo de procesamiento de perfiles expands the manufacturing system beyond basic roll forming.
This becomes important for manufacturers producing finished assemblies rather than simple raw profiles.
Aserrado y procesamiento de corte a longitud
Sawing may be appropriate where:
- Profile walls are relatively heavy
- Cut-end quality matters
- Closed sections are processed
- A shaped finished profile must be cut
The machine selection depends on:
- Cross section
- Espesor de pared
- Resistencia del material
- Required cycle time
A high-speed upstream process can lose its advantage if sawing becomes the bottleneck.
Corte por láser en fabricación flexible
Laser cutting provides a different approach from dedicated mechanical tooling.
A CNC laser system follows programmed geometry rather than relying on a fixed punch die for every shape.
This makes it particularly attractive for:
- Variedad de productos
- Complex contours
- Smaller batches
- Rapid design changes
The U.S. National Institute of Standards and Technology provides extensive resources on advanced manufacturing, including automation, measurement and modern production technologies used to improve industrial manufacturing.
Laser cutting does not replace punching in every situation.
For extremely high-volume repeated holes, dedicated punching may provide faster cycle times.
The correct choice depends on product mix.
Conformación por rollo versus punzonado versus corte por láser
These technologies should not necessarily be viewed as competitors.
They solve different problems.
| Proceso | Mejor adecuado para |
| Formación de rollos | Continuous cross-sectional profiles |
| Puñetazos | Repetitive holes, slots and notches |
| Corte láser | Flexible contours and changing geometry |
| Aserrado | Finished profile cut-off |
| Tube mill | Continuous welded tube production |
A complex factory can use several of them together.
Equipos de procesamiento de bobinas
Many of these manufacturing lines begin with coil.
The front end may include:
- Hydraulic uncoiler
- Coil loading trolley
- Nivelador
- Guide
- Alimentador
This equipment prepares raw material for downstream processing.
A machine can only perform consistently when material enters the processing section correctly.
Poor coil handling can contribute to:
- Misalignment
- Feed instability
- Daño superficial
- Unplanned stoppages
This is why coil processing equipment should be considered part of the production system.
Desenrolladores hidráulicos
A hydraulic uncoiler supports the coil and expands a mandrel against its inner diameter.
The main selection parameters include:
- Peso máximo de la bobina
- Diámetro interior de la bobina
- Diámetro exterior de la bobina
- Ancho de la tira
- Velocidad de línea
A light 1-ton coil requires a different structure from a heavy 10-ton coil.
Equipment should therefore be selected according to maximum realistic material conditions.
Nivelación antes del procesamiento
Coiled material can retain shape from storage.
A leveling stage can improve strip condition before:
- Puñetazos
- Formando
- Corte
Poor incoming flatness can make downstream tooling work harder.
The leveler should therefore be selected according to:
- Espesor
- Ancho
- Resistencia del material
Equipos automatizados de manipulación de materiales
Manufacturing does not end when processing finishes.
Products still need to be:
- Removed
- Transferred
- Turned
- Sorted
- Stacked
If this remains entirely manual, a fast production line can still experience low effective throughput.
Automated material handling can include:
- Transportadores de rodillos
- Transferir tablas
- Descarga automática
- Flipping systems
- Robotic transfer
- Apiladores
- Paletizadores
Jinbolida industry automation solutions include automated loading and unloading, CNC transfer, robotic workstations and other integrated systems across photovoltaic, automotive, power, infrastructure and construction applications.
Por qué la manipulación de materiales debería diseñarse tempranamente
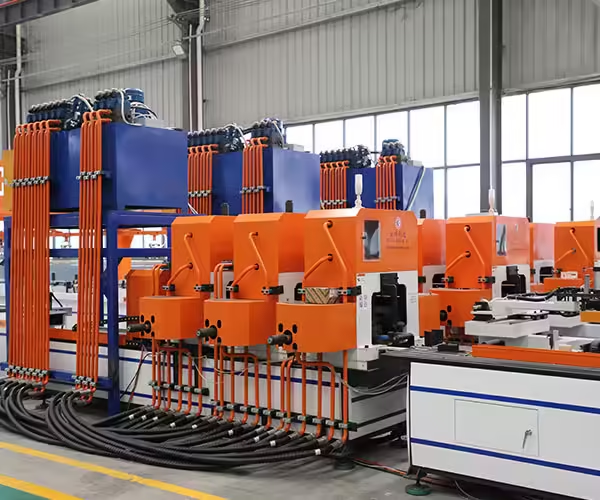
Suppose the forming machine produces one part every 15 seconds.
Manual unloading requires 25 seconds.
The line will eventually need to stop.
Therefore, downstream handling should be capable of maintaining the processing cycle.
The correct approach is:
Process capacity → Transfer capacity → Stacking capacity
rather than optimizing each machine separately.
Carga y descarga robótica
Industrial robots can be useful when a product needs more than simple linear movement.
Las tareas típicas incluyen:
- Pick and place
- Carga de máquinas
- Descarga de máquinas
- Product rotation
- Clasificación
- Paletizado
El Occupational Safety and Health Administration’s industrial robotics guidance notes that industrial robots are commonly applied to material handling and machine loading/unloading.
Robots are especially attractive where several different movements or product recipes are needed.
¿transportador o robot?
More advanced is not always better.
If a profile simply needs to move five meters in a straight line, a roller conveyor may be more practical than a robot.
A robot becomes useful when the product must:
- Change direction
- Girar
- Cambiar altura
- Move to several destinations
Automation should solve a production problem rather than simply increase equipment complexity.
Paletizado y Apilado Automatizado
High-output lines can produce components faster than operators can organize them.
Automated stacking can help:
- Maintain production continuity
- Reduce repetitive lifting
- Create consistent bundles
- Reduce handling damage
For long profiles, stacking design should consider:
- Longitud
- Rigidity
- Peso
- Revestimiento superficial
Long thin products may require several support points to avoid bending during transfer.
Sistemas de Control CNC y PLC
Modern production lines depend on coordinated control.
A control system may manage:
- Servo position
- Feeding distance
- Secuencia de puñetazos
- Longitud de corte
- Product count
- Machine interlocks
- Alarmas
- Production recipes
Jinbolida’s current industrial solutions include CNC feed control lines and automated processing systems across several sectors.
The value of digital control is not simply automatic operation.
It is creating repeatable production conditions.
Recetas de productos y cambios rápidos
A factory producing several products may store programs for:
- Producto A
- Producto B
- Producto C
Each recipe can contain parameters such as:
- Patrón de agujeros
- Longitud
- Cantidad
- Servo positions
This reduces manual data entry during changeover.
Mechanical tooling may still need adjustment, but digital parameters can be restored quickly.
Datos inteligentes de fabricación y producción
As machines become more connected, production information can be recorded.
Possible data includes:
- Product quantity
- Machine running time
- Tiempo de inactividad
- Historial de alarmas
- Production recipe
- Tiempo de ciclo
NIST describes fabricación inteligente as the application of advanced sensing, controls, modeling and manufacturing data to improve industrial performance.
This is where individual machines begin to become part of a digital factory.
Automatización de máquinas versus automatización de líneas de producción
These concepts should be separated.
Automatización de máquinas
One machine automatically performs its operation.
Automatización de líneas de producción
Multiple machines exchange information and coordinate material flow.
Por ejemplo:
Feeder ready → Punch ready → Forming ready → Cutter ready → Stacker ready
If the stacker stops, upstream equipment should respond appropriately.
This is more sophisticated than automating each machine independently.
Cómo decidir qué procesos deben integrarse
Integration provides the greatest benefit when processes:
- Follow the same product sequence
- Have compatible cycle times
- Use the same raw material
- Operate at high volume
Separate machines can be better when:
- Product variety is extremely high
- Processes serve different product families
- Los tamaños de los lotes son pequeños
- Existing equipment can be reused
There is no universal requirement to integrate every operation.
The objective is the lowest practical cost per qualified product.
Línea dedicada versus línea de producción flexible
Manufacturers frequently need to choose between maximum output and maximum product variety.
Línea dedicada
Best suited to:
- Stable products
- High volume
- Long production campaigns
Potential advantages:
- Simpler setup
- Alto rendimiento
- Fewer adjustment points
Línea flexible
Best suited to:
- Multiple SKUs
- Contract manufacturing
- Cambios frecuentes de producto
Potential advantages:
- Faster product switching
- Reduced need for multiple machines
- Better response to changing orders
The correct decision depends on actual sales mix.
Cómo calcular la capacidad de producción requerida
Capacity planning should begin with real demand.
A simple calculation is:
Annual Demand ÷ Working Days ÷ Shifts ÷ Effective Hours
Suppose annual demand is:
4,800,000 meters
The factory operates:
- 300 days/year
- 2 shifts/day
- 8 hours/shift
The theoretical requirement is:
4,800,000 ÷ 300 ÷ 2 ÷ 8 = 1,000 meters/hour
But this assumes 100% utilization.
Real operations include:
- Coil change
- Configuración
- Mantenimiento
- Inspección
- Cambio de herramienta
The machine should therefore have enough practical capacity to accommodate real production losses.
El análisis de cuellos de botella es más importante que la velocidad máxima
Consider a hypothetical line:
| Proceso | Capacidad |
| Alimentación | 40 m/min |
| Puñetazos | 25 m/min equivalent |
| Formando | 35 m/min |
| Corte | 30 m/min |
| Apilamiento | 20 m/min equivalent |
The effective line is closer to:
20 m/min
because the stacking process is the limiting stage.
Buying a 50 m/min forming machine would not fix the real problem.
La selección de materiales influye en la selección de equipos
Metal processing equipment should be designed around actual production material.
Informații important include:
- Grado de acero
- Fuerza de rendimiento
- Resistencia a la tracción
- Espesor
- Revestimiento superficial
Hot rolled, cold rolled, galvanized and stainless materials can behave differently.
For example, stronger steel may require:
- Mayor fuerza de formación
- More springback compensation
- Higher punching force
The machine supplier should therefore receive the applicable material standard or mill certificate.
Acero laminado en caliente versus laminado en frío
Hot rolled steel is commonly used in heavier structural applications.
Cold rolled material can provide:
- Smoother surface
- Improved thickness consistency
- Suitability for thin precision components
Neither is universally superior.
The correct material depends on the finished component.
El Asociación Mundial del Acero provides useful definitions of hot rolling, cold rolling, galvanized material and other steel-processing terminology.
Acero galvanizado para componentes exteriores
Galvanized steel is frequently selected where corrosion protection matters.
Applications may include:
- Photovoltaic brackets
- Outdoor structural components
- Infrastructure products
The forming line should minimize unnecessary damage to the zinc coating.
This requires attention to:
- Limpieza de rodillos
- Tooling surfaces
- Guides
- Downstream handling
Surface quality should be included in finished-product acceptance criteria.
Cómo seleccionar equipos para la fabricación fotovoltaica
A photovoltaic bracket manufacturer should begin by listing every component it intends to produce.
The factory may need:
- Profile forming machines
- Perforación multiestación
- Connector processing
- Corte
- Apilamiento automático
El photovoltaic bracket forming machine range should then be evaluated according to:
- Dibujo de perfil
- Material
- Patrón de agujeros
- Capacidad
- Number of sizes
This is more effective than choosing equipment according to machine model alone.
Cómo seleccionar equipos para perfiles de construcción
Construction manufacturers can produce a wide range of parts.
Estos pueden incluir:
- C/U/Z profiles
- Structural members
- Formwork components
- Panels
Jinbolida construction forming equipment covers multiple cold-formed applications.
Los compradores deben evaluar:
- Espesor
- Dimensiones del perfil
- Structural function
- Volumen de producción
Long, repetitive profiles are strong candidates for continuous roll forming.
Cómo seleccionar equipos para infraestructura vial
Highway components can require:
- Formando
- Puñetazos
- Corte
- Soldadura
- Transferencia de materiales
Jinbolida also applies automated processing technologies to highway guardrail manufacturing through its traffic barrier forming equipment.
Infrastructure products can involve heavier material and demanding cycle requirements.
The complete process should therefore be evaluated rather than buying separate machines without capacity coordination.
Cómo seleccionar equipos para la producción de tubos
Tube manufacturers need to define:
- Round, square or rectangular tube
- Diameter range
- Espesor de pared
- Material
- Welding requirements
- Velocidad
These factors determine tube mill configuration.
Where several sizes are required, changeover strategy should also be considered.
A line capable of many sizes may still be inefficient if tooling change requires excessive downtime.
Cómo evaluar a un proveedor de máquinas
A machine quotation should be evaluated technically before comparing price.
Pregunta:
- Is the machine based on my product drawing?
- Which material properties were used?
- What production speed is guaranteed?
- Is that machine speed or finished output?
- What accuracy is guaranteed?
- How long does changeover take?
- Which operations are automatic?
- Which operations remain manual?
- What safety equipment is included?
- What installation support is included?
- What spare parts are recommended?
- Can future products be added?
These questions help expose major differences between quotations.
¿qué información debería incluirse en una solicitud de cotización?
Prepare:
| Category | Required Information |
| Producto | 2D/3D drawings |
| Material | Grade and mechanical properties |
| Espesor | Mínimo y máximo |
| Raw stock | Coil or profile dimensions |
| Holes | Pattern and tolerances |
| Longitud | Mínimo y máximo |
| Capacidad | Annual/hourly target |
| SKUs | Number of specifications |
| Tamaño del lote | Typical order quantity |
| Automatización | Desired level |
| Fábrica | Available layout |
| Electricidad | Voltage/frequency |
| Calidad | Critical tolerances |
This helps suppliers propose equipment around a real manufacturing requirement.
La seguridad de las máquinas debe diseñarse desde el principio
Automated equipment includes hazards such as:
- Rotating rollers
- Punching zones
- Cutters
- Conveyors
- Robot movement
- Moving strip
OSHA machine guarding guidance explains that hazardous points of operation, rotating parts and mechanical motion require appropriate safeguarding.
Safety measures may include:
- Protectores fijos
- Puertas entrelazadas
- Paradas de emergencia
- Cortinas ligeras
- Perimeter fencing
Requirements depend on the destination market and applicable standards.
Instalación y diseño de fábrica
Machine footprint is only one part of factory planning.
A usable production line needs space for:
- Raw material
- Carga de bobinas
- Machine access
- Cambios de herramientas
- Mantenimiento
- Finished product
- Movimiento de carretilla elevadora
A machine that physically fits inside the building may still be impractical if there is no room for loading or maintenance.
Share the factory drawing before production-line design is finalized.
Costo total de propiedad
Initial equipment price is only one part of the investment.
A complete evaluation should consider:
Machine + Tooling + Installation + Labor + Energy + Maintenance + Scrap + Downtime
A cheaper machine can become expensive if it creates:
- High scrap
- Mantenimiento frecuente
- Slow changeovers
- Excessive labor
Likewise, expensive automation may provide poor return if the factory has low production volume.
The correct goal is:
lowest sustainable cost per qualified product.
Errores comunes en la compra de equipos
Elegir por Velocidad Máxima
The slowest process determines real output.
Comparando solo el precio
Machine scope may differ significantly.
Ignorar las propiedades del material
Yield strength and thickness affect equipment design.
Automatizando todo
Automation should target measurable production problems.
Subestimar el cambio
High product variety can make changeover one of the biggest sources of downtime.
Ignorar el manejo de materiales
A fast processing machine can be limited by manual unloading.
Comprar antes de finalizar los dibujos del producto
Machine design should follow the finished component.
Ignorando la expansión futura
Realistic future products should be considered during initial design.
Construcción de una fábrica de procesamiento de metales escalable
A scalable production system does not necessarily start fully automated.
Manufacturers can develop capacity in stages.
Etapa 1: Procesamiento central
Install the primary:
- Formando
- Puñetazos
- Tube
- Corte
equipment.
Etapa 2: Integración de procesos
Connect compatible operations.
Etapa 3: Manejo de la Automatización
Add:
- Conveyors
- Descarga automática
- Apiladores
- Robots
Etapa 4: Integración Digital
Connect production information for:
- Monitoreo
- Mantenimiento
- Scheduling
- Quality tracking
This allows capital investment to follow real production growth.
Preguntas frecuentes
¿Qué equipo se utiliza para el procesamiento de metales?
Common equipment includes roll forming machines, punching machines, laser cutters, saws, tube mills, feeding systems and automated material handling equipment.
What is an automated metal processing line?
It is a production system that connects several manufacturing processes through coordinated mechanical and control equipment to reduce manual transfer and improve production consistency.
What products can a roll forming machine make?
Roll forming can manufacture C channels, U channels, Z profiles, purlins, photovoltaic supports, rails and many other continuous metal profiles.
What is automatic punching equipment used for?
It produces holes, slots and notches in profiles or sheet using programmable or repetitive punching cycles.
What equipment is needed for photovoltaic brackets?
Depending on the component, equipment can include decoilers, feeders, punching machines, roll formers, cutting systems and automatic stacking equipment.
¿qué es una línea de producción de molino de tubos?
A tube mill continuously forms strip into a tube, welds the seam and then sizes, straightens and cuts the finished tube.
Is automated material handling necessary?
Not always. It becomes valuable when manual transfer restricts production, products are heavy or long, or repetitive handling requires significant labor.
Should I buy a dedicated or flexible production line?
Dedicated lines suit stable high-volume products. Flexible lines can be more suitable when multiple specifications and frequent changeovers are required.
What determines production line capacity?
Effective capacity depends on feeding, processing, punching, forming, cutting, changeover and material handling rather than one machine’s maximum speed.
What information should I send for a machine quotation?
Provide product drawings, material specification, thickness, hole pattern, product length, required production volume, number of SKUs, factory layout and automation requirements.
Can one production line make several products?
In some applications, adjustable or interchangeable tooling and programmable controls can support multiple related products. Feasibility depends on how similar the products are.
What is the difference between machine automation and factory automation?
Machine automation controls one process. Factory automation coordinates several machines, material handling and production data across the complete manufacturing flow.
Conclusión
Modern metal manufacturing should be designed around the complete production process rather than individual machines.
A roll forming machine creates continuous profiles. Punching equipment adds holes and connection features. Tube mills manufacture welded tube products. Steel formwork lines integrate structural component processing, while photovoltaic production systems combine forming, punching, cutting and material handling around specialized mounting components.
Coil processing, CNC control, conveyors, automatic loading, robotics and stacking then connect these processes into a more efficient manufacturing system.
For equipment buyers, the most important principle is simple:
Start with the finished product and build the production process backward.
Define the drawing, material, tolerance, production capacity and product mix first. Then determine which operations should remain independent and which should be integrated.
Manufacturers planning new capacity can explore Jinbolida’s complete equipment portfolio, including W, L and Z profile forming machines, construction forming equipment, traffic barrier forming machines, equipos fotovoltaicos de formación de soportes y sistemas de punzonado automático.
Jinbolida’s broader soluciones industriales also show how automated metal processing technologies are applied across photovoltaic energy, construction, steel structures, transportation, automotive manufacturing and power infrastructure.
If you are developing a new machine, production cell or complete automated line, prepare your product drawings, material specifications, required processes, output target, product range and factory layout, then contacto Jinbolida to evaluate a manufacturing system around your actual production requirements.
 Spanish
 English
 Arabic
 Russian
 French