
Capacité de la machine du moulin à tubes : un guide d'achat pratique
Table des matières
A tube mill machine is often promoted by its maximum line speed, but line speed alone does not tell buyers how many saleable tubes the production line can manufacture. Real output depends on tube size, wall thickness, material grade, coil changes, welding stability, cutting speed, tooling adjustments, maintenance, and quality-control requirements.
Before investing in a new production line, manufacturers should calculate practical production capacity rather than relying only on the maximum speed shown in a quotation.
Principaux points à retenir :
- Maximum forming speed is not the same as actual finished-tube output.
- Tube diameter, profile shape, and wall thickness affect stable production speed.
- Coil loading, strip joining, and size changes create planned downtime.
- Welding quality may become the main production limit at higher speeds.
- Cutting and unloading equipment must match the tube mill machine output.
- Buyers should calculate capacity by shift, product mix, and acceptable yield.
- Automatic controls can improve consistency but do not eliminate process bottlenecks.
- A production trial using the buyer’s material is more useful than a no-load demonstration.
Quelle est la capacité de la machine du broyeur à tubes
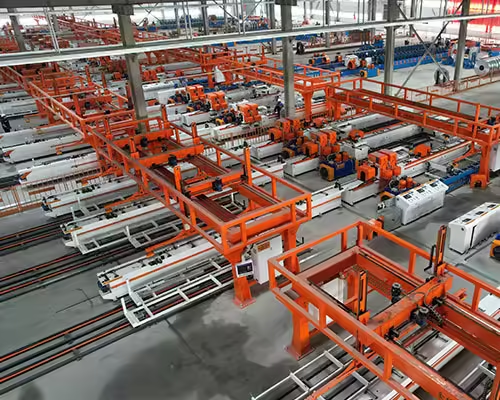
Tube mill machine capacity describes how much acceptable finished tubing a production line can manufacture within a defined period. It may be expressed in meters per minute, meters per shift, tons per month, or finished pieces per hour.
Each measurement answers a different purchasing question. Buyers should therefore ask suppliers to present capacity in a format that reflects their actual orders.
Vitesse de ligne
Line speed is the rate at which the strip passes through the forming and welding sections. It is usually expressed in meters per minute.
This figure is useful for comparing similar machines, but it does not include coil changes, setup time, equipment adjustments, inspections, or unplanned stops.
Sortie du tube fini
Finished output measures the quantity of acceptable tubes produced after welding, sizing, cutting, inspection, and unloading. This is more relevant to production planning because defective or unfinished tubes cannot be counted as saleable capacity.
Capacité de production mensuelle
Monthly capacity estimates the total output across the available shifts and working days. It must account for equipment utilization, product changes, maintenance, scrap, and actual operating efficiency.
Capacité nominale par rapport à la capacité pratique
Rated capacity represents output under specified or ideal conditions. Practical capacity reflects normal factory conditions and is usually lower because daily production includes both operating and non-operating time.
Comment fonctionne une machine de broyeur de tubes ?
A tube mill machine converts metal coil into continuously welded tubes or hollow sections. The strip passes through several coordinated stages before it becomes a finished product.
Understanding these stages helps buyers identify where production limitations may occur.
Chargement et déroulement de la bobine
The process begins with loading a metal coil onto an uncoiler. The uncoiler feeds the strip into the production line at a controlled rate.
Coil weight and strip length influence how frequently production must stop for replacement. Larger coils can reduce change frequency, but they require suitable material-handling equipment and sufficient uncoiler capacity.
Accumulation de bandes
An accumulator stores strip between the entry section and the forming mill. It allows the main production line to continue operating while the entry section completes a coil change or joins the next strip.
The type and capacity of the accumulator can strongly influence continuous production efficiency.
Profilage à rouleaux
The flat strip passes through a sequence of forming stands. Each stand gradually bends the material until the edges are correctly positioned for welding.
Roll design, stand alignment, shaft rigidity, and bearing condition affect forming stability. Poor control at this stage can create edge waves, twisting, dimensional errors, and unstable weld seams.
Soudage Haute Fréquence
The strip edges are heated and pressed together to create a continuous longitudinal weld. Welding speed must be coordinated with material grade, wall thickness, edge preparation, and forming conditions.
A machine may be mechanically capable of running faster than the welding process can consistently support. For buyers, stable weld quality is more important than the highest displayed speed.
Dimensionnement et Redressage
After welding, the tube passes through sizing stands to achieve the required outside dimensions and profile shape. Straightening helps control bow, twist, and final appearance.
For square and rectangular tubes, the sizing section must also maintain corner geometry and dimensional accuracy.
Découpe Volante
A flying saw or other cutting system divides the continuous tube into specified lengths without stopping the mill. Cutting acceleration, synchronization, blade condition, and return speed can influence maximum production speed.
Décharge et Emballage
Finished tubes are discharged, collected, inspected, and transferred for bundling or packaging. If the discharge table cannot remove products quickly enough, it can become a production bottleneck.
Quels facteurs déterminent la sortie de la machine du broyeur à tubes ?
Actual output is controlled by the slowest stage in the production process. Increasing forming speed will not improve final capacity if welding, cutting, inspection, or material handling cannot keep up.
Diamètre du tube et taille du profil
Small tubes may run at relatively high speeds because they require less forming work and are easier to cut and handle. Larger tubes normally need stronger stands, greater forming force, and more stable control.
Round, square, and rectangular tubes may also require different roll arrangements and sizing strategies.
Épaisseur de paroi
Thicker material increases the load on the forming stands, shafts, transmission system, welder, and cutting unit. It may require a lower line speed to maintain accurate forming and a reliable weld.
La plage d'épaisseur doit être vérifiée
A quotation should state the permitted wall-thickness range for specific tube sizes. A broad general thickness range may not apply to every profile included in the machine’s catalog.
Qualité matérielle
Yield strength, tensile strength, elongation, surface coating, and chemical composition influence forming behavior and welding response. High-strength steel may require stronger tooling and different operating parameters than common low-carbon steel.
Buyers should provide representative coil specifications instead of asking for a machine based only on finished tube dimensions.
Longueur du tube
Short finished lengths create more cutting cycles per hour. The flying cutting system must accelerate, synchronize, cut, and return before the next cutting cycle begins.
A production line that performs well with six-meter tubes may not achieve the same line speed when producing many short pieces.
Tolérance dimensionnelle
Tighter dimensional requirements can reduce practical speed because the process requires more stable forming, closer monitoring, and more frequent measurement. Buyers should define acceptable outside dimensions, corner geometry, straightness, length tolerance, and weld condition.
Comparaison de la capacité des machines du broyeur
The following table shows how different production factors affect practical output. The values are not fixed specifications; final capability must be confirmed for the selected equipment and product range.
| Production factor | Lower-demand condition | Higher-demand condition | Likely effect on output | What buyers should verify |
|---|---|---|---|---|
| Tube size | Small round tube | Large square or rectangular tube | Larger profiles may reduce speed | Size-specific production speed |
| Épaisseur de paroi | Thin wall | Thick wall | Thicker material increases forming and welding load | Motor, shaft, gearbox, and welder capacity |
| Matériel | Standard mild steel | High-strength or coated steel | Material behavior may limit stable speed | Approved material grades |
| Longueur coupée | Long standard lengths | Frequent short lengths | More cutting cycles can limit line speed | Flying saw cycle capacity |
| Size changes | Long production runs | Changements fréquents de produits | Changeovers reduce operating time | Tooling and adjustment method |
| Manipulation de bobines | Continuous coil supply | Frequent manual changes | Entry downtime reduces utilization | Uncoiler and accumulator configuration |
| Inspection level | Basic dimensional checks | Extensive inline testing | Additional checks may slow release | Quality-control workflow |
| Automation | Manual adjustments | Coordinated automatic control | Automation may improve repeatability | Control functions and data records |
This comparison helps buyers understand why two factories using similar machines may report different monthly outputs.
Comment calculer la capacité de production pratique
A basic capacity calculation begins with operating speed and available production time. The result must then be adjusted for utilization and yield.
Étape 1 : Calculez la longueur théorique
A simplified formula is:
Theoretical output length = Line speed × Available operating minutes
If a tube mill machine runs at 60 meters per minute for an eight-hour shift, its theoretical length would be:
60 × 480 = 28,800 meters per shift
This figure assumes that the machine operates continuously without stopping. It should not be treated as the expected saleable output.
Étape 2 : Appliquer le taux d'utilisation
Utilization represents the percentage of available time during which the line is actually producing. Coil changes, tool adjustments, maintenance, inspections, and production interruptions reduce this rate.
If the line achieves 75% utilization:
28,800 × 75% = 21,600 meters
Étape 3 : Appliquer le taux de rendement
Yield represents the percentage of produced material that meets quality requirements. Startup scrap, weld defects, dimensional errors, cut failures, and damaged tubes reduce the final quantity.
If acceptable yield is 96%:
21,600 × 96% = 20,736 meters of acceptable tube per shift
Utilisez des hypothèses conservatrices
New factories should avoid using aggressive utilization and yield assumptions. Operator experience, material consistency, maintenance practices, and production scheduling usually improve after the line has been commissioned.
Comment convertir la longueur du tube en tonnes
Many buyers evaluate output in tons per month rather than meters. To make this conversion, the approximate weight per meter of the finished tube must be known.
Weight depends on outside dimensions, wall thickness, profile shape, and material density.
Poids du tube rond
For a round tube, weight per meter can be estimated from its outside diameter, wall thickness, and steel density. Buyers should use the relevant engineering formula or verified product table for their market standard.
Poids du tube carré et rectangulaire
Square and rectangular tube calculations must account for external dimensions, thickness, and corner geometry. Theoretical formulas provide estimates, while actual weight may vary because of manufacturing tolerances.
Tonnage Mensuel
Once weight per meter has been established:
Monthly tonnage = Acceptable meters per shift × Weight per meter × Number of shifts × Working days
This method is more realistic than accepting a supplier’s general monthly tonnage claim without knowing the assumed product.
Pourquoi la vitesse maximale de la ligne peut être trompeuse
Maximum line speed is often achieved with a favorable tube size, material, thickness, and cut length. It may not apply to the buyer’s most common product.
A useful quotation should therefore include a speed range for several representative products.
Vitesse sans charge
No-load speed shows how fast the mechanical system can move without forming and welding material. It is useful during commissioning but does not represent production output.
Vitesse de production stable
Stable production speed is the rate at which the tube mill machine can continuously produce material within the agreed dimensional and weld-quality limits.
This figure should be evaluated during a loaded test using specified coil material.
Vitesse de changement moyenne
Average shift speed includes routine slowdowns and normal operating interruptions. It is the most useful number for production planning, labor calculations, and return-on-investment analysis.
Comment les changements de produits réduisent la capacité de production
A factory producing one standard tube for long periods can achieve higher utilization than a factory processing many short orders. Every size or profile change requires time for tooling, adjustment, trial production, and quality confirmation.
Changements de rouleau
Traditional roll changes may require removing and reinstalling several tooling sets. The time required depends on machine design, tooling weight, operator experience, and lifting equipment.
Ajustements de diamètre
Some lines allow selected adjustments without completely replacing all tooling. However, the actual adjustment range and resulting tube accuracy must be confirmed.
Changements d'un tour à l'autre
Producing square or rectangular tube may require additional sizing stands and different tooling. Buyers should ask whether the proposed line forms round tube first and then reshapes it, or uses another process arrangement.
Les petites commandes nécessitent une stratégie différente
When order volumes are low and product variety is high, changeover efficiency may be more valuable than maximum line speed. Tooling organization, digital recipes, quick-adjust systems, and clear setup procedures can improve overall factory output.
Équipement qui doit correspondre à la machine de broyage de tubes
The main forming mill cannot achieve its expected capacity unless the upstream and downstream equipment has compatible performance.
Décolleur
The uncoiler must support the required coil width, outside diameter, inside diameter, and maximum weight. Insufficient load capacity can restrict the raw material that the factory is able to purchase.
Unité de jonction du cisaillement et des bandes
A shear prepares the strip ends, while a joining system connects the next coil. Efficient strip preparation helps reduce interruption time.
Accumulateur
The accumulator provides temporary strip storage. Its capacity should give the entry section enough time to complete a normal coil change while the main line continues running.
Soudeur haute fréquence
The welder must provide stable energy at the required production speed. Its capacity should be matched to tube dimensions, wall thickness, material, and intended line speed.
Scie volante
The cutting system must handle the complete size and thickness range. It should also support the required cut lengths and tolerances without creating a bottleneck.
Tableau de sortie
The run-out and collection system must safely receive tubes at the expected production rate. Automatic counting, stacking, or bundling may be necessary for high-output lines.
Lignes de production de tubes manuels ou automatisés
Automation level affects labor requirements, setup repeatability, production visibility, and quality control. It also influences purchase price and maintenance complexity.
Ligne de production semi-automatique
A semi-automatic line uses powered equipment but relies on operators for many adjustments, inspections, and handling tasks. It may suit factories with stable products, moderate output, and experienced operators.
The initial investment can be lower, but performance may depend more heavily on individual skills.
Ligne de production entièrement automatique
A fully automatic tube mill machine can coordinate speed, cutting length, equipment status, and selected adjustments through a centralized control system.
Automation can reduce repetitive manual work and improve consistency. However, buyers must confirm what “fully automatic” includes because the term may be defined differently by each supplier.
Ligne de production intelligente
A smart line may add real-time monitoring, production records, fault alerts, energy data, maintenance reminders, and factory-system integration.
Concentrez-vous sur les données utiles
More data does not automatically create more value. Buyers should identify which information production managers, maintenance teams, and quality departments will actually use.
Comment la qualité du soudage affecte la vitesse de production
The weld is one of the most critical quality points in welded-tube production. Excessive speed can cause unstable heating, poor edge convergence, incomplete bonding, or inconsistent bead formation.
Présentation Edge
The forming stands must guide both strip edges into the correct position. Poor edge alignment increases weld instability even when the welding equipment has sufficient power.
Entrée de chaleur
Heat input must match the material, wall thickness, and line speed. Too little heat may create incomplete fusion, while excessive heat can damage the weld area or increase bead size.
Pression de compression
Squeeze rolls apply pressure to the heated edges. Their alignment and force influence the final weld structure and appearance.
Inspection des soudures
Depending on the tube application, inspection may include visual checks, dimensional measurement, flattening tests, eddy-current testing, ultrasonic testing, or hydrostatic testing.
The required testing method should be considered when designing the complete production workflow.
Comment comparer les devis des machines de broyeur de tubes
Two quotations with similar product ranges may describe very different equipment. Buyers should compare the proposed configuration line by line.
Confirmez la matrice du produit
Prepare a table listing:
- Tube shape
- Outside diameter or section dimensions
- Épaisseur de paroi
- Qualité matérielle
- Largeur de bobine
- Longueur finie
- Tolérance dimensionnelle
- Expected monthly volume
Ask every supplier to confirm which products can be manufactured and at what expected stable speed.
Réviser la construction mécanique
Important points include:
- Forming stand quantity
- Shaft diameter and material
- Bearing brand and arrangement
- Gearbox and transmission design
- Machine base construction
- Roll material and heat treatment
- Adjustment mechanism
- Système de lubrification
Révisez le système électrique
The quotation should identify motors, drives, PLC, operator interface, sensors, safety devices, and electrical components. Confirm voltage, frequency, phase, and local service availability.
Comparez la portée incluse
One price may include only the forming mill, while another covers the uncoiler, accumulator, welder, flying saw, run-out table, tooling, installation, and training.
A low initial price may become expensive after the missing components are added.
Test d'acceptation d'usine de machine de broyeur à tubes
A factory acceptance test helps the buyer verify performance before shipment. The test should be based on agreed products and acceptance criteria.
Matériel pour les essais
Whenever practical, use material that represents the buyer’s real coil grade, thickness, and width. A test with easier material may not demonstrate performance under actual production conditions.
Éléments de performance
The test can review:
- Stable production speed
- Tube outside dimensions
- Wall-thickness compatibility
- Weld appearance
- Tube straightness
- Cut-length accuracy
- État de surface
- Control-system operation
- Fonctions de sécurité
- Procédure de basculement
Documentation
Record material specifications, tooling setup, operating parameters, produced quantity, inspection results, and any corrections made during the test.
Ne testez pas la vitesse seul
A short high-speed demonstration does not prove continuous production capability. The line should run long enough to evaluate temperature stability, welding consistency, cutting synchronization, and finished-product quality.
Erreurs courantes d’achat de machines dans les usines de tubes
Choisir uniquement au prix le plus bas
A lower price may reflect a smaller scope, lighter mechanical structure, limited tooling, or fewer supporting systems. Compare total project cost rather than the main machine price alone.
Croire à la vitesse maximale
Ask what tube size, thickness, material, and length were used to establish the stated speed. Request both maximum and recommended continuous speeds.
Ignorer le mix de produits
A line designed for one long production run may not be efficient for frequent small orders. Product variety must be included in the capacity calculation.
Temps de passage sous-estimé
Tooling changes and adjustments can consume a large part of a shift. Ask the supplier to demonstrate the actual changeover process.
Oublier la manutention en aval
Cutting, collection, inspection, and packaging must support the planned production rate. Otherwise, downstream delays will force the main mill to slow down.
Échec de la formation des opérateurs de plan
A well-designed tube mill machine still requires trained operators, maintenance technicians, electricians, and quality inspectors. Training should cover both normal operation and troubleshooting.
FAQ À propos de la capacité des machines de broyeur
Combien de tonnes une machine de broyeur à tubes peut-elle produire par mois ?
Monthly tonnage depends on tube dimensions, wall thickness, weight per meter, operating speed, shifts, working days, utilization, and yield. A supplier should calculate output using your actual product mix rather than provide one general figure.
Quelle est une bonne vitesse de production de moulin à tubes ?
There is no universal best speed. The correct speed is one that consistently produces acceptable dimensions and weld quality for the required material and tube specification.
Un broyeur à tubes peut-il produire des tubes ronds, carrés et rectangulaires
Many lines can manufacture several profiles when equipped with suitable forming and sizing sections. Confirm the exact size matrix, tooling requirements, and changeover method.
L'acier plus épais réduit-il la vitesse du laminoir à
It often does. Thicker material increases forming force, welding demand, cutting load, and equipment stress, which may require a lower stable operating speed.
Combien de temps prend un changement de taille de tube ?
Changeover time varies according to machine design, tooling arrangement, product difference, lifting equipment, and operator experience. Ask for a live demonstration or documented changeover procedure.
Une soudeuse haute fréquence est-elle incluse dans le broyeur à tubes ?
It depends on the quotation. Some suppliers quote the forming mill separately, while others provide a complete line. Confirm every included component before comparing prices.
Qu'est-ce qui cause une faible efficacité de production
Common causes include frequent coil changes, long tooling adjustments, unstable welding, poor material consistency, equipment failures, cutting delays, insufficient inspection capacity, and unplanned maintenance.
Dois-je choisir la machine disponible la plus rapide
Not necessarily. A faster line may require more expensive welding, cutting, handling, and automation systems. Choose a
这篇建议围绕 tube mill machine 展开,与网站的高频焊管生产线、方管成型设备等产品方向更加匹配,也能覆盖产能、设备配置和采购成本等高购买意图问题。
H1 Title: Tube Mill Machine Capacity: A Practical Buyer’s Guide
Purchasing a tube mill machine requires more than comparing maximum production speed. Buyers must determine whether the complete line can consistently produce the required tube sizes, wall thicknesses, materials, and monthly output.
A line advertised at a high forming speed may deliver much lower real production capacity after changeovers, coil loading, welding adjustments, cutting, maintenance, and quality inspections are considered. Understanding these factors helps manufacturers select a production line that supports both current orders and future growth.
Principaux points à retenir :
- Calculate capacity from saleable tubes rather than maximum line speed.
- Match the machine to tube diameter, wall thickness, material grade, and profile shape.
- Evaluate every process from uncoiling to finished-product collection.
- Include coil changes, roll changes, maintenance, and quality checks in production estimates.
- Confirm whether the line can produce round, square, and rectangular tubes.
- Compare high-frequency welding systems according to real material requirements.
- Check the relationship between automation, labor, changeover time, and output.
- Request a production test using material close to your actual specification.
Quelle est la capacité de la machine du broyeur à tubes
Tube mill machine capacity describes how much qualified tubing a production line can manufacture within a specified period. It may be expressed in meters per minute, tons per shift, tubes per hour, or tons per month.
However, these figures do not describe exactly the same thing. Line speed measures how quickly the strip moves, while production capacity measures how many acceptable finished tubes are produced after downtime and losses are considered.
Vitesse de ligne nominale
Rated speed is usually the maximum mechanical speed stated by the equipment supplier. It may be achievable when the machine is producing a suitable tube size under stable operating conditions.
Rated speed is useful for comparing basic equipment potential, but it should not be treated as guaranteed output for every product specification.
Vitesse de production réelle
Actual speed is the stable operating speed achieved with a specific material, tube diameter, wall thickness, weld type, and quality requirement.
Thick material, difficult steel grades, frequent specification changes, and strict surface requirements may reduce practical operating speed.
Sortie vendable
Saleable output includes only tubes that satisfy dimensional, welding, surface, and length requirements. Scrap, trial pieces, setup material, and defective tubes should not be counted as finished production.
For purchasing decisions, saleable output is more meaningful than the highest displayed speed of the tube mill machine.
Comment fonctionne une machine de broyeur de tubes ?
A tube mill production line converts a metal coil into continuously formed and welded tubing. Depending on the configuration, the line may include uncoiling, strip joining, accumulation, forming, welding, sizing, straightening, cutting, and collection.
The performance of every section affects final production capacity. One slow or unstable process can restrict the output of the entire line.
Débobinage et alimentation en bandes
The uncoiler supports and releases the steel coil into the production line. Stable strip feeding helps prevent sudden tension changes that may affect forming accuracy.
For continuous or high-volume production, the uncoiler must match the coil weight, strip width, and line speed required by the project.
Accumulation de bandes
An accumulator stores strip so the forming and welding sections can continue running while a new coil is prepared. Without enough accumulation capacity, the entire line may need to stop during every coil change.
Pourquoi la capacité de l'accumulateur est importante
An accumulator does not directly increase the maximum forming speed. Instead, it reduces avoidable downtime and helps the line remain in continuous production for a greater percentage of each shift.
Profilage à rouleaux
The forming section gradually shapes flat strip into an open circular profile. Correct roll design, stand alignment, and forming sequence are important for stable edges and consistent welding.
Improper forming may cause edge waves, twist, unstable weld seams, or excessive roll wear.
Soudage Haute Fréquence
The welding section heats and joins the strip edges to create a continuous tube. Welding stability depends on material properties, strip preparation, line speed, power settings, edge presentation, and cooling control.
Dimensionnement et Redressage
After welding, sizing stands bring the tube to its required dimensions. If square or rectangular tubing is being produced, additional shaping stages may convert a round tube into the final profile.
Découpe Volante
A flying saw or flying cold-cutting system cuts the moving tube to length without stopping the main production line. Cutting speed, tracking accuracy, and blade life directly affect productivity and finished length tolerance.
Principaux facteurs qui déterminent la sortie de la machine du broyeur à tubes
The theoretical output of a tube mill machine can be estimated from line speed, tube dimensions, material density, and operating time. Real capacity also depends on production efficiency and the percentage of acceptable products.
Before comparing quotations, buyers should define a representative product mix rather than asking for one general capacity figure.
Diamètre du tube et taille du profil
Smaller tube sizes may run faster because they require less forming force and create less load on the production line. Larger tubes generally require stronger stands, shafts, bearings, gearboxes, and drive systems.
Square and rectangular profiles may also require additional sizing control. Sharp corner requirements can increase the forming difficulty.
Épaisseur de paroi
Thicker strip increases the load placed on forming stands, welding equipment, motors, and cutting systems. It may also require a lower production speed to maintain consistent forming and welding quality.
The supplier should confirm output for both the thinnest and thickest walls in the required product range.
Qualité matérielle
Carbon steel, galvanized steel, stainless steel, and high-strength steel do not behave identically during forming. Yield strength, coating condition, surface finish, and dimensional tolerance may influence machine settings and stable speed.
Ne spécifiez pas le matériel uniquement en tant que“Steel”
A useful inquiry should include the material standard, grade, yield strength, tensile strength, strip thickness, coating condition, and expected surface quality. This allows the supplier to evaluate the tooling and power requirements more accurately.
Longueur du tube fini
Short finished lengths create more frequent cutting cycles. The flying cutting unit must accelerate, synchronize with the moving tube, complete the cut, and return for the next cycle.
If the cutting system cannot complete this sequence quickly enough, it may become the line’s production bottleneck.
Exigences de qualité du produit
Tight dimensional tolerances, smooth weld seams, controlled corner radii, and high surface-finish requirements may limit practical line speed. Production capacity should therefore be considered together with the acceptable quality standard.
A faster line does not create more value if a higher percentage of tubes must be reworked or rejected.
Comparaison de la capacité des broyeurs à tubes par scénario de production
The following table shows how different production conditions influence the type of tube mill machine configuration a buyer may require. These are selection principles rather than fixed technical specifications.
| Production scenario | Main capacity priority | Important equipment configuration | Common capacity risk |
|---|---|---|---|
| Small-batch custom tubes | Fast specification changes | Quick-change tooling and flexible controls | Too much time lost during roll changes |
| High-volume standard tubes | Durée continue | Accumulator and automated cutting | Selecting equipment only by maximum speed |
| Thick-wall structural tubes | Forming force and weld stability | Heavy-duty stands and sufficient welding power | Drives or shafts undersized for thick strip |
| Furniture and decorative tubes | Qualité de surface | Controlled strip handling and non-marking systems | Scratches reducing saleable output |
| Square and rectangular tubes | Dimensional consistency | Accurate sizing and straightening sections | Poor corners or excessive tube twist |
| Multiple tube profiles | Tooling flexibility | Organized roll sets and adjustment systems | Long changeovers reducing monthly output |
| Export-oriented production | Repeatability and documentation | Quality monitoring and traceable controls | Output achieved at the expense of consistency |
A supplier should calculate the recommended configuration using actual product specifications. General category names such as “small tube mill” or “high-speed tube mill” are not detailed enough for final selection.
Comment calculer la capacité de production réelle
Production planning should begin with theoretical output and then account for operational efficiency. The calculation does not need to be complicated, but it must use realistic input values.
Étape 1 : Déterminez la vitesse de ligne stable
Use the expected production speed for a representative tube specification. Do not automatically use the maximum mechanical speed shown in the product brochure.
Ask the supplier to provide estimated stable speeds for several important sizes and thicknesses.
Étape 2 : Calculez le temps de production programmé
Determine the number of working hours per shift, shifts per day, and working days per month.
Then subtract planned breaks, preventive maintenance, roll changes, coil loading, and quality inspections.
Étape 3 : Appliquer un facteur d’efficacité
The efficiency factor accounts for unplanned stops, welding adjustments, material variation, minor faults, and operator delays.
New factories should use conservative assumptions because operators may require time to become familiar with the tube mill machine.
Étape 4 : Appliquer le taux de rendement
Not every meter of input strip becomes a saleable finished product. Edge trimming, coil ends, trial sections, weld adjustments, cutting losses, and rejected tubes reduce actual yield.
Formule de capacité de base
A simplified monthly calculation can be expressed as:
Monthly saleable output = Stable production rate × Available production time × Operating efficiency × Product yield
When production is measured in tons, the tube weight per meter must also be included.
Exemple de la Logique de Calcul
If a line operates at a stable speed for only part of each shift, the unused time cannot be treated as production. Likewise, tubes rejected during quality inspection should not be included in final output.
The goal is not to create the highest theoretical result. The goal is to estimate the quantity that the factory can reliably deliver to customers.
Vitesse maximale par rapport à la sortie réelle
Maximum speed is one of the most visible figures in a quotation, but it can also be one of the most misleading. The maximum may apply only to a specific small, thin-wall tube under ideal conditions.
A buyer should request a capacity matrix covering the main production sizes.
Questions à poser sur la vitesse
Demandez au fournisseur :
- Which tube size can run at the quoted maximum speed?
- What material grade was used to determine the speed?
- What speed is expected for the thickest wall?
- Does the figure include square and rectangular tube production?
- What finished length was used?
- Can the flying saw operate continuously at that speed?
- What quality tolerance can be maintained?
- Has this speed been verified on an existing line?
Matrice de Capacité
A useful capacity matrix lists tube size, wall thickness, material, expected stable speed, approximate weight per meter, and projected output.
This makes it easier to identify whether the tube mill machine is optimized for the products that generate most of the buyer’s revenue.
Comment les changements de produits affectent la capacité
A tube mill that runs quickly but requires long changeovers may produce less per month than a slightly slower line with efficient tooling changes.
This is particularly important for contract manufacturers producing many tube specifications in small batches.
Temps de changement de rouleau
Traditional roll changes may require the removal, handling, installation, and alignment of multiple roll stands. The time required depends on machine design, tooling weight, operator experience, and available lifting equipment.
A complete quotation should explain the roll-changing method and any optional quick-change system.
Ajustement de la taille
Some changes may be completed through stand adjustment, while others require a complete tooling replacement. Buyers should confirm which products can share roll sets and which require separate tooling.
Organisation d'outillage
Clearly marked roll sets, proper storage racks, lifting tools, setup records, and standardized procedures can reduce changeover errors. These operational details influence production capacity even though they are not part of the advertised line speed.
Inspection de première pièce
After a changeover, the first tubes must be checked for dimensions, straightness, weld quality, corner shape, and cut length. The production schedule should include time for adjustment and approval.
Production de tubes ronds, carrés et rectangulaires
Many buyers want one production line to manufacture several tube profiles. This can be possible, but the tooling, forming route, sizing range, and quality requirements must be evaluated carefully.
Le machine de formage de tubes carrés provides a useful reference for manufacturers considering square or rectangular tube production.
Formage rond à carré
In this method, the strip is first formed and welded as a round tube. Sizing stands then reshape it into a square or rectangular profile.
It is a common and flexible production method, but corner radius and wall-thickness distribution must be properly controlled.
Formage carré direct
Direct square forming shapes the strip toward the final profile before welding. Depending on the product range and line design, it may offer material or tooling advantages.
However, it requires a suitable forming system and careful technical evaluation. Buyers should not assume that every conventional tube mill supports direct square forming.
Profil Tolérances
Square and rectangular tubes must be evaluated for side dimensions, corner radius, twist, concavity, convexity, straightness, and weld position.
The expected production speed should be linked to these finished-product requirements.
Équipement qui peut devenir un goulot d'étranglement de production
A complete tube mill machine is a connected system. The overall line can only operate as efficiently as its slowest essential section.
Buyers should compare the capacity of every major component.
Décolleur
An undersized uncoiler may not support the required coil weight or strip width. Slow loading and manual expansion can also increase downtime between coils.
Équipement de jonction d'extrémité de bande
The ends of consecutive coils must be prepared and joined before entering the accumulator. A slow or difficult joining process can delay coil changes and reduce operating efficiency.
Accumulateur
The accumulator must hold enough strip to cover the expected coil-change time. If stored strip runs out before the new coil is ready, the forming section must stop.
Système de soudage
Welding capacity must match the material, thickness, and target speed. Insufficient power or unstable edge presentation can create weak or inconsistent seams.
Système de coupe
The cutting unit must support the shortest required product length at the intended line speed. Otherwise, the main line may need to slow down to complete each cutting cycle.
Emballage et Collection
Finished tubes must be removed, inspected, counted, bundled, and transported away from the line. Poor downstream handling can create congestion even when the forming and welding sections operate correctly.
Niveaux d'automatisation pour une machine de broyage de tubes
Automation can reduce manual intervention, improve repeatability, and provide more accurate production records. However, it should be selected according to factory requirements rather than added without a clear purpose.
Configuration semi-automatique
A semi-automatic line may require operators to adjust some stands, monitor welding, inspect finished tubes, and manage product collection.
This option may offer a lower initial cost, but output can depend more heavily on operator experience.
Configuration entièrement automatique
A highly automated tube mill machine may integrate coordinated drive control, automated length setting, production counting, fault alarms, parameter storage, and automated collection.
It can improve consistency and reduce repetitive tasks, especially in high-volume factories.
L'automatisation n'élimine pas la configuration
Operators still need to verify tooling, material, weld quality, cooling, lubrication, and finished dimensions. Automation supports a controlled process but cannot correct an unsuitable machine configuration.
Comment comparer les devis des machines de broyeur de tubes
Quotations should be compared line by line rather than by total price. A lower-priced proposal may exclude essential tooling, an accumulator, testing equipment, installation, or operator training.
Prepare one technical requirement sheet and send it to every potential supplier.
Gamme Produits
Préciser:
- Round tube diameter range
- Square and rectangular tube range
- Minimum and maximum wall thickness
- Material grades and coating conditions
- Strip width range
- Longueurs de tubes finis
- Dimensional and surface requirements
Cible de Production
Fournir:
- Required annual or monthly output
- Expected shifts per day
- Typical batch size
- Number of specification changes
- Main high-volume tube sizes
- Acceptable scrap rate
- Future expansion plans
Configuration de ligne requise
Ask whether the quotation includes:
- Coil loading equipment
- Décolleur
- Strip-end shear and joining equipment
- Accumulateur
- Forming and sizing stands
- High-frequency welding system
- Seam scarfing equipment
- Cooling section
- Flying cutting system
- Table d'épuisement
- Bundling or stacking system
- Outillage rouleau
- Electrical controls
- Installation and training
- Pièces détachées recommandées
You can review Jinbolida’s broader tube mill production line solutions when comparing possible production configurations.
Tests d'acceptation en usine avant expédition
Factory acceptance testing helps verify whether the machine can produce the agreed tube specification before it is shipped.
The test should be based on representative materials and documented acceptance criteria.
Utiliser un Produit Représentant
Whenever practical, test one of the buyer’s important tube specifications. A demonstration using only the easiest small-diameter product may not prove performance across the full range.
Enregistrer les conditions de fonctionnement
The test record should identify:
- Material grade and strip thickness
- Coil or sample-strip dimensions
- Tube size and finished length
- Stable production speed
- Welding settings
- Dimensional measurements
- Surface and weld observations
- Précision de coupe
- Quantity of qualified tubes produced
Inspectez les tubes finis
Inspection may include dimensions, wall thickness, straightness, twist, cut quality, weld appearance, and other tests required by the agreed product standard.
Confirmez la norme d’acceptation tôt
The buyer and supplier should agree on test methods and acceptance criteria before manufacturing begins. This prevents different interpretations during final inspection.
Erreurs courantes d’achat de machines dans les usines de tubes
Recognizing common mistakes can help buyers avoid low productivity, unexpected upgrades, and product-quality problems.
Sélection par Maximum Speed Alone
High maximum speed has little value if the line cannot maintain weld quality or cutting accuracy for the required product.
Providing an Incomplete Tube Range
If the supplier receives only maximum diameter and thickness, the tooling and drive system may not be optimized for the buyer’s real product mix.
Ignorer le temps de changement
Factories producing small orders can lose a significant portion of each shift during tooling changes and adjustment.
Underestimating Downstream Handling
Inspection, collection, bundling, and transport must keep pace with the production line.
Excluding Tooling from the Comparison
The main machine and roll tooling form one production system. Tooling material, design, number of sets, and expected service life should be included in the technical comparison.
Failing to Plan Installation
Foundation conditions, factory height, crane capacity, electrical supply, cooling water, compressed air, and available floor space should be checked before the equipment arrives.
FAQ À propos de la capacité des machines de broyeur
How many tons can a tube mill machine produce per day?
Daily output depends on tube size, wall thickness, material, stable line speed, operating hours, efficiency, and product yield. Ask the supplier to calculate output using your actual tube schedule instead of relying on a general tonnage figure.
What controls the speed of a tube mill?
Forming stability, welding capacity, material properties, finished tube length, cutting speed, cooling, and quality requirements can all limit production speed.
Can one tube mill produce round and square tubes?
Many lines can produce round tubes and then size them into square or rectangular profiles. The available range depends on the machine design and installed tooling.
Does thicker tube require a more powerful machine?
Usually, yes. Thicker material increases forming loads and may require stronger stands, shafts, drives, welding equipment, and cutting systems.
How much production time is lost during a roll change?
Changeover time varies widely according to machine design, tooling weight, lifting equipment, operator skill, and adjustment requirements. Request an estimated changeover procedure and time from the supplier.
Is the fastest tube mill always the most productive?
No. A slower but more stable line may produce more qualified tubes if it has fewer stops, faster changes, lower scrap, and better cutting reliability.
What is the purpose of an accumulator?
An accumulator stores strip and allows the forming section to continue operating while a new coil is being prepared and joined. This reduces stoppage during coil changes.
How can I estimate monthly tube production?
Multiply the realistic production rate by scheduled operating time, then apply reasonable efficiency and yield factors. Use separate calculations for major product sizes if their production speeds differ significantly.
What information does a tube mill supplier need?
The supplier needs tube shapes, dimensions, wall thicknesses, material grades, finished lengths, target capacity, electrical conditions, quality requirements, and available factory space.
Should I request a production test?
Yes. A documented factory acceptance test using a representative tube specification helps verify forming, welding, sizing, cutting, and overall line stability before shipment.
Conclusion
Choosing a tube mill machine should begin with the factory’s actual product mix and saleable production target. Maximum line speed is only one part of the calculation.
A reliable capacity assessment must include tube dimensions, wall thickness, material grade, welding requirements, finished length, tooling changes, coil handling, cutting cycles, maintenance, labor, scrap, and quality inspection.
Before placing an order, ask the supplier to provide a capacity matrix for the most important products. Review the complete line configuration, identify possible bottlenecks, and agree on a representative factory acceptance test.
Manufacturers planning a new tube production facility or upgrading an existing line can explore Jinbolida’s industrial machinery and production-line solutions. For a configuration based on your tube sizes, materials, output target, and factory layout, submit the project details through the page contact.
Si vous avez apprécié cet article sur l'expertise de Jinbolida en matière de fabrication intelligente et d'usine numérique, suivez-nous pour plus d'informations et de mises à jour :
- 📘 Facebook : Restez à l'écoute de nos derniers projets de lignes de production intelligentes → Facebook
- 📱 WhatsApp : Contactez-nous à tout moment pour des solutions de production personnalisées → Chattez maintenant
- ▶️ YouTube : Regardez nos démonstrations de lignes automatisées et nos applications concrètes → YouTube
Continuons d'innover et de façonner ensemble l'avenir de l'industrie intelligente !
 French
 English
 Arabic
 Russian
 Spanish