
Крен Формируя Springback: причины и как контролировать его
Оглавление
Введение
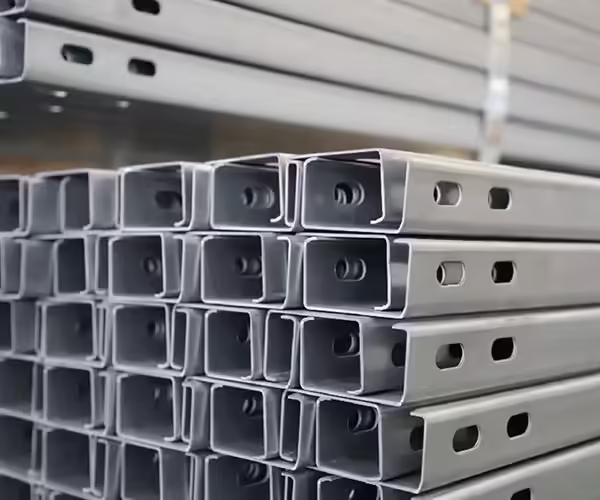
A roll formed profile does not always remain exactly in the shape imposed by the rollers. After metal leaves a forming pass and the external forming force is reduced, part of the deformation can recover elastically. This phenomenon is known as roll forming springback.
Springback can change bend angles, corner radii, flange positions, overall width, profile height, and the relationship between different features in the finished section. The effect may be small on a simple low-strength steel profile but become much more noticeable when forming high-strength steel, stainless steel, aluminum, thin material, or profiles with relatively large bend radii.
For manufacturers, the main challenge is not eliminating every form of elastic recovery. Springback is a normal result of metal deformation. The objective is to understand how much recovery is likely to occur and then design the tooling and forming process so the material reaches the required geometry after it leaves the rollers.
Stable springback control therefore depends on material properties, bend geometry, flower-pattern design, over-forming, roll gaps, final calibration, machine alignment, and consistent raw material.
Что такое ролл, образующий спрингбек?
Roll forming springback is the partial elastic recovery that occurs after a metal strip is bent and the forming load is removed.
During bending, the material contains both elastic and plastic deformation.
Plastic deformation creates the permanent shape.
Elastic deformation remains recoverable.
When the strip leaves the forming roll, the elastic portion attempts to return toward its original condition. As a result, the final bend often opens slightly compared with the shape imposed while the material was under load.
A simplified example is a flange that needs to finish at 90 degrees.
If the tooling forms the material to exactly 90 degrees while it is under pressure, the flange may leave the roll and recover to 92 or 93 degrees depending on the material and forming conditions.
The tooling may therefore need to intentionally form beyond the required angle so that after springback occurs, the finished profile approaches the target dimension.
This intentional compensation is commonly called over-forming or overbending.
Почему металлическая пружина возвращается после формирования рулона?
To understand springback, it helps to consider what happens across the material thickness during bending.
The outside surface of a bend is stretched.
The inside surface is compressed.
Between them is a region where longitudinal strain is lower, commonly associated with the neutral axis.
When forming force is applied strongly enough, some regions pass beyond the elastic range and experience permanent plastic deformation. Other portions of the stress distribution still contain recoverable elastic strain.
Once the material leaves the tooling, that elastic strain is released.
The cross-section therefore changes slightly.
MIT’s manufacturing coursework on sheet metal springback illustrates this principle: after unloading, the final bend radius can increase and the bend angle can decrease because the elastic portion of the deformation attempts to recover.
Roll forming applies this same material behavior progressively across several forming stands instead of in one press-brake operation.
Почему пружинение имеет значение при формировании рулонов
Roll forming produces long sections where small angular differences can affect several finished dimensions simultaneously.
Suppose a channel contains two side flanges.
If each flange springs outward slightly, the finished profile may show changes in:
- габаритная ширина,
- угол фланца,
- ширина проема,
- hole relationship,
- assembly fit,
- and straightness.
A profile can therefore appear only slightly different at one bend while the accumulated dimensional change becomes significant across the complete section.
Springback is especially important for products such as:
- солнечные монтажные каналы,
- construction profiles,
- C and U sections,
- Z-профили,
- структурные каналы,
- brackets,
- steel formwork components,
- and customized industrial profiles.
The tighter the required assembly relationship, the more important controlled springback becomes.
Прочность материала оказывает большое влияние
Yield strength is one of the most important material properties affecting springback.
Higher-strength material generally requires greater stress to create permanent deformation.
As a result, the proportion of recoverable elastic deformation can become more significant.
This means a roll set developed around relatively mild steel may behave differently when high-strength steel is introduced.
The profile may leave the final forming stand with:
- more open bend angles,
- larger effective bend radii,
- different flange positions,
- or increased dimensional variation.
Operators sometimes respond by tightening the rollers.
That may change the profile temporarily, but excessive roll pressure is not the same as correctly compensating for material behavior.
If the new steel grade produces more springback, the forming strategy should be reviewed systematically.
Упругий модуль также влияет на пружинение
Springback is related not only to yield strength but also to the material’s elastic stiffness.
The relationship between yield strength and elastic modulus helps explain why different materials can show substantially different recovery after bending.
Materials with a relatively high ratio of yield strength to elastic modulus can exhibit more noticeable springback.
This is one reason aluminum and certain high-strength steels can behave very differently from conventional low-carbon steel.
Two coils with the same thickness and profile geometry therefore should not automatically be expected to use identical forming settings if the material properties are substantially different.
Толщина материала влияет на пружинение
Material thickness changes the relationship between elastic and plastic deformation during bending.
In general, thinner material can show greater springback sensitivity when other conditions remain comparable.
A thin strip also has less section stiffness, making it more sensitive to:
- зазоры валков,
- положение инструмента,
- side pressure,
- вариация материала,
- and downstream handling.
Thickness variation within the allowable coil specification can therefore contribute to angular and dimensional variation.
For tight-tolerance profiles, incoming thickness should be checked during commissioning and after material changes.
If a profile begins opening more after a new coil is introduced, material thickness should be examined before large machine adjustments are made.
Радиус изгиба меняет поведение спрингбека
The relationship between bend radius and material thickness has a strong effect on springback.
A relatively large bend radius compared with sheet thickness usually produces a larger elastic contribution to the total deformation.
This can increase springback.
A tighter radius forces more material into plastic deformation, although excessively tight bending can introduce other concerns such as high strain, surface damage, or cracking depending on the material.
The tooling designer therefore should not simply make the bend radius smaller to reduce springback.
The correct radius should satisfy:
- product design,
- material formability,
- structural requirements,
- состояние поверхности,
- tooling capability,
- and applicable product specifications.
Springback compensation should then be designed around that required geometry.
Факторы пружинения, образующие крен
| Фактор | Typical Effect on Springback | What to Review |
|---|---|---|
| Предел текучести | Higher strength can increase recovery | Материальный сорт |
| Elastic modulus | Influences elastic recovery | Тип материала |
| Толщина | Thin material can be more springback-sensitive | Диапазон толщины |
| Радиус изгиба | Larger radius/thickness ratio can increase recovery | Рисунок профиля |
| Угол изгиба | Greater deformation changes stress distribution | Цветочный узор |
| Tooling progression | Controls how strain develops | Number and sequence of passes |
| Зазор валка | Influences actual bending condition | Настройка |
| Вариация материала | Changes recovery between coils | Incoming inspection |
| Over-forming | Compensates for expected recovery | Final passes |
| Calibration | Refines final profile geometry | Finishing stands |
| Износ инструмента | Changes effective forming geometry | Обслуживание |
| Выравнивание машины | Changes material loading | Stand and shaft condition |
Почему одно значение Springback не может быть использовано для каждого профиля
Springback is often discussed as though every bend can be corrected using one fixed angular allowance.
Real roll forming is more complicated.
Профиль может содержать
- different bend radii,
- different flange lengths,
- asymmetric features,
- возвратные губы,
- several closely spaced bends,
- пробитые отверстия,
- and locally reinforced areas.
Each feature interacts with the rest of the cross-section.
A 2-degree overbend that works on one flange does not necessarily work on another section of the same profile.
The complete forming progression must therefore be evaluated rather than assigning one universal springback correction to every roller.
Спрингбек начинается во время всей формирующейся последовательности
The final profile is created through multiple passes.
Each pass changes the stress condition left by the previous one.
This means springback should not be considered only at the last forming station.
Early passes establish how material begins to move.
Intermediate stands continue bending and redistribute stress.
Later stands finish the geometry and may intentionally introduce compensation.
If the early forming progression is poorly designed, the final stands may need to correct excessive accumulated error.
This can increase residual stress and make the profile less stable after cutting.
A better approach is to manage deformation progressively so that the final correction remains controlled.
Дизайн цветочного узора помогает контролировать пружинение
The flower pattern shows the cross-section at each major forming stage.
It allows the tooling designer to decide:
- when each bend begins,
- how rapidly it develops,
- which features form first,
- how adjacent bends interact,
- and where final correction should occur.
For springback-sensitive materials, the progression can be adjusted so that bends are not created too aggressively in one station.
The designer may also reserve later passes for controlled over-forming and calibration.
A good flower pattern therefore does more than show the shortest path between flat strip and final profile.
It manages material strain throughout the machine.
JBLDIE's направляющая машины для формования рулонов explains how profile geometry develops progressively through multiple roller stations rather than being created in a single operation.
Чрезмерное формирование - распространенный метод компенсации
One of the most direct methods of controlling springback is intentional over-forming.
Suppose the required finished angle is 90 degrees.
If testing shows that the material consistently springs open by approximately 2 degrees under established production conditions, tooling may form the profile beyond 90 degrees before release.
After elastic recovery, the flange moves closer to the desired final angle.
The concept is straightforward, but implementation requires care.
Too little over-form produces an open angle.
Too much creates an excessively closed angle.
The correct compensation depends on:
- фактический материал,
- толщина,
- radius,
- формирование истории,
- tooling geometry,
- и настройка машины.
Over-forming should therefore be validated using representative production material.
Где должно произойти переформирование?
Over-forming does not always need to happen in only one stand.
Depending on the profile, compensation may be distributed across several later forming passes.
This can produce a smoother deformation path than forcing a large angular correction at the final station.
For example, a profile requiring a nominal 90-degree flange may progress conceptually through:
20° → 45° → 70° → 88° → controlled over-form → final calibration
The actual values depend entirely on the profile and tooling design.
The purpose is to reach the final geometry through controlled stages while accounting for material recovery.
Калибровочные стенды помогают стабилизировать конечную геометрию
Later roller stations can function partly as calibration passes.
Instead of introducing major new bends, these stands refine:
- angle,
- ширина,
- height,
- положение фланца,
- and cross-sectional stability.
Calibration is particularly useful when the material has already undergone most of its plastic deformation.
The tooling can then apply controlled correction to bring the profile closer to the final dimensional requirement.
However, calibration should not be expected to repair a fundamentally poor forming sequence.
If the profile arrives at the final stands with severe twist, wave, or incorrect bend locations, aggressive calibration may add residual stress rather than produce a stable solution.
Пробел влияет на компенсацию пружинного возврата
The actual contact relationship between the material and rollers influences the amount of deformation created at each pass.
If the roll gap changes, the effective forming condition can also change.
Excessive gap may reduce control.
An overly tight gap can create unnecessary compression, surface marking, or material distortion.
This means a tooling design with correct theoretical springback compensation can still produce inconsistent angles if roll gaps are not repeatable.
Successful settings should therefore be documented after commissioning.
During future production, operators can return the machine to a known baseline instead of adjusting every stand by visual judgment.
Не используйте чрезмерное давление крена в качестве универсального решения
A common troubleshooting response is to tighten the tooling when a flange springs open.
This can sometimes change the result, but it is not a reliable general method of controlling springback.
Excessive pressure can cause:
- поверхностные метки,
- increased tooling wear,
- краевая волна,
- additional longitudinal strain,
- unwanted profile distortion,
- or higher bearing and shaft loads.
The correct response is first to confirm whether the dimensional change is actually caused by springback.
The profile may instead be affected by:
- ширина материала,
- entry misalignment,
- worn tooling,
- incorrect roll position,
- bearing movement,
- or another mechanical issue.
Only after these possibilities are considered should springback compensation be adjusted.
Спрингбек против смещения инструментов
Springback and tooling misalignment can produce similar-looking symptoms.
Suppose a flange is more open than required.
Possible explanations include:
Спрингбек
The material bends correctly under load but opens after leaving the roll.
Incorrect Roll Position
The tooling never creates enough angle in the first place.
Shaft or Bearing Movement
The roll position changes under forming load.
Off-Center Feeding
One side of the profile forms differently from the other.
Инструмент Износ
The actual roller geometry is no longer the same as the original design.
The troubleshooting method should determine where the flange angle changes.
If the profile is correctly over-formed while inside the tooling and opens after release, springback is the likely mechanism.
If it never reaches the intended loaded geometry, machine setup should be investigated first.
Материальная согласованность имеет важное значение
Springback compensation works best when the incoming material remains reasonably consistent.
Imagine a tooling setup established with one steel grade and thickness.
If the next coil has a different yield behavior, the same over-forming condition may produce a different final angle.
The machine itself has not changed.
The material response has.
Incoming-material control should therefore include relevant checks such as:
- класс материала,
- толщина,
- ширина полосы,
- mechanical-property documentation where required,
- and coil identification.
Production records should associate coil information with dimensional inspection data when tight accuracy is important.
Изменение катушки на катушку может выявить материальные эффекты
One useful troubleshooting clue is whether the dimensional change begins exactly when a new coil enters production.
If the profile was stable throughout one coil and changes immediately after the next coil begins, material variation deserves attention.
Before changing several roll stands, compare:
- толщина,
- оценка,
- batch identification,
- ширина полосы,
- and known mechanical properties.
If the profile returns to its previous behavior when the original material specification is restored, the problem is unlikely to be random machine drift.
Recording these relationships gradually builds useful process knowledge for future material changes.
Высокопрочная сталь требует более тщательной компенсации
High-strength steel is increasingly used where thinner sections or greater structural capacity are required.
However, higher yield strength can make springback more noticeable.
Tooling originally developed around conventional mild steel may therefore need a different forming progression or over-forming strategy for high-strength grades.
Simply increasing forming force may not be enough.
Engineers may need to review:
- bend progression,
- радиус изгиба,
- over-form angle,
- calibration,
- machine rigidity,
- прогиб вала,
- and material consistency.
The line should be engineered for the actual material range expected in production.
Нержавеющая сталь может вести себя иначе, чем углеродистая сталь
Stainless steel may show different springback behavior from conventional carbon steel because of its mechanical properties and work-hardening characteristics.
Surface protection is also more important for many stainless profiles.
Using excessive forming pressure to compensate for springback can therefore create unwanted surface marking as well as dimensional problems.
Tooling surface condition, forming progression, lubrication where appropriate, and controlled calibration become especially important.
When a roll forming machine is expected to process both carbon steel and stainless steel, the production team should not assume that one set of forming values will produce identical geometry across both materials.
Алюминий часто демонстрирует значительную чувствительность к пружинам
Aluminum has a lower elastic modulus than steel and can show noticeable elastic recovery depending on alloy, temper, thickness, and bend geometry.
This does not mean aluminum cannot be roll formed accurately.
It means springback needs to be included in tooling development.
The process may require different:
- переформирование,
- bend progression,
- roller contact,
- and final calibration
from a comparable steel profile.
Surface sensitivity can also make excessive roller pressure undesirable.
Material-specific setup therefore becomes especially important in multi-material production.
Расположение излучины должно оставаться стабильным
Springback correction assumes the bend itself occurs at the correct position.
If the bend line shifts laterally during forming, over-forming cannot solve the underlying dimensional problem.
For example, a flange may have the correct final angle but still have the wrong width because the bend began in the wrong location.
Tooling design should therefore control:
- bend position,
- угол изгиба,
- radius,
- and adjacent feature relationship
together.
Springback compensation is one part of geometry control, not a substitute for accurate tooling.
Adjacent Bends Can Influence One Another
Complex profiles often contain several bends located close together.
When one bend is formed, the resulting material movement can influence neighboring features.
This interaction becomes particularly important in:
- narrow channels,
- возвратные губы,
- boxed sections,
- deep profiles,
- and asymmetrical shapes.
The forming sequence may need to delay one bend until another has developed sufficiently.
If all bends are driven aggressively at the same time, material stress can become difficult to control.
Springback must therefore be evaluated at the profile level rather than one bend at a time.
Asymmetric Profiles Can Show Uneven Recovery
Symmetrical profiles often distribute forming forces more evenly.
Asymmetric profiles do not.
One side may contain several bends while the other side remains relatively flat.
This can create differences in longitudinal strain and springback behavior across the strip.
The result may include:
- крутить,
- камбер,
- unequal flange angles,
- or lateral movement.
Tooling design may use side rolls, additional calibration, or a modified flower pattern to help stabilize the profile.
The solution depends on the actual cross-section rather than one standard springback correction.
Punched Holes Can Affect Local Forming Behavior
Many roll formed components are punched before forming.
Holes and slots remove material locally.
When these features sit close to a bend, they can influence the way the surrounding strip deforms.
A slotted solar channel, for example, may behave differently around a densely punched region than around an unpunched section.
This can affect:
- угол изгиба,
- форма отверстия,
- local stiffness,
- and final hole position.
Punching and forming should therefore be developed together for high-accuracy components.
JBLDIE's формовочные машинные решения can combine feeding, punching, forming, and cutting according to the profile and production sequence, making coordination between these processes important when final dimensions depend on both punching and bending.
Cutting Can Reveal Residual Stress
A profile may appear stable while it remains part of a continuous strip.
After cutting, residual stresses are partially released.
Готовый компонент может тогда
- open,
- close,
- крутить,
- боу,
- or develop end flare.
This behavior is related to the same stored elastic and residual stresses involved in springback.
For this reason, profile inspection should not be completed only before the cut-off operation.
Finished parts should be measured after cutting and after sufficient release from the tooling.
A profile that meets the drawing only while still restrained inside the machine is not yet a qualified finished product.
Springback and End Flare Are Related but Not Identical
Springback generally describes elastic recovery after bending.
End flare describes a change in cross-section near the cut end of a roll formed profile.
Both involve residual stress, but they appear differently.
A profile may maintain a consistent flange angle through most of its length while opening significantly near the first several centimeters after cutting.
Trying to correct end flare by globally increasing over-forming can distort the central section.
The production team should therefore distinguish between:
- general angular springback,
- localized end flare,
- боу,
- и крутить.
Each may require a different correction strategy.
Temperature and Production Conditions Can Influence Repeatability
Cold roll forming is generally performed without deliberately heating the complete strip, but machine and material temperatures can still change during extended production.
Tooling, bearings, drives, and material-contact areas can warm as the line runs.
For extremely tight dimensional requirements, production teams may observe slight differences between startup conditions and stable continuous operation.
This is another reason first-piece inspection should be followed by in-process inspection.
A correct first profile does not guarantee that the process remains centered during a long production run.
Tool Wear Changes Springback Compensation
Tooling wear gradually alters the effective forming geometry.
Suppose a roll surface responsible for over-forming a flange wears over time.
The tooling may no longer impose the same loaded angle.
The operator then sees more springback in the finished profile, even though the material behavior itself has not changed.
This can lead to repeated manual adjustments.
Maintenance records and dimensional trends can help separate true material-related springback from tooling deterioration.
When a dimension drifts gradually over weeks or months rather than changing suddenly with a new coil, mechanical wear deserves closer investigation.
Shaft Deflection Can Look Like Springback
During forming, the rollers apply load through the shafts.
If shaft stiffness is insufficient for the material and profile, the shaft can deflect under load.
The roll gap then becomes different during forming than it appears when the machine is stopped.
The finished flange may therefore leave the stand less formed than expected.
Operators may describe this as springback, but the actual cause is a mechanical change in tooling position under load.
Machine rigidity, shaft diameter, shaft span, bearing arrangement, and stand construction should therefore match the expected forming force.
How to Measure Springback Correctly
Springback should be measured on the finished unloaded profile.
Useful measurements can include:
- угол изгиба,
- внутренний радиус,
- ширина фланца,
- габаритная ширина,
- высота секции,
- and assembly fit.
The measurement location should be standardized.
Avoid measuring one sample close to the cut end and another at the center if end flare is present.
Use the same:
- datum,
- measuring tool,
- part orientation,
- and distance from the end
when comparing production samples.
Repeatable measurement is essential before the process can be adjusted intelligently.
First-Piece Testing Establishes the Compensation Baseline
When a new profile or material is commissioned, first-piece testing helps establish how much springback occurs under actual production conditions.
A practical process is:
- Install tooling according to the design baseline.
- Verify incoming material.
- Produce a trial profile.
- Measure finished angles and dimensions.
- Compare results with the drawing.
- Identify whether deviation is caused by springback or setup.
- Adjust the relevant forming or calibration pass.
- Produce another sample.
- Record the successful setting.
This process should be systematic.
Changing multiple stands at once makes it difficult to understand which adjustment created the improvement.
Use Several Samples, Not One
Springback control is about repeatability.
One profile reaching exactly 90 degrees does not prove that the process is stable.
Several consecutive samples should be measured.
If the angle varies between:
89.5° → 91.0° → 90.2° → 92.0°
the issue is not simply average springback.
The process itself may be unstable.
К числу возможных причин относятся
- вариация материала,
- roll movement,
- отслеживание полос,
- loose tooling,
- нестабильность питателя,
- or changing machine conditions.
Springback compensation should be applied only after the underlying process demonstrates reasonable repeatability.
Springback Troubleshooting Table
| Symptom | Возможная Причина | First Check |
|---|---|---|
| Bend consistently too open | Material springback or insufficient over-form | Material and final forming pass |
| Angle changes after coil change | Different material properties | Coil grade and thickness |
| One flange differs from the other | Alignment or asymmetric forming | Entry centerline and tooling |
| Angle gradually changes over time | Tool wear or machine movement | Rollers, shafts and bearings |
| Correct before cutting, open after cutting | Residual stress | Cutting and forming progression |
| Only ends open | End flare | Final passes and cut-off condition |
| Angle varies randomly | Process instability | Material, roll gap and mechanical looseness |
| More pressure causes surface marks | Over-tight tooling | Reassess compensation method |
How Simulation Can Help
For complex sections and advanced materials, forming simulation can help predict areas where high strain or springback may develop.
Simulation is particularly useful when:
- material strength is high,
- geometry is complex,
- tooling changes would be difficult,
- or tolerance requirements are demanding.
However, simulation depends heavily on accurate input data.
Material models, thickness, mechanical properties, friction assumptions, tooling geometry, and process conditions all influence the prediction.
Physical trial forming and measurement remain important for final validation.
Simulation should therefore support tooling engineering rather than replace real production verification.
How to Reduce Springback Variation in Production
Stable springback control depends more on consistency than on extreme forming force.
A practical production strategy includes:
Control incoming material
Use the specified grade and thickness range.
Standardize roll gaps
Return tooling to documented baseline settings.
Maintain centerline
Keep the strip aligned through entry and forming.
Inspect tooling
Watch for wear and contamination.
Use controlled over-forming
Compensate for expected elastic recovery.
Calibrate final geometry
Use later passes for controlled correction.
Measure after cutting
Verify the actual unloaded finished component.
Record coil and dimensional data
Identify material-related trends.
Change one parameter at a time
Build repeatable process knowledge.
This approach turns springback from an unpredictable defect into a controllable manufacturing variable.
When Tooling Redesign May Be Necessary
Machine adjustment has limits.
If the material range or profile requirement changes significantly from the original design, the existing tooling may no longer provide sufficient control.
A tooling review may be needed when:
- significantly higher-strength material is introduced,
- thickness range changes substantially,
- bend radius changes,
- tighter tolerances are required,
- profile geometry changes,
- additional punched features are added,
- or repeated adjustments cannot create stable results.
In these situations, modifying the flower pattern or selected roll geometry can provide a more robust solution than continuing to compensate through machine settings.
What Information Is Needed Before Designing for Springback?
Accurate springback compensation begins with complete engineering information.
Useful data includes:
Finished profile drawing
Include bend angles, radii, flanges, lips, and critical dimensions.
Материальный сорт
Specify actual steel, stainless steel, aluminum, or other material.
Механические свойства
Provide relevant strength data where available.
Диапазон толщины
Include minimum, maximum, and normal thickness.
Ширина полосы
Confirm incoming coil width requirements.
Tolerance requirements
Identify which dimensions are functionally critical.
Punching features
Show holes or slots near bend locations.
Требования к поверхности
Indicate whether the material is coated or appearance-sensitive.
Метод резки
Clarify whether cutting occurs before or after forming.
Ассортимент продукции
Identify whether one line needs several materials or profile sizes.
The more accurately these conditions are defined, the more realistically the tooling can be engineered around springback.
How to Evaluate Springback During Machine Acceptance
Factory or site acceptance should use representative material whenever possible.
Finished samples should be checked after they leave the tooling and are cut to their normal product condition.
Important measurements may include:
- угол фланца,
- радиус изгиба,
- габаритная ширина,
- высота секции,
- прямолинейность,
- крутить,
- end condition,
- положение отверстия,
- and assembly fit.
If several steel grades or thicknesses are part of the agreed production range, representative material changes should be tested where practical.
The objective is to confirm that the machine and tooling can maintain the required geometry across the specified production conditions rather than only with one ideal coil.
Заключение
Roll forming springback is a normal result of elastic recovery after metal is bent, but it can become a significant source of dimensional variation when material behavior is not considered during tooling and process design.
Yield strength, elastic modulus, thickness, bend radius, profile geometry, forming sequence, roll gaps, tooling wear, machine stiffness, punching, and cutting can all influence the final amount of recovery.
The most common compensation method is controlled over-forming, often supported by final calibration passes. However, over-forming works reliably only when the incoming material and machine setup remain consistent.
Manufacturers should therefore treat springback as part of the complete roll forming process rather than as a final-stand adjustment.
A stable strategy begins with accurate material information and profile drawings, develops the correct flower pattern, establishes controlled over-forming, verifies the finished unloaded profile, and records successful machine settings for future production.
When these factors are managed systematically, springback becomes a predictable engineering consideration rather than a recurring production problem.
Часто задаваемые вопросы
What is roll forming springback?
Roll forming springback is the elastic recovery that occurs after metal leaves the forming rolls. The material partially returns toward its original shape, which can change bend angles, radii, and finished profile dimensions.
What causes excessive springback in roll forming?
Springback is influenced by material yield strength, elastic modulus, thickness, bend radius, profile geometry, forming progression, and tooling conditions. Higher-strength or thinner materials can be particularly sensitive.
How is springback compensated in roll forming?
A common method is controlled over-forming, where the tooling bends the material slightly beyond the required final angle. After elastic recovery, the profile moves toward its target geometry. Final calibration passes can provide additional correction.
Can tighter roll gaps eliminate springback?
Not reliably. Excessive roll pressure can create surface damage, tooling wear, distortion, or additional residual stress. Springback should be controlled through material-aware tooling design, forming progression, over-forming, and calibration.
Why does springback change after switching coils?
Different coils can vary in thickness, strength, residual stress, or other mechanical characteristics. These differences can change how much elastic recovery occurs even when the machine settings remain unchanged.
Need to Control Springback in a Roll Formed Profile?
Springback compensation should be developed around the actual material, thickness, bend radii, profile geometry, tolerances, punching features, and cutting process. If you are evaluating tooling or a new roll forming production line, связаться JBLDIE to discuss your profile drawings and forming requirements.
 Russian
 English
 Arabic
 Spanish
 French