
Photovoltaic Bracket Production Line: 7 Buyer Checks
Table of Contents
Introduction
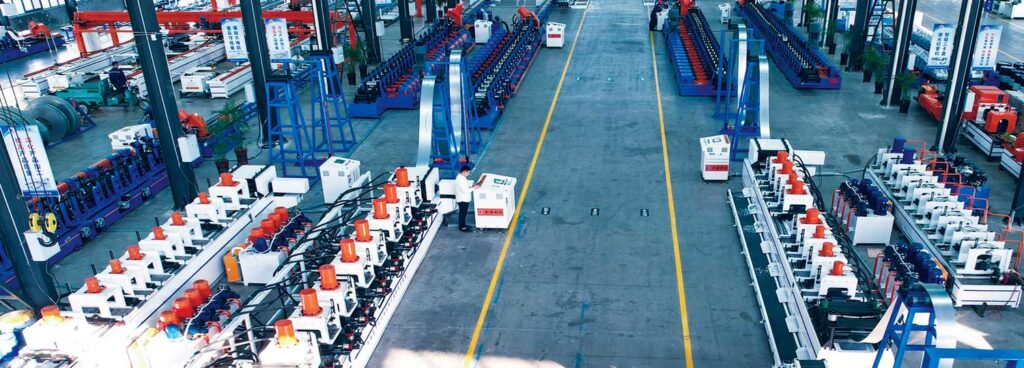
Photovoltaic manufacturing is entering a stage where production volume alone is no longer enough to define a competitive factory. Solar projects are becoming more diverse, photovoltaic deployment continues to expand across more countries, and mounting-system manufacturers increasingly need to support different profiles, hole patterns, materials, batch sizes, and project specifications.
According to the IEA PVPS Snapshot of Global PV Markets 2026, approximately 698 GW of new photovoltaic capacity was installed worldwide in 2025, bringing cumulative global PV capacity close to 3 TW. The report also notes that system integration and flexibility are becoming increasingly important as the global photovoltaic market develops.
For manufacturers of mounting structures, this changes how a photovoltaic bracket production line should be evaluated.
The most important question is no longer simply:
How fast can the roll forming machine run?
A more useful question is:
Can the complete production line repeatedly manufacture the actual C-channel, U-channel, Z-profile, strut channel, connectors, and punched components required by different photovoltaic projects?
Machine flexibility, punching accuracy, tooling changeover, material compatibility, qualified production output, automation, maintenance accessibility, and quality verification are becoming increasingly important procurement considerations.
This guide examines seven areas manufacturers should evaluate before selecting or configuring a photovoltaic bracket production line.
Why PV Bracket Equipment Requirements Are Changing
The photovoltaic market is expanding not only in scale but also in the range of system applications.
Utility-scale projects remain an important part of global deployment, while applications such as agrivoltaics, floating PV, infrastructure-integrated PV, commercial rooftops, and other project formats continue to develop.
These projects do not necessarily use identical mounting structures.
Different systems may require different:
- channel dimensions,
- post profiles,
- connector components,
- material thicknesses,
- corrosion-protection requirements,
- mounting-hole patterns,
- finished lengths,
- and assembly interfaces.
This creates an important manufacturing issue.
A factory designed around one fixed bracket profile can be highly efficient when production remains stable. But a manufacturer supplying several solar mounting projects may need much greater flexibility.
For equipment buyers, the correct production line therefore depends on the expected product portfolio, not simply on the current highest-volume bracket.
Buyer Check 1: Can the Line Produce Your Real Profile Range?
The first procurement question should be based on finished drawings.
A photovoltaic bracket production line may need to manufacture:
- C-channel supports,
- lipped C profiles,
- U-channel supports,
- Z-shaped profiles,
- strut channels,
- ground-mount posts,
- connector plates,
- clamps,
- and customized project-specific sections.
These products may belong to the same photovoltaic mounting system but require very different production processes.
JBLDIE’s Solar Photovoltaic Bracket Forming Machine category includes equipment for several photovoltaic profile and component types.
The key procurement issue is determining which of your products can realistically share one production line.
Do Not Assume One Machine Can Produce Every Profile
A machine advertised as “multi-profile” should be evaluated carefully.
Ask exactly how the profile changes.
Does the machine use:
- adjustable rollers,
- motorized roll positioning,
- interchangeable tooling,
- replaceable cassettes,
- common-roll tooling,
- or completely separate roll sets?
A 40 mm C-channel and a related 50 mm C-channel may potentially share more tooling than a C-channel and a completely different ground-mount post.
Technical feasibility and practical production flexibility are not the same thing.
A machine may technically produce multiple profiles but require so much manual tooling replacement that frequent changeovers become inefficient.
Dedicated vs Flexible Production Lines
Equipment buyers should compare the benefits of dedicated and flexible production strategies.
| Factor | Dedicated Profile Line | Flexible Multi-Profile Line |
|---|---|---|
| Main production goal | High-volume stable product | Multiple specifications |
| Tooling | Profile-specific | Adjustable or interchangeable |
| Setup complexity | Lower | Higher |
| Changeover | Limited or infrequent | Important design requirement |
| Operator adjustments | Usually fewer | Depends on automation |
| Best fit | Long production campaigns | Project-based or mixed production |
| Main procurement concern | Stability and output | Repeatability after changeover |
Neither approach is automatically better.
A mounting-system manufacturer producing one dominant C-channel around the clock may benefit from dedicated tooling.
A factory supplying different EPC projects with changing section dimensions may place far more value on flexible adjustment.
The annual product mix should therefore be provided before equipment configuration begins.
Buyer Check 2: Can the Equipment Handle Future Material Requirements?
Photovoltaic brackets are commonly produced from galvanized steel and other coated or corrosion-resistant materials.
The machine should therefore be evaluated against the actual material range rather than a single nominal thickness.
Important information includes:
- steel grade,
- minimum thickness,
- maximum thickness,
- yield strength,
- strip width,
- galvanized coating,
- other coating systems where applicable,
- coil weight,
- coil inner diameter,
- and coil outer diameter.
Material properties directly influence the forming process.
Higher-strength steel can require greater forming force and may show more springback.
Thinner materials may become more sensitive to:
- edge wave,
- roll pressure,
- guide contact,
- and local deformation.
Thicker materials increase load on:
- shafts,
- bearings,
- roll stands,
- gearboxes,
- and drive systems.
A machine should therefore be engineered for the intended combination of profile geometry and material properties.
Do Not Evaluate Only Maximum Thickness
A common equipment comparison is:
Machine A: 1.5–3.0 mm
Machine B: 1.0–3.5 mm
This information alone is incomplete.
Three-millimeter mild steel and three-millimeter high-strength steel do not necessarily create identical forming loads.
Similarly, two profiles using the same material thickness may require substantially different forming forces because one contains:
- deeper bends,
- return lips,
- more complex geometry,
- or a wider strip.
Ask the equipment supplier what material and profile assumptions were used when defining the machine range.
Protecting Galvanized Surfaces
PV mounting structures frequently operate outdoors, making coating condition an important finished-product consideration.
The production line should protect galvanized surfaces throughout:
decoiling → leveling → feeding → punching → forming → cutting → unloading → stacking
Possible sources of coating damage include:
- damaged rollers,
- dirty guides,
- punching debris,
- excessive roll pressure,
- metal-to-metal sliding,
- rough receiving tables,
- and uncontrolled stacking.
Equipment procurement should therefore include questions about both profile accuracy and surface handling.
A profile with perfect dimensions but repeated coating scratches can still create a production-quality problem.
Buyer Check 3: How Flexible Is the Punching System?
Punching is one of the most important differences between photovoltaic bracket manufacturing and ordinary profile production.
Solar mounting profiles can contain:
- round holes,
- elongated slots,
- connection holes,
- locating holes,
- side holes,
- mounting openings,
- and customized project-specific patterns.
JBLDIE’s Solar Photovoltaic Rack Punching Equipment includes three-, six-, and nine-station configurations for different bracket-processing requirements.
Equipment buyers should not ask only:
Does the line include punching?
Instead, ask:
How many different punching operations can it perform, and how are those operations changed between products?
Single-Station vs Multi-Station Punching
A simple solar rail containing one repeated slot may not require a complex punching system.
A profile containing several different features can require multiple dies or stations.
| Punching Requirement | Possible Equipment Direction |
|---|---|
| One repeated hole | Single-station system |
| Multiple hole shapes | Multi-station punching |
| Different project patterns | Programmable servo feeding |
| Holes on several surfaces | More specialized processing |
| Short connectors | Independent connector punching/forming |
| Frequent product changes | Flexible tooling and stored recipes |
| High hole density | Cycle-time optimization |
The number of punching stations should therefore come from the finished component drawings.
More stations are useful only when the product requires them.
Hole Accuracy Matters More Than the Number of Stations
A profile can have the correct cross-section and still fail assembly because its hole pattern is wrong.
Equipment buyers should therefore define:
- hole diameter,
- slot length,
- slot width,
- center-to-center pitch,
- first-hole position,
- final-hole position,
- distance to the cut end,
- and tolerance.
For a long profile containing many repeated slots, cumulative error becomes especially important.
Checking only the distance between two adjacent holes may not reveal that the entire hole pattern gradually shifts along a six-meter profile.
A realistic machine test should therefore inspect the complete finished part.
Pre-Punching or Post-Punching?
This is another important procurement decision.
Pre-Punching
Holes are created while the strip is still flat.
Potential advantages include:
- easier die access,
- simple strip support,
- efficient servo feeding,
- and straightforward integration.
However, later roll forming can influence features positioned near bends.
Post-Punching
The profile is punched after forming or partial forming.
This can reference finished geometry more directly but requires tooling that supports the three-dimensional section.
The correct strategy depends on the actual profile.
The supplier should therefore review the full cross-sectional drawing and hole drawing together before finalizing the process.
Buyer Check 4: What Is the Real Production Capacity?

Maximum line speed is one of the easiest machine specifications to compare—and one of the easiest to misunderstand.
Suppose a roll forming machine can theoretically run at 40 m/min.
That does not mean a production line containing dozens of punching operations will continuously produce finished brackets at 40 m/min.
Actual output may be limited by:
- punching cycle,
- servo feeding,
- stop-to-cut time,
- coil change,
- tooling adjustment,
- unloading,
- stacking,
- quality inspection,
- or operator intervention.
Procurement teams should therefore ask for qualified finished-product capacity, not only forming speed.
Calculate Capacity From the Finished Bracket
Consider two C-channel products.
Profile A
- Few mounting holes
- One standard finished length
- Long production batch
Profile B
- Multiple elongated slots
- Several hole groups
- Frequent length changes
- Short production batches
They may use the same roll forming section.
Their real production capacity can nevertheless be significantly different.
For Profile B, punching and changeover may become more important than forming speed.
This is why machine evaluation should use actual product drawings and expected batch quantities.
Find the Bottleneck Before Selecting Automation
A complete photovoltaic bracket line can be represented as:
decoiling → leveling → feeding → punching → roll forming → straightening → cutting → unloading → stacking
The slowest repeating operation sets practical production capacity.
| Possible Bottleneck | What Buyers Should Ask |
|---|---|
| Coil loading | How long does coil change take? |
| Feeding | Is material movement stable at required acceleration? |
| Punching | How many cycles per finished profile? |
| Roll forming | At what speed does profile quality remain stable? |
| Cutting | Stop-to-cut or tracking cut? |
| Unloading | Can finished profiles leave fast enough? |
| Stacking | Does bundle change interrupt production? |
| Changeover | How long until the next qualified product? |
An expensive automation feature provides little benefit if it does not address the actual bottleneck.
Buyer Check 5: How Long Does Product Changeover Really Take?
Flexible manufacturing has become increasingly relevant as photovoltaic markets diversify.
A production line serving different projects may need to switch between:
- C-channel sizes,
- U-channel sizes,
- different strip widths,
- different material thicknesses,
- different punching patterns,
- and different finished lengths.
A machine supplier may describe this as “fast changeover.”
Buyers should ask exactly what that means.
Measure Changeover From Good Part to Good Part
A useful changeover definition is:
last qualified Product A → first qualified Product B
This includes:
- stopping production,
- tooling adjustment,
- material change,
- punching-die change,
- guide adjustment,
- straightener adjustment,
- cutting setup,
- PLC recipe selection,
- trial running,
- and first-piece inspection.
Changing one roller position in five minutes does not mean the complete line has a five-minute changeover.
This distinction is especially important for factories producing smaller project-based batches.
Ask Which Adjustments Are Automatic
Modern production lines may use:
- motorized roll positioning,
- servo adjustment,
- stored PLC recipes,
- automatic feeder settings,
- programmable hole patterns,
- and automated cutting lengths.
These functions can reduce repeated manual setup.
However, buyers should understand which settings still require:
- mechanical tooling change,
- spacer replacement,
- die replacement,
- manual measurement,
- or operator correction.
A realistic changeover demonstration during FAT can be more informative than a list of automation functions.
Buyer Check 6: How Will Product Quality Be Verified?
As photovoltaic deployment grows, manufacturing quality becomes increasingly important throughout the supply chain.
IEA PVPS Task 13’s 2026 report on Photovoltaic Project Decisions: Quality, Performance, and Economic Value emphasizes the value of early quality assurance, technical due diligence, and component testing in reducing downstream failures.
For bracket production equipment, this means machine acceptance should focus on the finished component, not merely whether each motor and cylinder operates.
What Should Be Included in Finished-Part Inspection?
For a photovoltaic C- or U-channel, the inspection can include:
- web width,
- flange height,
- lip geometry,
- opening width,
- bend angle,
- straightness,
- camber,
- twist,
- hole diameter,
- slot dimensions,
- hole pitch,
- cumulative hole position,
- finished length,
- cut-end condition,
- and surface quality.
Several consecutive products should be inspected.
One good sample is not enough to prove repeatability.
FAT Should Use Representative Products
A realistic Factory Acceptance Test should use material and product specifications that represent actual production where practical.
For a multi-profile line, testing only the easiest profile provides limited information.
A useful FAT program may include:
- a common high-volume profile,
- another profile requiring changeover,
- a product with demanding punching,
- representative material thickness,
- and continuous production for a defined test period.
Buyers should also confirm how measurements will be taken.
The drawing, datum points, measuring instruments, and acceptance method should be agreed before the test.
Test Actual Punching Patterns
Running the material through an empty punching station does not demonstrate the line’s real cycle time.
If the intended product contains 30 slots, the FAT should reflect that actual processing requirement where practical.
Likewise, if several profile lengths will be produced, programmable length changes should be demonstrated.
The closer the test is to real manufacturing, the more useful the result becomes.
Buyer Check 7: Is the Automation Practical to Operate and Maintain?
The solar manufacturing sector increasingly discusses digitalization, smart factories, robotics, and automated production.
These technologies can improve manufacturing—but only when the underlying process is stable.
A photovoltaic bracket production line may integrate:
- servo feeding,
- multi-station punching,
- automatic roll adjustment,
- flying cutting,
- conveyors,
- robotic blanking,
- automatic stacking,
- recipe management,
- production counting,
- alarm diagnostics,
- and production-data collection.
The procurement question should not be:
How much automation does the machine have?
It should be:
Which automation functions improve our actual manufacturing process?
Useful Automation vs Unnecessary Complexity
Automation creates the most value when it solves recurring production problems.
For example:
Frequent size changes
Motorized or servo adjustment may improve repeatability.
Many hole patterns
Programmable servo feeding can reduce mechanical pattern changes.
High output with long profiles
Automated unloading can prevent downstream handling from limiting the line.
Multiple product recipes
Centralized recipe storage can reduce repeated data entry.
Recurring troubleshooting
Alarm history and process data can help identify patterns.
By contrast, automation that adds maintenance complexity without reducing setup, improving quality, or increasing effective output may provide limited practical value.
Ask About Fault Recovery
A production line should not be evaluated only when everything is operating normally.
Buyers should ask what happens when:
- a sensor fails,
- a punch does not return,
- material reaches the wrong position,
- a profile jams,
- a servo alarm occurs,
- the cutter does not complete its cycle,
- or an unloading station remains occupied.
Can operators identify the cause quickly?
Does the HMI show useful diagnostics?
Can the machine restart without losing the product sequence?
Automation quality becomes especially visible during abnormal production conditions.
Maintenance Access Is Part of Machine Design
Equipment should provide practical access to:
- forming rolls,
- bearings,
- shafts,
- guides,
- punching tools,
- hydraulic components,
- electrical cabinets,
- sensors,
- cut-off tooling,
- and lubrication points.
A compact line can save floor space, but excessive crowding can make maintenance difficult.
If operators need to remove several unrelated components to reach one wearing part, routine maintenance becomes more time-consuming.
Procurement teams should therefore inspect maintenance accessibility during machine evaluation.
Current Industry Trend: Flexibility Is Becoming More Valuable
The latest IEA PVPS market data shows that photovoltaic deployment is becoming increasingly global, with nearly 40 countries installing at least 1 GW of PV during 2025.
For bracket manufacturers serving international projects, this can mean greater variation in:
- project standards,
- mounting structures,
- environmental conditions,
- project scale,
- profile dimensions,
- and construction methods.
A factory designed around one permanent bracket specification may still be appropriate for dedicated mass production.
But manufacturers supplying multiple markets should increasingly evaluate how quickly their equipment can adapt to changing profile requirements.
Flexibility should therefore be considered at four levels:
Material Flexibility
Can the machine handle the intended thickness and material range?
Profile Flexibility
Which C, U, Z, strut, or customized sections can share equipment?
Punching Flexibility
How easily can hole patterns change?
Production Flexibility
How quickly can the complete line move from one qualified product to another?
These questions are more meaningful than simply labeling a machine “flexible.”
Current Industry Trend: More Attention to Quality and Traceability
As photovoltaic systems become larger and project lifetimes extend over many years, component quality increasingly matters across development, construction, operation, and maintenance.
For mounting-profile production, practical traceability can include linking finished batches with:
- coil number,
- material grade,
- production date,
- profile recipe,
- punching program,
- machine settings,
- inspection results,
- and operator or shift information
where the factory’s quality system requires it.
This does not mean every factory needs a complex industrial data platform.
Even structured production records can make troubleshooting more effective.
For example, if opening width suddenly changes, production records may show that the change began immediately after a different steel coil entered the line.
Data then supports process investigation rather than simply adding digital features.
Current Industry Trend: Multiple Profile Families Need Better Production Planning
Photovoltaic mounting structures increasingly contain a combination of long profiles and smaller connection components.
A production system may therefore need separate strategies for:
Long members
- C-channels
- U-channels
- rails
- posts
Short components
- connectors
- clamps
- plates
- brackets
Attempting to manufacture every component on one continuous roll forming line may not be efficient.
Long-profile equipment should remain focused on continuous production where possible.
Short components with repeated punching and bending can be handled by dedicated equipment.
This is why manufacturers should evaluate the complete component family rather than one individual machine.
Procurement Checklist Before Final Equipment Configuration
Before equipment configuration begins, buyers should prepare a technical production package.
Product Information
Provide:
- all profile drawings,
- connector drawings,
- hole patterns,
- finished lengths,
- annual product mix,
- normal batch sizes.
Material Information
Provide:
- material grades,
- minimum and maximum thickness,
- strip widths,
- coil dimensions,
- coating requirements.
Quality Information
Define:
- critical dimensional tolerances,
- punching tolerances,
- straightness,
- twist,
- surface requirements,
- applicable standards.
Production Information
Define:
- expected output,
- shift arrangement,
- product-change frequency,
- coil-change requirements,
- automation target.
Factory Information
Provide:
- available floor space,
- material-flow direction,
- crane or forklift access,
- electrical requirements,
- finished-product handling strategy.
The equipment supplier can then design the production line around real manufacturing conditions rather than assumptions.
Questions Buyers Should Ask a PV Bracket Machine Supplier
Before finalizing a photovoltaic bracket production line, procurement and engineering teams can ask:
- Which of our actual profile drawings can run on the same forming line?
- Which products require separate roll tooling?
- Which dimensions can be adjusted automatically?
- Which adjustments remain manual?
- How many punching stations are required for our real hole patterns?
- How is cumulative hole-position error controlled?
- What material grades and thicknesses were used to define machine capacity?
- What is the expected qualified output for our representative product?
- Which operation becomes the bottleneck for our most heavily punched profile?
- How long does a real profile changeover take?
- How will galvanized surfaces be protected?
- How will profile straightness and twist be controlled?
- What will be included in FAT?
- Which actual profiles will be tested?
- What measurements will determine acceptance?
- How are alarms and faults diagnosed?
- Which parts require routine maintenance?
- How easily can operators access punching and forming tooling?
- Can production recipes be stored for repeated products?
- Can the line be expanded or integrated with future handling equipment?
The quality of the answers to these questions usually reveals more than a basic specification sheet.
Red Flags During Equipment Evaluation
Several situations deserve additional technical review.
One Machine Is Claimed to Produce Almost Any Profile
Ask exactly how tooling changes and whether representative drawings have been reviewed.
Production Capacity Is Based Only on Maximum Forming Speed
Request capacity calculations using real punching patterns and finished lengths.
Accuracy Is Stated Without Explaining the Measurement Method
Ask which dimensions, materials, lengths, and operating conditions the figure applies to.
Changeover Is Described as “Automatic” Without a Demonstration
Clarify which mechanical operations remain manual.
FAT Tests Only Machine Motion
Finished brackets should be produced and measured.
Automation Functions Are Extensive but Maintenance Access Is Poor
A highly automated line still requires tooling inspection and component maintenance.
These are not automatic reasons to reject equipment. They are signals that more detailed engineering discussion is required.
How JBLDIE PV Bracket Equipment Fits Different Production Requirements
JBLDIE currently provides photovoltaic bracket equipment covering both long-profile forming and specialized punching applications.
For manufacturers focused on specific C-shaped profiles, the Solar Photovoltaic Bracket C-Channel Steel Roll Forming Machine provides a dedicated reference for C-channel production.
The broader solar bracket equipment range can also include U-channel forming, connector processing, multi-station punching, feeding, cutting, and related automation.
The appropriate configuration should be selected only after reviewing:
- profile drawings,
- material,
- hole patterns,
- production mix,
- batch size,
- required changeover,
- and factory layout.
This approach avoids selecting equipment based only on a generic model name.
Conclusion
The rapid expansion of global photovoltaic deployment continues to create manufacturing opportunities, but it also makes photovoltaic bracket production line selection more demanding.
Modern equipment buyers increasingly need to evaluate more than forming speed.
The seven most important areas are:
- actual profile-range capability,
- material compatibility,
- punching flexibility and accuracy,
- realistic qualified output,
- changeover performance,
- finished-product quality verification,
- and practical automation and maintenance.
A strong production line should be designed around actual bracket drawings and expected project requirements.
For factories producing one stable high-volume profile, dedicated tooling can remain an effective strategy. For manufacturers serving multiple solar projects, adjustable tooling, programmable punching, repeatable changeover, production recipes, and scalable automation can become much more important.
The most useful procurement process therefore starts with the finished products, tests representative manufacturing conditions, identifies the true production bottleneck, and evaluates whether the complete line can repeatedly deliver qualified photovoltaic mounting components.
FAQ
What is a photovoltaic bracket production line?
A photovoltaic bracket production line is a manufacturing system used to produce metal profiles and components for solar mounting structures. It can integrate decoiling, leveling, servo feeding, punching, roll forming, cutting, unloading, and automated handling.
What should buyers check when selecting a PV bracket production line?
Important factors include product range, material specifications, punching requirements, profile accuracy, actual finished-product output, changeover time, automation, maintenance accessibility, and FAT procedures.
Is maximum roll forming speed the same as actual production capacity?
No. Actual output can be limited by punching cycles, feeder movement, cutting, material changes, unloading, stacking, changeover, and quality inspection. Buyers should evaluate complete-line capacity using representative products.
Can one photovoltaic bracket production line make C, U, and Z profiles?
Some related profiles may share parts of a production line, but substantially different sections can require different tooling or equipment. Actual drawings should be reviewed before confirming multi-profile capability.
Why is punching accuracy important for photovoltaic brackets?
Mounting holes and slots determine how bracket components connect during installation. Even when the profile cross-section is correct, inaccurate or cumulatively shifted holes can create assembly problems.
Planning a Photovoltaic Bracket Production Line?
A reliable production-line configuration should begin with your actual C-channel, U-channel, Z-profile, connector, material, punching, tolerance, batch-size, and automation requirements. Contact JBLDIE to discuss your photovoltaic bracket drawings and production plans.
 English
 Arabic
 Russian
 Spanish
 French