
Square Tube Forming Machine: Round vs Direct Forming
Table of Contents
Introduction

Square and rectangular tubes can be produced through more than one forming route. Two of the most common approaches are round-to-square forming, in which flat strip is first formed and welded into a round tube before being reshaped into a square or rectangular section, and direct square forming, in which the strip is progressively formed toward the final square or rectangular geometry without first creating a complete round tube.
For manufacturers evaluating a square tube forming machine, the difference between these two processes affects much more than the appearance of the finished tube. Tooling structure, forming sequence, corner development, size changeover, production range, strip behavior, welding conditions, sizing requirements, and quality control can all change according to the selected method.
Neither process is universally better. Round-to-square forming is a mature and widely used production route that can provide stable processing across many tube specifications. Direct square forming can simplify parts of the deformation path and may provide greater tooling flexibility for certain square and rectangular tube ranges. The appropriate solution depends on the actual product range rather than on the name of the forming technology.
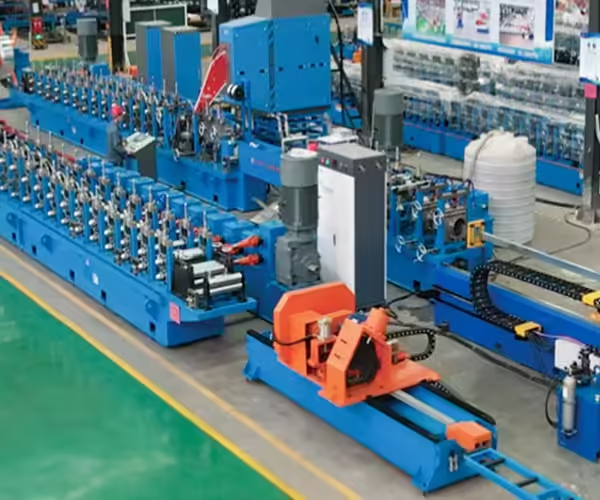
JBLDIE’s Square Tube Forming Machine is designed around continuous tube processing that can include forming, high-frequency welding, sizing, straightening, and related production operations according to the required tube specifications.
What Is a Square Tube Forming Machine?
A square tube forming machine is an industrial production system used to convert metal strip or intermediate welded tube into square or rectangular hollow sections.
A complete production line normally includes more than the forming stands themselves.
Depending on the equipment configuration, the manufacturing process may contain:
- coil loading,
- uncoiling,
- strip joining,
- accumulation,
- strip forming,
- fin-pass forming,
- high-frequency welding,
- weld-bead removal,
- cooling,
- square or rectangular shaping,
- sizing,
- straightening,
- cutting,
- and finished-tube handling.
The exact position at which the square shape is created depends on the selected forming method.
With round-to-square production, most of the initial forming section is designed around creating a round welded tube. Square or rectangular geometry is developed later.
With direct square forming, the strip begins developing the final hollow-section geometry earlier in the process.
This difference changes the entire tooling strategy.
What Is Round-to-Square Tube Forming?
Round-to-square forming is a conventional welded tube manufacturing process in which flat metal strip is progressively formed into an open round section.
The two edges of the strip are then brought together at the welding section and joined to create a continuous round tube.
After welding, scarfing, and cooling, the round tube enters additional sizing and forming stands.
These downstream rolls gradually change the circular cross-section into a square or rectangular profile.
The simplified process is:
steel coil → strip preparation → round forming → HF welding → cooling → square/rectangular reshaping → sizing → straightening → cutting
This method separates the production task into two major stages.
The first stage creates a stable welded round tube.
The second transforms that tube into the required square or rectangular section.
Because round tube manufacturing is highly established, this route remains widely used for many hollow-section applications.
What Is Direct Square Forming?
Direct square forming—also called direct forming to square—changes the forming strategy.
Instead of first creating a complete round tube, the flat strip is progressively bent toward a square or rectangular open section.
The corners and relatively flat faces begin developing before the welding stage.
The strip edges are eventually positioned for welding, after which the welded section continues through calibration and sizing stands to achieve the required final geometry.
A simplified direct-forming route can be represented as:
steel coil → strip preparation → progressive corner forming → open square/rectangular section → HF welding → sizing → straightening → cutting
The important difference is that the material does not undergo the full transformation:
flat → round → square
Instead, the forming progression moves more directly toward the final shape.
This changes how deformation is distributed across the strip and how tooling needs to be configured.
Round-to-Square vs Direct Square Forming
| Factor | Round-to-Square | Direct Square Forming |
|---|---|---|
| Initial forming shape | Round | Square/rectangular development begins directly |
| Welding-stage geometry | Primarily round tube | Near-square or rectangular open section |
| Final shaping | Round tube reshaped after welding | Final profile refined after welding |
| Tooling strategy | Round forming + square sizing tooling | Direct corner and face-forming tooling |
| Deformation path | Flat → round → square/rectangle | Flat → square/rectangle |
| Corner development | Mainly during downstream reshaping | Developed progressively earlier |
| Size change strategy | Depends strongly on roll sets | Can support adjustable/common-roll concepts in suitable designs |
| Production flexibility | Mature for broad tube production | Particularly useful for selected square/rectangular ranges |
| Round tube production | Naturally supported by the line concept | Usually focused on square/rectangular products |
| Best choice | Depends on product mix | Depends on product mix |
The appropriate process should be selected according to the actual tube range, wall thickness, material, quality requirements, and production strategy.
Why Round-to-Square Forming Remains Widely Used
Round-to-square forming has a major practical advantage: the first part of the line follows an established welded-round-tube process.
Forming the strip symmetrically toward a circular shape allows the edges to approach the welding point under a well-understood geometry.
Once the round tube is welded and stabilized, later stands reshape it into square or rectangular sections.
This process can be useful for factories that manufacture both round and shaped tubes.
A production strategy built around round tube forming may allow the same basic mill concept to support:
- round tube,
- square tube,
- rectangular tube,
- and several related tube dimensions,
provided that the tooling and sizing sections are configured accordingly.
For manufacturers whose product portfolio includes a substantial proportion of round tube, this can be an important consideration.
Why Direct Square Forming Was Developed
Direct square forming addresses a different manufacturing objective.
If the factory mainly needs square and rectangular sections, forming every strip into a complete round tube before converting it again into a square shape introduces deformation that does not directly correspond to the final profile.
Direct forming seeks to make the forming route correspond more closely with the finished section.
Instead of gradually bending the entire strip toward a circular shape, the tooling progressively creates:
- corner regions,
- flat faces,
- edge positions,
- and the open section required for welding.
This can make direct forming attractive for production programs focused heavily on square and rectangular hollow sections.
However, the process requires careful tooling design because the strip must remain stable while different regions of the cross-section undergo different amounts of deformation.
Corner Formation Is One of the Biggest Differences
Square and rectangular tubes are defined partly by their corners.
Round-to-square and direct square processes develop those corners differently.
In a round-to-square line, the material first contains continuous curvature around the circumference of the round tube. During downstream reshaping, selected areas are flattened while other areas develop into corners.
The sizing section therefore redistributes an already curved cross-section.
In direct square forming, the corners are introduced progressively from the flat strip.
The tooling designer determines where each corner begins and how its angle develops from one forming stand to the next.
This provides a different level of control over the forming path, but it also makes the flower pattern especially important.
Forming a corner too aggressively can increase local strain, while insufficient control can allow the faces or edges to become unstable.
Corner Radius Must Match the Finished Tube Requirement
A perfectly sharp square corner is generally not the objective in cold-formed structural tubing.
Real square and rectangular hollow sections have defined corner radii.
The appropriate radius depends on:
- tube specification,
- wall thickness,
- material properties,
- product standard,
- downstream use,
- and forming method.
For structural hollow sections, dimensional and material requirements should follow the applicable tube specification.
For example, the American Institute of Steel Construction provides technical information on Hollow Structural Sections (HSS), including square, rectangular, and round sections used in structural applications.
The square tube forming machine should therefore be configured around the required finished tube standard rather than attempting to create the smallest possible corner radius simply for appearance.
Wall Thickness Influences the Forming Strategy
Wall thickness changes how the strip responds during both round and direct forming.
Thinner strip can be more sensitive to local instability, face distortion, and wave formation.
Thicker material requires greater forming force and may create higher loads on shafts, stands, drives, and tooling.
Material strength also matters.
A high-strength steel may resist bending more strongly and exhibit different springback behavior than a lower-strength material at the same nominal thickness.
For this reason, a tube size range cannot be evaluated only by outside dimensions.
A machine designed for one combination of:
tube size + wall thickness + material
may require a substantially different mechanical configuration for another.
The intended material range should therefore be established before selecting between round-to-square and direct forming.
How Strip Width Relates to the Forming Method
Strip width is fundamental to welded tube manufacturing because the flat strip eventually becomes the complete tube perimeter.
The required width is influenced by:
- finished tube dimensions,
- wall thickness,
- corner geometry,
- forming method,
- weld allowance,
- and tooling design.
Round-to-square and direct-forming methods may use different strip-width calculations because the material follows different deformation paths.
Manufacturers should therefore avoid assuming that an existing strip specification for a round-to-square process can automatically be transferred to a direct-forming line.
Strip width should be calculated from the actual tooling design and confirmed through production trials.
Incorrect width can influence edge position at the weld point, dimensional stability, corner formation, and finished section size.
Welding Still Remains a Critical Process
Changing the forming route does not remove the need for stable welding.
Both processes must bring the two strip edges together under controlled conditions before creating the continuous seam.
Important welding-related variables can include:
- strip-edge condition,
- edge alignment,
- weld V geometry,
- high-frequency energy,
- line speed,
- squeeze-roll position,
- squeeze pressure,
- and material characteristics.
The forming section should deliver the edges to the welding station consistently.
If direct square tooling creates uneven longitudinal movement between the two sides of the strip, welding stability can suffer.
Likewise, a round-to-square mill with poor upstream alignment can deliver mismatched edges to the weld point.
The welding section therefore needs to be considered together with the forming method rather than treated as a completely independent system.
Round-to-Square Forming After Welding
After the round tube is welded, it enters a series of sizing and reshaping stands.
The transformation should occur progressively.
The first stands begin flattening selected regions of the circular cross-section.
As the tube advances, four corner regions become more defined and the faces gradually approach the required flat geometry.
For rectangular tube, width and height are controlled independently through the forming progression.
The process needs to avoid creating excessive stress in individual areas of the tube wall.
If reshaping occurs too aggressively, problems may include:
- concave faces,
- convex faces,
- corner distortion,
- twist,
- dimensional variation,
- or seam-related stress.
The sizing strategy should therefore be developed around the specific tube range.
Direct Square Forming Before Welding
In direct square forming, the strip begins developing the final section earlier.
The tooling typically introduces controlled bends at the future corner locations while guiding the relatively flat faces toward their intended positions.
As the forming process progresses, the strip begins to resemble an open square or rectangular tube.
The edges still need to approach the weld point correctly.
This is one of the critical engineering challenges of direct forming.
The tooling must create the desired corner geometry without allowing the open section to lose stability or causing the edges to become mismatched.
Successful direct forming therefore depends strongly on:
- flower-pattern design,
- guide positioning,
- stand alignment,
- roll adjustment,
- material consistency,
- and controlled forming progression.
Tooling Requirements Are Different
The two forming methods require fundamentally different tooling concepts.
A round-to-square line normally includes tooling for:
- initial breakdown forming,
- fin-pass preparation,
- welding,
- round-tube sizing,
- square or rectangular reshaping.
A direct square line uses a forming sequence designed around the final square or rectangular section from an earlier stage.
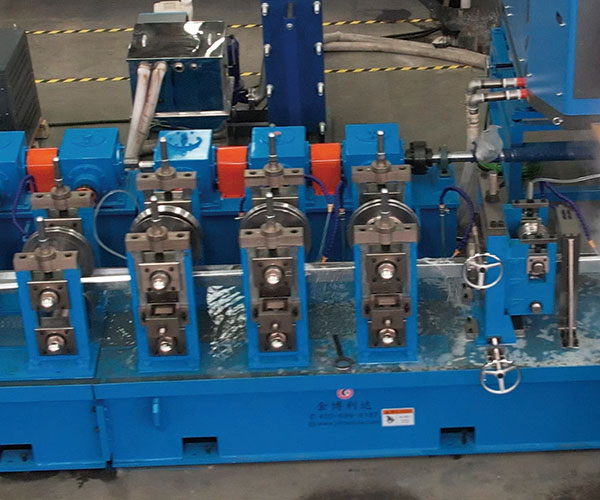
This can allow more use of adjustable or shared rolls within a designed product range.
However, the term “common tooling” should be interpreted carefully.
It does not mean that one universal roll configuration can produce every possible square and rectangular tube.
The range that can share tooling depends on:
- minimum section size,
- maximum section size,
- width-to-height ratio,
- wall thickness,
- corner requirements,
- material,
- stand design,
- and required accuracy.
The actual common-roll range must therefore be defined during machine engineering.
Which Method Is Better for Frequent Size Changes?
This depends on the machine design.
Traditional round-to-square mills often require tooling changes or repositioning when changing between tube sizes.
If many rollers need to be removed, replaced, and realigned, changeover can become a significant part of production time.
Some direct square forming systems are designed around adjustable roll positions so that several tube sizes can share more of the tooling.
This can reduce physical roll replacement for a defined production range.
However, changeover should not be evaluated only by counting roller changes.
Manufacturers should also consider:
- guide adjustment,
- fin-pass setup,
- weld-box adjustment,
- squeeze-roll positioning,
- scarfing setup,
- sizing adjustment,
- straightener setup,
- cut-off configuration,
- and stored control parameters.
The useful measurement is total line changeover time from the last acceptable tube of one size to the first acceptable tube of the next.
Product Range Is More Important Than One Tube Size
A common equipment-selection mistake is evaluating the machine using only one representative tube.
For example, a factory may initially focus on a 100 × 100 mm square tube.
But the actual production program may also include:
- 50 × 50 mm,
- 80 × 80 mm,
- 100 × 50 mm,
- 120 × 60 mm,
- 150 × 150 mm,
- and other sizes.
A machine optimized around one section may not provide the same efficiency across the entire range.
Before selecting a forming method, manufacturers should map the expected production portfolio.
Useful information includes:
| Product Information | Why It Matters |
|---|---|
| Smallest square size | Defines lower forming range |
| Largest square size | Defines structural machine capacity |
| Rectangular sizes | Influences adjustment range |
| Wall-thickness range | Affects load and tooling |
| Material grades | Influences forming force and springback |
| Production share by size | Shows which products deserve optimization |
| Changeover frequency | Influences tooling strategy |
| Round-tube requirement | Can favor a round-based production route |
This product-family approach gives a much more realistic basis for choosing a square tube forming machine.
Round Tube Production Can Affect the Decision
If the factory also needs round tube, round-to-square production may provide a natural advantage.
The upstream line already forms and welds round tube.
When a round product is required, the downstream square-forming section does not need to reshape it into a hollow rectangular section.
When square or rectangular tube is required, additional sizing stands perform the conversion.
A direct square line, by contrast, is generally developed specifically around square and rectangular production.
For a factory dedicated almost entirely to structural square and rectangular profiles, that specialization may be useful.
For a factory that needs a broad combination of round, square, and rectangular tube, the manufacturing strategy may favor a different line configuration.
The correct choice should therefore consider the entire sales and production mix.
Face Flatness Needs to Be Controlled
Square tube is not simply defined by four corners.
The faces between those corners must also meet dimensional and appearance requirements.
Possible problems include:
- concave faces,
- convex faces,
- local wave,
- uneven width,
- face twist,
- and asymmetrical corners.
These defects can develop from incorrect roll positions, uneven material strain, poor tooling progression, welding distortion, or inappropriate sizing pressure.
Direct forming and round-to-square forming control face geometry in different ways.
In round-to-square production, curved portions of the round tube must be flattened progressively.
In direct forming, the relatively flat faces need to remain stable while corner bends are developed.
Neither method removes the need for final calibration.
Finished-tube measurements should therefore include face condition as well as width and height.
Seam Position Must Remain Stable
Weld seam position is important for both manufacturing stability and downstream applications.
If the strip tracks laterally during forming, the seam may move from its intended location.
This can make scarfing, sizing, testing, and downstream fabrication less consistent.
The square tube forming machine should therefore maintain material centerline through:
- entry control,
- forming stands,
- guides,
- fin passes,
- welding,
- and sizing.
When seam movement occurs, operators should determine where the strip begins to shift rather than correcting only the final sizing stands.
Stable upstream forming is essential regardless of whether the process is round-to-square or direct square.
How the Two Methods Affect Roll Adjustment
Roll adjustment is one of the practical differences manufacturers notice during daily production.
Traditional fixed tooling is designed around a specific profile geometry. Producing another size may require replacing rolls or spacers.
Adjustable tooling allows the position of selected rolls to change while retaining more common components.
Direct square systems are often engineered with adjustable-roll concepts because the faces and corners can be controlled through repositioned tooling over a designed range.
Motorized or CNC-controlled adjustment can further reduce manual setting work.
However, automatic positioning does not remove the need for verification.
After a size change, operators should still confirm:
- section width,
- section height,
- corner radius,
- diagonal dimensions,
- wall condition,
- seam position,
- straightness,
- and cut length.
Stored machine settings are a starting point, not a replacement for finished-product inspection.
Production Speed Should Not Be Compared in Isolation
Maximum line speed is often included prominently in tube mill specifications.
But the faster machine is not automatically the more productive machine.
Actual production output depends on:
- coil change frequency,
- strip joining,
- accumulator performance,
- forming stability,
- welding speed,
- cooling,
- sizing,
- cut-off capacity,
- product handling,
- size changeover,
- and quality yield.
For example, one machine may have a higher maximum running speed but require significantly more time between product sizes.
Another may run slightly slower but spend more time producing acceptable tube.
The useful measure is therefore stable finished output over an actual production period.
Quality Control for Square and Rectangular Tube
Quality control should be based on the finished tube specification.
Important measurements commonly include:
- outside width,
- outside height,
- wall thickness,
- corner radius,
- diagonal difference,
- face flatness,
- straightness,
- twist,
- seam position,
- weld condition,
- finished length,
- and surface quality.
For structural hollow sections, the applicable material and dimensional standard should also be identified.
The manufacturing process should therefore be designed backward from the required finished specification.
A square tube that visually appears acceptable may still fail dimensional requirements if width, corner geometry, wall condition, or straightness falls outside the specified range.
Typical Problems in Round-to-Square Forming
Round-to-square production can develop several process-specific problems.
Excessive Face Concavity
If the round tube is converted too aggressively, the central portion of a face may not develop the required flatness.
Tooling progression and sizing pressure should be reviewed.
Uneven Corners
Incorrect roll positioning or tube centering can create differences between the four corner regions.
Twist During Reshaping
Unequal deformation between the sides of the tube can cause the finished section to rotate along its length.
Dimensional Drift
Wear, setup variation, tube temperature, material changes, or sizing-roll movement can affect finished width and height.
These problems should be traced to the stage where they first become visible rather than corrected only at the last stand.
Typical Problems in Direct Square Forming
Direct forming has its own control challenges.
Corner Instability
If corners develop too rapidly or inconsistently, the section can distort before reaching the weld point.
Edge Mismatch
Uneven forming paths can cause the strip edges to arrive at different positions.
Face Wave
Relatively flat areas of the strip may become unstable if longitudinal strain is not controlled.
Asymmetry
Incorrect roll adjustment can produce different corner angles or side dimensions.
Changeover Setup Error
Adjustable tooling improves flexibility but also makes correct position settings important. One incorrectly adjusted stand can affect several finished dimensions.
These are not reasons to avoid direct forming. They simply show why tooling design and setup remain critical.
How to Compare the Two Methods for Your Factory
Instead of asking which technology is generally better, manufacturers should compare them using actual production requirements.
Product Mix
Will the factory produce only square and rectangular tube, or also significant quantities of round tube?
Size Range
How large is the difference between the smallest and largest sections?
Rectangular Ratio
How many rectangular dimensions are required compared with square profiles?
Wall Thickness
What are the minimum and maximum thicknesses?
Material
Will the line process conventional carbon steel, high-strength steel, stainless steel, or other materials?
Changeover Frequency
Will one specification run for several days, or will several sizes be produced in one shift?
Corner Requirements
What corner radii and dimensional tolerances must be maintained?
Production Volume
Which tube sizes account for most annual production?
Downstream Processing
Will tubes later be laser cut, drilled, welded into frames, galvanized, or used directly as structural components?
These questions help identify which forming strategy better supports the factory’s actual operating model.
When Round-to-Square Forming May Be More Suitable
Round-to-square production can be a strong choice when the factory needs a flexible mix of round, square, and rectangular tubing.
It can also suit manufacturers with an established conventional ERW tube mill process, existing tooling experience, and standardized changeover procedures.
The method may be particularly practical when production consists of long runs in relatively stable sizes and tooling change frequency is not a major constraint.
Because the welding stage is based around round-tube forming, operators familiar with conventional tube mills may also find the process easier to standardize.
However, these advantages still depend on the specific machine and production range.
When Direct Square Forming May Be More Suitable
Direct square forming becomes particularly relevant when production is heavily concentrated on square and rectangular hollow sections.
It may also be useful when:
- the line needs to cover several related square sizes,
- frequent size changes are expected,
- adjustable tooling is a major priority,
- round tube is not an important product,
- or the manufacturer wants the forming process focused more directly on the finished geometry.
For larger structural sections, reducing unnecessary intermediate deformation can also become an important design consideration.
However, the benefits depend heavily on correct tooling engineering and the size range for which the line is designed.
Direct forming should therefore be evaluated as a complete production system rather than as a single technological feature.
Factory Acceptance Testing Should Include Multiple Sizes

When a square tube forming machine is intended to produce a wide range of dimensions, testing only one tube size provides limited information.
Factory acceptance testing should ideally evaluate representative products from the required range.
Depending on the project, this might include:
- a smaller square section,
- a larger square section,
- a rectangular section,
- a thinner-wall product,
- and a thicker-wall product.
The purpose is to confirm not only that the machine runs but that size changes and finished quality can be maintained across the specified production range.
Useful FAT checks include:
| FAT Item | What to Verify |
|---|---|
| Forming stability | Tube moves through stands consistently |
| Welding | Seam remains stable |
| Width and height | Match required specification |
| Diagonals | Section remains square |
| Corners | Radius and symmetry are acceptable |
| Face condition | No excessive concavity or convexity |
| Straightness | Finished tube remains within requirement |
| Changeover | Required adjustment method works |
| Cutting | Tube length and end quality are consistent |
| Repeatability | Multiple consecutive tubes remain stable |
A successful sample from one setting should not be the only basis for evaluating a multi-size production line.
What Information Should Be Provided Before Configuring the Machine?
Before configuring a square tube forming machine, the manufacturer should prepare a complete tube list.
The information should include:
Square tube dimensions
List every required width and height.
Rectangular tube dimensions
Provide the complete dimensional range.
Round tube requirements
Clarify whether round products must also be manufactured.
Wall thickness
Define the complete thickness range.
Material grades
Identify the steel or other materials expected to run on the line.
Applicable standards
Specify relevant product standards and tolerance requirements.
Finished lengths
Define the normal and maximum tube lengths.
Production distribution
Identify the sizes that will represent most production volume.
Changeover expectations
State how frequently the factory expects to switch specifications.
Downstream requirements
Describe additional cutting, drilling, laser processing, welding, or handling operations.
With this information, the production line can be engineered around the real manufacturing range rather than a single nominal tube size.
Conclusion
Round-to-square and direct square forming are two different ways of producing square and rectangular welded tubes, and neither method is universally superior.
Round-to-square forming first creates a welded round tube and then progressively reshapes it into the required hollow section. It is a mature process that can fit production environments where round, square, and rectangular tubes share the same broader manufacturing strategy.
Direct square forming begins developing the final square or rectangular geometry earlier, avoiding the complete round intermediate shape. This can be valuable for production programs focused heavily on square and rectangular sections and can support flexible tooling concepts within an engineered size range.
The choice of square tube forming machine should therefore be based on product mix, tube dimensions, wall thickness, materials, corner requirements, welding conditions, size-change frequency, production volume, and downstream processing.
A production line designed around the complete tube portfolio will usually provide a more practical result than selecting a forming process based on one claimed advantage alone.
FAQ
What is a square tube forming machine?
A square tube forming machine is equipment used to produce square or rectangular metal tubing through progressive forming, welding, sizing, straightening, and cutting processes. The line may use round-to-square or direct square forming depending on its design.
What is the difference between round-to-square and direct square forming?
Round-to-square forming first produces a welded round tube and then reshapes it into a square or rectangular section. Direct square forming progressively forms flat strip toward the final square or rectangular geometry before welding and final sizing.
Is direct square forming better than round-to-square forming?
Not universally. Direct forming can be advantageous for certain square and rectangular product ranges, particularly where tooling flexibility and frequent size changes are important. Round-to-square forming can be highly suitable where round tube is also produced or conventional tube-mill processing is preferred.
Can one square tube forming machine produce different tube sizes?
Yes, depending on the machine design and engineered production range. Some lines require roll changes between sizes, while others use adjustable or shared tooling for selected dimensions. The exact capability should be confirmed against the complete tube list.
What information is needed to configure a square tube forming machine?
Important information includes square and rectangular tube dimensions, wall thickness, material grades, required standards, finished lengths, round-tube requirements, expected production volume, changeover frequency, and downstream processing requirements.
Need to Evaluate a Square Tube Production Line?
Choosing between round-to-square and direct square forming should begin with the complete tube range rather than one individual size. If you are planning square or rectangular tube production, contact JBLDIE to discuss your tube dimensions, wall thickness, materials, production mix, and line configuration requirements.
 English
 Arabic
 Russian
 Spanish
 French