
Photovoltaic Solar Bracket Machine: 2026 Buying Checklist
Table of Contents
Key Takeaways
- Start with the finished bracket drawing, not the machine quotation.
- Confirm profile dimensions, material grade, thickness, coating, hole pattern, and annual output.
- Compare actual production capacity instead of relying only on maximum line speed.
- Check whether punching, roll forming, cutting, and stacking should be integrated.
- Request a factory acceptance test using your real material and product drawings.
- Evaluate tooling life, changeover time, spare parts, training, and after-sales support.
- Choose a photovoltaic solar bracket machine according to total production value, not only initial price.
A photovoltaic solar bracket machine is a major investment for manufacturers supplying solar mounting rails, C-channels, U-channels, posts, purlins, and related support components. The machine directly affects profile accuracy, punching consistency, production capacity, material utilization, assembly efficiency, and long-term operating costs.
However, machine quotations can be difficult to compare. One supplier may emphasize maximum speed, while another focuses on automation, tooling, or punching capacity. These specifications only become meaningful when they are matched with your actual bracket drawings, material requirements, production volume, and factory conditions.
This buying checklist explains how to evaluate a photovoltaic solar bracket machine from a practical B2B purchasing perspective.
What Is a Photovoltaic Solar Bracket Machine?
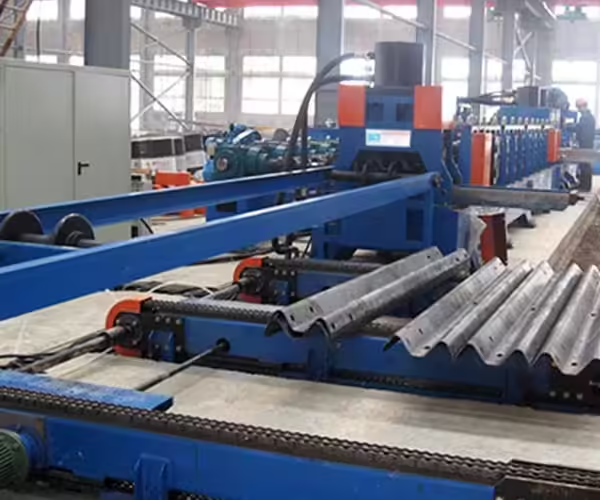
A photovoltaic solar bracket machine is an industrial production system used to form metal coils into structural profiles for solar panel mounting systems. The line normally processes galvanized steel, carbon steel, or other coated materials through a series of precision forming rollers.
Depending on the required product, the system may also include decoiling, leveling, servo feeding, punching, roll forming, cutting, welding, marking, stacking, and digital production monitoring.
Manufacturers can explore different configurations in the solar photovoltaic bracket forming machine category.
Continuous Roll Forming
Continuous roll forming gradually bends a metal strip through multiple roller stations. Each station makes a controlled change until the material reaches the required profile.
This process is suitable for high-volume production because it provides repeatable dimensions and can continuously process long profiles.
Integrated Punching and Cutting
Solar brackets often require mounting holes, slots, connector holes, and fixed cut lengths. An integrated line can complete these processes without repeatedly moving the material between separate machines.
The final configuration depends on the hole pattern, bracket length, production speed, and required tolerance.
Why the Buying Checklist Must Start with the Finished Product
A common purchasing mistake is asking suppliers for a general machine price before providing a complete product specification.
A reliable machine proposal should be based on the finished component rather than a general description such as “solar bracket” or “C-channel.” Two products that look similar may require different roller stations, shaft sizes, motor power, punching systems, tooling, and control programs.
Before requesting a quotation, prepare:
- Finished profile drawings
- Cross-sectional dimensions
- Product length range
- Hole dimensions and spacing
- Slot shape and orientation
- Material grade
- Material thickness range
- Coating specification
- Dimensional tolerance
- Annual or monthly production target
- Required automation level
- Factory layout and available utilities
The more complete the information, the more accurate the machine configuration and quotation will be.
1. Confirm the Solar Bracket Profiles You Need to Produce
The first step is identifying every profile that the photovoltaic solar bracket machine must manufacture.
Common profiles include:
- C-channel rails
- U-channel supports
- Z-shaped purlins
- Hat-shaped channels
- Strut channels
- Ground-mount posts
- Solar tracker components
- Connector plates
- Custom open profiles
C-Channel Solar Brackets
C-channels are widely used because they provide structural strength while remaining relatively easy to connect, transport, and install.
A dedicated solar photovoltaic bracket C-channel steel roll forming machine may be suitable when the factory has stable, high-volume C-profile orders.
U-Channel Solar Brackets
U-shaped profiles are frequently used as rails, support members, connecting structures, and installation components.
Factories focused on U-shaped products can review the configuration of a solar photovoltaic bracket U-channel steel forming machine.
Single-Profile vs Multi-Profile Production
A single-profile machine normally offers simpler tooling, faster adjustment, and stable mass production. A flexible production line can cover several dimensions or profile families but may require replaceable rollers, adjustable stands, or intelligent changeover systems.
| Production Requirement | Recommended Configuration | Main Advantage | Main Consideration |
|---|---|---|---|
| One stable C-channel size | Dedicated C-channel line | Simple and efficient | Limited product flexibility |
| Several C-channel sizes | Adjustable or cassette tooling | Wider product range | Longer setup time |
| C- and U-channel production | Multi-profile or changeover line | Flexible order handling | More complex tooling |
| Many customized profiles | Modular production line | Supports varied projects | Higher initial investment |
| Small connector components | Separate punching and forming system | Specialized production | Additional material handling |
The correct choice depends on whether your business is based on standardized mass production or customized project orders.
2. Match the Machine with the Raw Material
The same profile geometry may behave differently when the material grade, thickness, yield strength, or coating changes.
Therefore, the supplier must know the actual raw material before designing the rollers and calculating the machine structure.
Material Thickness
A wider thickness range creates greater tooling and adjustment requirements. A line designed around thin material may not have enough shaft strength or motor capacity for thicker, higher-strength steel.
Avoid providing only the maximum thickness. Give the supplier:
- Minimum thickness
- Normal production thickness
- Maximum thickness
- Thickness tolerance
- Expected percentage of orders at each thickness
Yield Strength and Formability
Higher-strength steel normally creates greater forming resistance and springback. The machine may require more forming stations, larger shafts, stronger bearings, additional power, or a revised roller design.
Material strength should therefore be included in the technical agreement, not discussed only after the machine has been manufactured.
Galvanized and Coated Steel
Solar mounting structures frequently use galvanized or metallic-coated steel for corrosion resistance. The current ASTM A653/A653M specification covers hot-dip zinc-coated and zinc-iron alloy-coated steel sheet in coils and cut lengths.
When processing coated material, evaluate:
- Surface scratching
- Zinc coating damage
- Roller cleanliness
- Tooling surface finish
- Lubrication requirements
- Protective film compatibility
- Burr control after punching and cutting
A properly designed photovoltaic solar bracket machine should form the profile without causing unacceptable damage to the protective coating.
3. Calculate the Required Production Capacity
Maximum forming speed does not equal actual factory output.
Real production capacity is affected by:
- Coil loading time
- Material feeding
- Punching frequency
- Product length
- Cutting cycle
- Profile changeover
- Tool adjustment
- Quality inspection
- Scheduled maintenance
- Unplanned downtime
- Operator efficiency
- Finished-product handling
A machine rated at a high speed may still deliver low output when the punching system, cutter, stacking process, or material loading becomes the production bottleneck.
Use Finished Pieces as the Main Output Unit
Ask suppliers to estimate output in:
- Pieces per hour
- Pieces per shift
- Tons per month
- Meters per day
- Coils per shift
These figures should be calculated using your normal product length and hole pattern.
For example, Jinbolida’s existing C-channel and U-channel product configurations list forming speeds of up to 45 meters per minute. However, the actual output of a photovoltaic solar bracket machine should still be confirmed through the complete forming, punching, cutting, and material-handling cycle.
Check the Bottleneck
The fastest component does not determine the output. The slowest repeated process does.
If the roll former runs faster than the punching station, the punching cycle controls production. If the forming and punching sections are fast but operators manually collect long profiles, stacking may become the bottleneck.
Ask the supplier to provide a complete cycle-time analysis.
4. Select the Right Production-Line Configuration
A basic photovoltaic solar bracket machine may include:
- Hydraulic or manual decoiler
- Coil loading device
- Leveling unit
- Servo feeding system
- Pre-punching station
- Roll forming section
- Straightening device
- Servo tracking cutter
- Run-out table or automatic stacker
- PLC and HMI control system
More advanced systems may add welding, marking, robotic handling, automatic packing, production-data collection, and remote diagnostics.
Companies planning a higher level of automation can review the photovoltaic equipment production line options.
Integrated Line vs Separate Machines
| Factor | Integrated Production Line | Separate Machines |
|---|---|---|
| Material handling | Minimal | More transfers required |
| Labor demand | Lower | Usually higher |
| Hole-position consistency | Easier to control | Depends on repeated positioning |
| Factory space | Compact linear layout | Multiple work areas |
| Production flexibility | High when properly designed | Individual processes are flexible |
| Initial investment | Usually higher | Can be introduced gradually |
| Production management | Centralized | Multiple controls and operators |
| Maintenance impact | One section may affect the line | Individual machines can operate separately |
An integrated line is often appropriate for repeatable, high-volume products. Separate machines may be more practical when order quantities are small, hole patterns vary frequently, or the factory already owns compatible punching equipment.
5. Evaluate Punching and Cutting Accuracy
Hole position is critical because solar brackets must align with connectors, fasteners, foundations, modules, and other structural components.
Even when the profile dimensions are correct, inaccurate holes can increase assembly time or make the finished component unusable.
Punching Questions to Ask
- Is punching completed before or after forming?
- What is the guaranteed hole-position tolerance?
- How is cumulative error controlled?
- Can the system produce round holes and elongated slots?
- How many punching stations are included?
- Can different hole patterns be stored as recipes?
- How long does a die change require?
- Is slug removal automatic?
- What is the expected punch and die life?
- Does changing material strength affect punching speed?
Flying Cut vs Stop-to-Cut
A stop-to-cut system temporarily stops material movement during cutting. It is usually simpler but may reduce output.
A flying or servo tracking cutter moves with the profile during cutting. It can support continuous production but requires accurate synchronization and a more advanced control system.
The choice should be based on required speed, length tolerance, profile stability, and budget.
6. Inspect the Roll Tooling and Changeover Method

Roll tooling determines whether the photovoltaic solar bracket machine can consistently produce the required profile.
Ask the supplier to explain:
- Roller material
- Heat treatment
- Surface hardness
- Roller machining accuracy
- Shaft material and diameter
- Bearing brand and specification
- Number of forming stations
- Roller replacement method
- Adjustment points
- Tooling warranty
- Spare roller availability
Why More Roller Stations Are Not Always Better
A complex or high-strength profile may need more gradual forming steps. However, adding unnecessary stations increases machine length, adjustment points, maintenance, and cost.
The supplier should justify the number of stations according to the profile geometry and material properties.
Changeover Time
Factories producing many bracket sizes should request a documented changeover procedure.
Compare:
- Manual spacer adjustment
- Adjustable roller stands
- Replaceable roller cassettes
- Automatic width adjustment
- Stored digital recipes
- Full tooling replacement
A flexible machine is valuable only when changeovers are repeatable and practical for operators.
7. Review the Control and Automation System
Automation should reduce production variation, not simply add complicated electronic components.
A practical control system may include:
- PLC control
- Touchscreen HMI
- Servo feeding
- Length control
- Punching recipe storage
- Production quantity setting
- Alarm history
- Fault diagnostics
- Coil usage records
- Energy monitoring
- Remote technical support
- Shutdown memory
- User permission levels
Production Recipe Management
Recipe management allows operators to select a product specification and automatically load the corresponding length, hole pattern, quantity, and processing sequence.
This is especially useful when a photovoltaic solar bracket machine frequently switches between project orders.
Remote Diagnostics
Remote diagnostics can reduce troubleshooting time when the supplier is located overseas. Before purchasing, confirm what data can be accessed, how network security is managed, and whether local operators can still run the machine if remote access is unavailable.
8. Check Factory Layout and Utility Requirements
The quotation should include more than the machine body.
Request a complete layout showing:
- Machine length and width
- Coil loading area
- Raw material storage
- Finished-product collection
- Operator position
- Electrical cabinet location
- Maintenance access
- Safety fencing
- Material movement route
- Crane or forklift access
- Foundation requirements
Utility Checklist
Confirm:
- Voltage and frequency
- Total installed power
- Normal operating power
- Compressed air pressure
- Hydraulic oil requirements
- Cooling requirements
- Network connection
- Ambient temperature
- Floor load
- Earthing requirements
The layout must allow enough space for coil handling, tooling replacement, maintenance, and finished-profile storage.
9. Establish a Factory Acceptance Test
Never rely only on a no-load demonstration.
The factory acceptance test, or FAT, should use the agreed material, profile drawing, thickness, hole pattern, and production length.
| FAT Item | What to Verify | Suggested Evidence |
|---|---|---|
| Profile dimensions | Cross-section matches drawing | Caliper or inspection report |
| Product length | Cut length remains within tolerance | Multiple measured samples |
| Hole position | Hole spacing and edge distance | Inspection template or CMM |
| Surface quality | No unacceptable scratches or coating damage | Visual inspection |
| Line speed | Stable output at agreed conditions | Timed production test |
| Changeover | Adjustment procedure and duration | Recorded changeover trial |
| Control recipes | Correct automatic program selection | Multiple product tests |
| Emergency stops | Safe and correct shutdown | Safety-function test |
| Continuous operation | Stability under extended production | Agreed endurance test |
| Documentation | Manuals, drawings, parts lists | Document checklist |
The acceptance agreement should define how many samples will be measured, which tools will be used, and what happens if the result does not meet the agreed tolerance.
10. Assess the Supplier’s Engineering and Service Capability
The machine itself is only one part of the project.
A qualified supplier should be able to review drawings, identify forming risks, recommend process steps, test raw material, prepare technical documentation, install the line, train operators, and provide spare parts.
Supplier Evaluation Questions
Ask the supplier:
- Have you produced a similar profile before?
- Can you provide a sample-production video?
- Can you test our actual raw material?
- Who is responsible for tooling design?
- What parts are manufactured in-house?
- Which electrical and hydraulic brands are used?
- What is included in installation?
- Is operator training included?
- How quickly are technical questions answered?
- Which spare parts should be purchased with the line?
- How long are PLC programs and drawings retained?
- Can replacement rollers be manufactured later?
- What warranty exclusions apply?
For broader equipment evaluation criteria, refer to the roll forming machine buying guide.
11. Compare Total Cost Instead of Purchase Price
The lowest-priced photovoltaic solar bracket machine is not always the lowest-cost option over its operating life.
Total cost may include:
- Machine purchase
- Tooling
- Additional dies
- Freight
- Installation
- Foundation work
- Operator training
- Spare parts
- Electricity
- Labor
- Maintenance
- Tooling replacement
- Unplanned downtime
- Scrap material
- Product rework
- Changeover losses
| Low Initial Price May Hide | Higher-Value Configuration May Provide |
|---|---|
| Limited tooling life | Longer tooling service life |
| Slow manual adjustment | Faster repeatable changeover |
| Basic punching control | Servo-controlled hole positioning |
| Limited documentation | Complete manuals and drawings |
| No remote diagnostics | Faster technical troubleshooting |
| Lower structural strength | Stable long-term production |
| Few included spare parts | Planned spare-parts package |
| Unclear acceptance criteria | Documented FAT standards |
Calculate the value of stable output, reduced scrap, shorter changeovers, and faster after-sales support before making the final decision.
12. Information to Include in Your RFQ
A complete request for quotation should include:
Product Information
- Profile drawings
- Product photographs
- Bracket application
- Length range
- Hole pattern
- Required tolerances
Material Information
- Material grade
- Yield strength
- Thickness range
- Coil width
- Coil weight
- Coating type
- Surface protection requirements
Production Information
- Pieces per shift
- Tons per month
- Number of shifts
- Expected product mix
- Changeover frequency
- Required automation level
Factory Information
- Available floor space
- Local voltage and frequency
- Compressed air supply
- Coil-handling method
- Crane and forklift capacity
- Local safety requirements
Commercial Information
- Delivery destination
- Required delivery date
- Installation expectations
- Training requirements
- Spare-parts package
- Warranty requirements
- Preferred payment terms
This information helps the supplier provide a technically accurate photovoltaic solar bracket machine proposal rather than a generic quotation.
Conclusion
Purchasing a photovoltaic solar bracket machine requires a complete evaluation of the finished profile, raw material, punching system, roll tooling, automation, production capacity, factory layout, acceptance testing, and supplier support.
The most reliable decision is not based on one headline specification. It is based on whether the complete production line can repeatedly manufacture qualified brackets under real factory conditions.
Before confirming an order, prepare accurate drawings, define measurable acceptance standards, test actual material, and compare total operating value.
For help evaluating C-channel, U-channel, punching, and automated solar bracket production configurations, contact the Jinbolida engineering team with your drawings, material specifications, and required production capacity.
Photovoltaic Solar Bracket Machine FAQ
What is the best machine for making solar mounting brackets?
The best machine depends on the profile drawing, material strength, thickness, hole pattern, output target, and product variety. A dedicated line may be best for stable mass production, while a flexible line is more suitable for factories handling many project specifications.
Can one machine produce both C- and U-channel solar brackets?
It is possible when the machine is designed with suitable adjustable or replaceable tooling. Buyers should confirm the actual changeover method, required setup time, profile limitations, and whether separate roller sets are included.
How fast should a photovoltaic solar bracket machine run?
The correct speed depends on punching frequency, material thickness, product length, cutting method, and stacking process. Instead of focusing only on maximum meters per minute, request a guaranteed number of finished pieces per shift.
Should punching be integrated with the roll forming line?
Integrated punching can reduce handling and improve hole-position consistency. Separate punching equipment may be more flexible when the factory produces many low-volume products or frequently changes hole patterns.
What material information should I send to the supplier?
Provide material grade, yield strength, tensile strength when available, thickness range, coil width, coil weight, coating specification, and sample material. Do not provide only the general term “galvanized steel.”
How can I verify machine accuracy before shipment?
Use a factory acceptance test with your real material and product drawing. Measure several finished samples for cross-section, length, hole position, surface quality, and consistency during continuous operation.
Do solar mounting brackets need to follow international standards?
Requirements vary by project and market. The machine buyer should identify the applicable material, structural, dimensional, corrosion, and installation requirements before finalizing the equipment specification. The latest IEC 62548-1 photovoltaic array design standard includes requirements relating to PV array design and mounting structures.
What should I send when requesting a machine quotation?
Send finished drawings, raw material information, target capacity, factory utilities, required automation, and sample products. This allows the supplier to evaluate tooling, punching force, roll stations, motor power, layout, and cycle time.
If you enjoyed this article on Jinbolida’s smart manufacturing and digital factory expertise, follow us for more insights and updates:
- 📘 Facebook: Stay tuned for our latest smart production line projects → Facebook
- 📱 WhatsApp: Contact us anytime for custom production solutions → Chat Now
- ▶️ YouTube: Watch our automated line demos and real-world applications → YouTube
Let’s keep innovating and shaping the future of smart manufacturing — together!
 English
 Arabic
 Russian
 Spanish
 French