
How to Choose a PV Bracket Production Line
جدول المحتويات
A photovoltaic bracket production line should not be selected by machine speed or automation level alone. The right configuration depends on what brackets you need to manufacture, the steel or aluminum specification, hole patterns, dimensional tolerances, production volume, product mix and the way material moves through your factory.
This distinction matters because photovoltaic mounting systems can use different rails, channels, posts, braces and connection components depending on the installation design. As explained in this overview of photovoltaic mounting systems, mounting structures form the mechanical support between photovoltaic modules and the roof, ground or other supporting structure.
For a bracket manufacturer, that diversity translates directly into different manufacturing requirements.
A high-volume factory producing one C-channel profile may benefit from a highly integrated line with automated punching, forming, cutting and stacking. A manufacturer supplying multiple bracket systems in smaller batches may need faster changeover and more flexible tooling instead.
The most effective way to choose equipment is therefore to work backward from the finished bracket rather than forward from a machine catalog.
ماذا يفعل خط إنتاج الأقواس الكهروضوئية؟
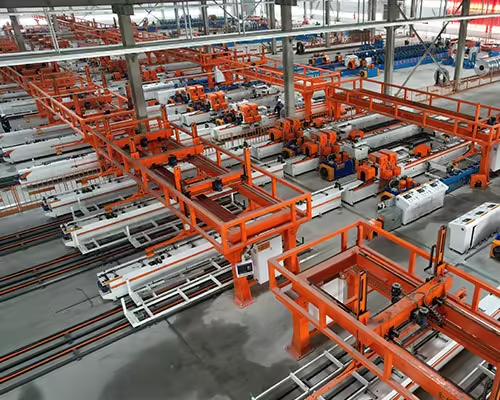
A photovoltaic bracket production line converts metal coil or prepared strip into profiles and components used in solar mounting structures.
Depending on the product, a complete line may combine:
- تحميل الملف
- إزالة التربة
- التسوية
- التغذية المؤازرة
- اللكم
- الشق
- تشكيل لفة
- Length measurement
- القطع
- تفريغ
- Turning
- التراص
- Production monitoring
جينبوليدا photovoltaic bracket production line solutions can integrate several of these processes into a coordinated manufacturing system.
For long structural profiles such as C channels and U channels, roll forming is normally the central process. Shorter connectors and plates may require different punching, cutting or forming equipment.
This is why manufacturers planning a complete solar mounting component factory should evaluate both profile-forming equipment and معدات تثقيب الرف الكهروضوئي rather than treating every component as if it were produced by the same machine.
ابدأ برسم الملف الشخصي النهائي
The most important document when selecting a photovoltaic bracket production line is usually the finished product drawing.
It tells the machine manufacturer far more than a general statement such as:
“We need a machine for solar brackets.”
A useful drawing should define parameters such as:
| معلومات المنتج | لماذا يهم |
|---|---|
| شكل الملف الشخصي | Determines roll tooling and forming sequence |
| Profile width and height | Determines machine geometry |
| سمك المادة | Influences forming force and tooling |
| أبعاد الحفرة | Determines punching tools |
| تباعد الثقب | Affects feeding and positioning |
| Slot pattern | Influences punching configuration |
| طول | Affects cutting and downstream handling |
| التسامح الأبعاد | Influences line control requirements |
| Straightness requirement | Affects forming and correction |
| حالة السطح | Influences roller and handling design |
A manufacturer supplying only one profile should send that drawing.
A manufacturer producing ten or twenty specifications should prepare a complete product matrix before machine configuration begins.
This makes it possible to determine whether those products can realistically share one forming line or whether they should be divided between dedicated and flexible equipment.
حدد المادة قبل اختيار الجهاز
Two brackets with similar dimensions can behave differently during forming if their materials have different mechanical properties.
تتضمن المعلومات المادية المهمة ما يلي:
- درجة الصلب
- قوة العائد
- قوة الشد
- نطاق السماكة
- عرض الشريط
- وزن الملف
- القطر الداخلي للملف
- القطر الخارجي للملف
- Galvanized or other coating
- Surface protection requirements
Material formability is especially important in cold forming.
The International Organization for Standardization maintains standards covering steel used for cold forming. For example, ISO 13887 covers cold-reduced steel sheet of higher yield strength with improved formability, while ISO 20805 addresses certain hot-rolled steel sheet in coils intended for cold forming.
These standards do not mean every solar bracket must use those particular grades. They illustrate an important engineering principle: material strength and formability must be considered together when designing a forming process.
Higher-strength material may require different forming radii, station design, drive capacity and springback compensation compared with softer material.
Therefore, the RFQ should specify the actual material rather than simply writing “galvanized steel.”
حدد ملفات تعريف الأقواس التي تحتاج إلى إنتاجها
Solar mounting structures can contain a wide range of profiles and connectors.
Common examples include:
- C-channel brackets
- يدعم قناة U
- Strut channels
- ملفات تعريف Z
- قضبان التثبيت
- Ground-mount posts
- بورلينز
- أعضاء تستعد
- لوحات موصل
- المشابك
- لوحات القاعدة
- Tracker components
جينبوليدا solar photovoltaic bracket forming machine range covers equipment for multiple photovoltaic profile applications.
The correct machine architecture depends on how similar those profiles are.
Profiles with similar dimensions may sometimes share tooling or use adjustable roll stations. Products with substantially different geometry may require tooling replacement or separate forming machines.
This creates one of the most important purchasing decisions in a PV bracket factory:
Should you optimize for maximum output or maximum flexibility?
الخط المخصص مقابل الخط المرن متعدد الملفات
There is no universally better option.
A dedicated line is typically optimized around a limited range of products, while a flexible line sacrifices some simplicity in exchange for the ability to process more specifications.
| Production Situation | More Suitable Direction |
| One profile, very high volume | Dedicated production line |
| Several similar C/U profiles | Adjustable or interchangeable solution |
| Frequent small batches | Flexible production configuration |
| Long campaigns with few changes | High-output dedicated line |
| Contract manufacturing | Flexible multi-profile capability |
| Rapidly changing product portfolio | Future-expandable tooling strategy |
A common purchasing mistake is asking:
“How many profiles can this machine produce?”
A better question is:
“How long does a complete changeover take between the profiles we actually sell?”
Those two questions are not equivalent.
A line may technically produce many sizes, but if tooling changes and recalibration take several hours, it may not suit a factory processing frequent small batches.
تقييم التثقيب قبل تشكيل اللفة
Hole processing is one of the most important parts of photovoltaic bracket manufacturing.
Solar brackets may contain:
- ثقوب مستديرة
- Slotted holes
- Elongated mounting slots
- Repeated hole patterns
- Connection holes
- الشقوق
- End features
The number, shape and spacing of these features influence punching equipment selection.
Before choosing a line, determine:
- How many hole patterns are required?
- Are the patterns fixed or variable?
- Does every product use the same punching sequence?
- How frequently will product specifications change?
- What positional tolerance is required?
- Is high-speed repetitive punching required?
- Should punching be integrated into the forming line?
Jinbolida provides dedicated معدات تثقيب الرفوف الشمسية الكهروضوئية as well as systems in which punching can be coordinated with feeding, forming and cutting.
The correct decision should follow the product mix rather than assuming integrated punching is always superior.
اللكم المسبق أم اللكم اللاحق؟
The punching position within the manufacturing sequence can affect both equipment layout and dimensional control.
اللكم المسبق
In a pre-punching arrangement, holes and slots are produced while the material is still flat or before the profile is fully formed.
Potential advantages include:
- Easier access to the material
- Simpler punching tooling in some applications
- Efficient repetitive hole processing
- Easier integration with servo feeding
However, the designer must understand how the subsequent forming process influences the final location of those features.
بعد اللكم
Post-punching processes features after part or all of the profile has been formed.
This may be useful where the finished geometry provides a more appropriate dimensional reference, but tooling access can become more complicated.
There is no single correct answer for every bracket.
Hole pattern, profile geometry, accuracy requirement, speed and tooling cost should all be evaluated before selecting the sequence.
لا تحدد الخط بأقصى سرعة بمفردك
Machine speed is one of the most frequently misunderstood specifications in equipment purchasing.
Suppose a forming machine is rated at 40 m/min.
That does not automatically mean the factory will continuously produce saleable brackets at 40 m/min.
Actual output can also be limited by:
- دورة اللكم
- التسارع والتباطؤ
- طريقة القطع
- طول المنتج
- Tooling change
- Coil change
- تحميل المواد
- Operator intervention
- التراص
- التعبئة والتغليف
- فحص الجودة
- صيانة
- Downstream bottlenecks
For this reason, the more useful metric is often finished parts per hour or finished meters per shift under the actual production recipe.
Jinbolida’s existing guide to PV bracket factory workflow discusses how receiving, coil preparation, punching, forming, inspection and downstream handling need to work as a connected process.
A fast roll former surrounded by slow material handling can still create a low-output factory.
حساب السعة المطلوبة من الطلب الحقيقي
Before requesting equipment speed, calculate your required output.
A simplified production estimate can start with:
Annual demand ÷ working days ÷ shifts ÷ effective production hours
For example, imagine a factory needs to produce:
- 6,000,000 meters per year
- 300 production days
- 2 shifts per day
- 8 hours per shift
The theoretical average requirement is:
6,000,000 ÷ 300 ÷ 2 ÷ 8 = 1,250 meters per hour
But this calculation assumes 100% utilization.
Real factories experience downtime from:
- استبدال الملف
- Tool changes
- تنظيف
- صيانة
- فحص الجودة
- Material shortages
- Production scheduling
- تغيير المنتج
Therefore, capacity planning needs a realistic utilization allowance rather than simply matching theoretical annual demand to rated machine speed.
مطابقة نظام القطع للمنتج
Cutting is another area where buyers often focus on the forming machine but overlook the effect of the downstream process.
The cutting method influences:
- Cycle time
- دقة الطول
- حالة القطع
- ضجيج
- Tool maintenance
- Line continuity
Depending on the application, a system may use hydraulic cutting, tracking cutting, saw cutting or other configurations.
For high-throughput production, cutting should be coordinated with line speed so it does not repeatedly force the forming process to stop.
For lower-volume or frequently changing products, a simpler system may sometimes be economically more appropriate.
The correct selection depends on the required production cycle and cut quality rather than the name of the cutting technology alone.
Consider Surface Protection for Galvanized Profiles
Many photovoltaic mounting profiles use coated steel because the final bracket is expected to operate outdoors.
That creates an additional manufacturing requirement: forming and handling should minimize unnecessary surface damage.
وتشمل الاعتبارات الهامة ما يلي:
- Roller surface condition
- Tooling cleanliness
- محاذاة الدليل
- Contact pressure
- Burrs
- Material dragging
- Metal chips
- Stacking method
- Transport between processes
A machine can produce dimensionally correct profiles while still creating commercial problems if the surface is heavily scratched during forming or unloading.
Surface requirements should therefore be included in the project specification from the beginning.
Think Beyond the Roll Former
An efficient photovoltaic bracket production line is more than a roll forming machine.
A complete manufacturing system may require coordinated equipment before and after forming.
A typical flow could be:
Coil Storage → Decoiling → Leveling → Feeding → Punching → Roll Forming → Cutting → Unloading → Stacking → Inspection → Packaging
The exact configuration should depend on the product.
Jinbolida’s guide to تخطيط خط آلة تشكيل قوس الدعم الشمسي explains why equipment position, coil-loading space, maintenance access, punching capacity and downstream handling should be planned together.
This becomes increasingly important as automation rises.
Automating one process while leaving the next process manual can simply move the bottleneck further downstream.
Choose the Right Automation Level
More automation does not automatically mean a better investment.
The right level depends on:
- Labor availability
- تكلفة العمالة
- حجم المنتج
- Number of SKUs
- حجم الدفعة
- Required traceability
- Factory management system
- تردد التحول
- Product handling requirements
- Investment budget
Consider three simplified scenarios.
Scenario 1: High-Volume Standard Product
The factory manufactures a small number of bracket profiles continuously.
A more integrated line can be attractive because repetitive handling and operator intervention can be reduced.
Scenario 2: Many Small-Batch Products
The manufacturer serves multiple customers and changes specifications frequently.
Fast adjustment and flexible tooling may create more value than maximum automation.
Scenario 3: Rapid Capacity Expansion
The manufacturer already has equipment but needs substantially higher output.
The correct solution may not be replacing every machine.
Instead, the bottleneck should first be identified. Punching, forming, coil handling or stacking may be restricting capacity.
This is why factory-level analysis is often more useful than comparing machines individually.
Evaluate Factory Layout Before Ordering
Equipment dimensions alone are not enough for layout planning.
Allow space for:
- Coil delivery
- Crane or forklift access
- تحميل الملف
- Tooling storage
- خزائن كهربائية
- Operator movement
- صيانة
- Finished profile discharge
- فحص
- التراص
- التعبئة والتغليف
- Emergency access
- Future expansion
Long photovoltaic profiles also need sufficient discharge length.
A line that physically fits between two walls may still be impractical if there is no room to replace tooling or remove finished material.
The factory drawing should therefore be shared with the equipment supplier before final configuration.
Understand Accuracy as a Complete System
Customers commonly ask for “high precision,” but precision needs to be translated into measurable requirements.
Relevant dimensions may include:
- Profile width
- Profile height
- Flange dimension
- قطر الثقب
- موقف الحفرة
- طول الفتحة
- تحمل الطول
- الاستقامة
- تطور
- Cross-sectional angle
Each of these can be affected by different processes.
For example, a hole-position issue may originate from feeding or punching rather than roll forming.
A length problem may relate to measurement or cutting.
Profile twist may relate to tooling, material variation or forming balance.
The equipment specification should therefore define which dimensions matter and how they will be inspected.
Consider Material Variation, Not Only Nominal Thickness
A drawing may specify material thickness of 2.0 mm, but real coil material always has permitted manufacturing variation.
The same applies to mechanical properties.
This is one reason the production line should be engineered for a realistic material range rather than one perfect theoretical value.
ISO’s Steel Technical Committee covers standardization relating to cast, wrought and cold-formed steel, illustrating how material specifications and delivery conditions form an important part of industrial processing.
For equipment projects, buyers should provide the applicable material standard or actual mill certificate whenever possible.
That gives the equipment engineer more useful information than a generic steel description.
Plan Changeover Before You Need It
Photovoltaic mounting products can change as customer projects, structural designs and market requirements evolve.
Therefore, manufacturers should consider future products before finalizing machine tooling.
يسأل:
- Can width be adjusted?
- Can forming stations be repositioned?
- How is tooling replaced?
- How long does replacement take?
- Which parts are product-specific?
- Are recipes stored in the control system?
- What requires manual adjustment?
- Could future tooling be added?
If your production includes C-channel and U-channel variants, reviewing Jinbolida’s solar photovoltaic bracket forming machine solutions can help illustrate the range of profile-processing equipment that may be involved.
The objective is not to buy an unnecessarily complicated machine.
It is to avoid discovering after installation that every new profile requires major equipment modification.
Evaluate Total Production Cost, Not Only Machine Price
The lowest quotation does not always create the lowest manufacturing cost.
A production-line investment should consider:
- Initial equipment price
- الأدوات
- تثبيت
- Shipping
- متطلبات المشغل
- استهلاك الطاقة
- صيانة
- Spare parts
- Changeover downtime
- Scrap
- Tool life
- Product quality
- الإنتاجية
- Future expansion
Imagine two lines.
Line A costs less but requires two additional operators and 90 minutes of product changeover.
Line B costs more but requires fewer operators and changes products in 20 minutes.
Which is cheaper?
The answer depends on your actual production schedule.
A manufacturer producing one profile for several weeks may gain little from rapid changeover.
A contract manufacturer changing products three times per shift could obtain significant value from it.
The correct economic comparison therefore needs to reflect the production model.
Common Mistakes When Buying a PV Bracket Production Line
Choosing by Price Before Defining the Product
Different machine quotations may represent completely different technical configurations.
The finished profile and production requirement should be defined first.
Asking Only for Maximum Speed
Rated speed is not the same as effective factory output.
Evaluate the complete manufacturing cycle.
Ignoring Punching Capacity
A fast roll forming machine cannot compensate for a punching process that cannot keep pace.
Underestimating Changeover
Flexibility should be measured in actual changeover steps and time.
Ignoring Downstream Handling
Manual unloading and stacking can become a bottleneck when upstream equipment is automated.
توفير معلومات مادية غير كاملة
Material grade and mechanical properties can influence forming behavior.
Designing the Machine Before the Factory Layout
Machine access, coil loading and product discharge must be considered before equipment is finalized.
Buying Automation Without a Production Reason
Automation should solve a measurable labor, quality, throughput or traceability requirement.
Information to Prepare Before Requesting a Quote
A professional RFQ should contain enough information for the supplier to design the line around the real product.
Prepare the following:
| Category | معلومات لتقديمها |
| ملف تعريف | 2D/3D drawings |
| مادة | Grade and standard |
| سمك | الحد الأدنى والحد الأقصى |
| لفائف | Width, ID, OD and weight |
| نمط الثقب | Drawing and tolerance |
| طول المنتج | الحد الأدنى والحد الأقصى |
| الناتج | Pieces/hour or meters/year |
| مزيج المنتج | SKUs and batch quantities |
| التحول | Required frequency |
| سطح | Coating and finish |
| الأتمتة | Desired level |
| مصنع | Layout and available area |
| المرافق | Voltage, frequency and air |
| جودة | Critical tolerances |
| توسع | Expected future products |
The more complete this information is, the easier it becomes to compare equipment proposals on an equal basis.
How to Compare Two Production Line Proposals
When two suppliers submit quotations, do not compare only the final price.
Use a technical comparison table.
| Evaluation Area | Questions to Ask |
| تشكيل | How many forming stations and why? |
| الأدوات | What material and treatment are used? |
| اللكم | What cycle and positioning method are used? |
| القطع | Does cutting interrupt production? |
| سرعة | Is it forming speed or effective output? |
| التحول | What steps and time are required? |
| يتحكم | Which parameters are recipe-controlled? |
| التعامل | Is unloading automatic or manual? |
| دقة | Which tolerances are guaranteed? |
| تثبيت | What commissioning support is included? |
| Spare parts | What critical parts are recommended? |
| توسع | Can future profiles be added? |
This converts the buying process from a price comparison into an engineering comparison.
When Does a Fully Integrated Line Make Sense?
A highly integrated line becomes particularly attractive when:
- Product demand is stable
- Production volume is high
- Processes are repetitive
- Labor reduction is important
- Material transfer creates bottlenecks
- Product traceability is required
- Finished profiles can be automatically handled
In these conditions, integrating loading, forming, cutting and stacking can reduce unnecessary work between separate machines.
جينبوليدا photovoltaic support equipment guide provides additional discussion of when integrated equipment makes sense and when separate machines may provide greater flexibility.
When Are Separate Machines Better?
Separate machines can still be appropriate.
They may make sense when:
- Production volume is moderate
- Product variety is very high
- Different processes serve multiple product families
- The manufacturer already owns usable equipment
- Capital investment needs to be phased
- Batch production changes frequently
The key principle is simple:
Integration should remove a real production bottleneck, not merely make a production line look more advanced.
A Practical Selection Process
A reliable photovoltaic bracket production line selection process can be summarized in nine steps:
- Collect all finished bracket drawings.
- Group similar and different profile families.
- Define the actual material specification.
- Map all punching, forming and cutting operations.
- Calculate required annual and hourly output.
- Determine acceptable changeover time.
- Define the appropriate automation level.
- Check factory layout and material flow.
- Compare suppliers using measurable technical criteria.
Following this order dramatically reduces the risk of selecting equipment before the manufacturing problem has been properly defined.
الأسئلة المتداولة
What machines are needed to manufacture photovoltaic brackets?
The exact equipment depends on the bracket design. A production system may include a decoiler, leveler, feeder, punching machine, roll forming machine, cutting unit, unloading system and stacking equipment. Connector components may require additional punching or forming equipment.
Can one roll forming machine produce different solar bracket sizes?
Yes, some machines can produce multiple sizes through adjustable or interchangeable tooling. However, the number of possible profiles does not alone determine flexibility. Buyers should also evaluate the actual changeover procedure and time.
What information is needed to quote a PV bracket production line?
The most important information includes profile drawings, material grade, thickness, coil dimensions, hole patterns, product lengths, required output, production mix and desired automation level.
Should punching be integrated with the roll forming machine?
It can be, but integration is not always the best solution. The decision depends on hole patterns, production volume, cycle time, product variety and factory workflow.
What determines the speed of a solar bracket production line?
Effective speed can be limited by feeding, punching, roll forming, cutting, coil replacement, changeover, unloading and stacking. The slowest process in the production sequence often determines actual output.
Is a fully automatic PV bracket line always better?
No. High automation is especially valuable for repetitive, high-volume production. Smaller batches and frequent specification changes may benefit more from flexible equipment.
Why is the material grade important for roll forming?
Different yield strength, tensile strength and formability can change springback and forming behavior. These differences can affect tooling design, forming sequence and machine requirements.
How should I compare two PV bracket machine quotations?
Compare the complete technical scope: forming stations, tooling, punching, cutting, effective production speed, changeover, automation, accuracy, downstream handling, service and future expansion—not only the purchase price.
خاتمة
Choosing a photovoltaic bracket production line starts with the finished product, not the machine.
Profile geometry, steel properties, hole patterns, production volume, changeover frequency, automation requirements and factory layout all influence the correct configuration. A line designed for a high-volume C-channel manufacturer may be completely different from equipment designed for a contract manufacturer producing many solar bracket specifications.
The most useful purchasing process is therefore to define products and production targets first, identify the processes required to manufacture them, and then determine how those processes should be connected.
Manufacturers planning new photovoltaic bracket capacity can review Jinbolida’s آلات تشكيل الأقواس الشمسية الكهروضوئية, معدات تثقيب الرف الكهروضوئي and existing PV bracket factory workflow guide for additional production-line planning information.
For a customized production line proposal, prepare your profile drawing, material specification, hole pattern, required capacity and available factory layout, then اتصل بجينبوليدا to discuss a configuration based on your actual manufacturing requirements.
 Arabic
 English
 Russian
 Spanish
 French