
Formage de rouleaux d'acier galvanisé : facteurs clés du processus
Table des matières
Introduction
Galvanized steel is widely used for roll formed components that require a combination of structural performance, efficient continuous production, and corrosion protection. Construction profiles, photovoltaic mounting channels, roofing components, brackets, framing members, and other outdoor metal products are frequently manufactured from zinc-coated steel coil.
However, galvanized steel roll forming involves more than processing ordinary carbon steel with a zinc layer on the surface. The coating changes how manufacturers need to think about material handling, roller contact, bend severity, surface protection, tooling cleanliness, lubrication, punching, cutting, and finished-profile inspection.
A roll forming line may successfully produce the required cross-section while still damaging the galvanized surface through excessive pressure, worn tooling, trapped metal particles, poor guides, or inappropriate handling. Conversely, focusing only on protecting the coating without controlling material properties and springback can result in dimensional inconsistency.
The most effective production strategy therefore considers the steel substrate and zinc coating as one material system. Tooling, machine setup, feeding, forming, punching, cutting, and handling should all be developed around the actual galvanized coil specification and finished-profile requirements.
What Is Galvanized Steel Roll Forming?

Galvanized steel roll forming is the continuous cold-forming process used to transform zinc-coated steel strip into a specified cross-section through a series of roller stations.
The basic process is similar to other roll forming operations:
coil loading → decoiling → leveling → guiding → punching where required → progressive roll forming → straightening → cutting → handling
What makes galvanized material different is the presence of the zinc-based protective coating.
This coating helps protect the underlying steel from corrosion, but it also becomes one of the surfaces directly contacting:
- decoiler components,
- leveler rolls,
- feeder rolls,
- guides,
- outillage de poinçonnage,
- former des rouleaux,
- équipement de coupure,
- convoyeurs,
- and stacking systems.
Surface protection therefore needs to be considered across the whole line rather than only inside the roll forming machine.
JBLDIE guide-machine de formage de rouleaux includes galvanized steel among the common materials used for continuous profile production and emphasizes the importance of controlling roller and guide contact when coated material is processed.
Why Is Galvanized Steel Commonly Roll Formed?
Roll forming is particularly suitable for producing long profiles with a constant cross-section.
Galvanized steel complements this process because the material already carries a protective zinc coating before it enters the production line.
Depending on the product design, manufacturers can therefore produce:
- canaux structurels,
- C and U profiles,
- Profils Z,
- solar mounting channels,
- sections de toiture,
- framing components,
- reinforcement profiles,
- support brackets,
- and other continuous sections
without requiring the entire profile to receive the same type of post-forming coating process.
This can be useful for high-volume production where long sections and repeated geometries are required.
However, processing pre-galvanized steel places more responsibility on the forming line because unnecessary coating damage created during production can reduce the quality of the finished part.
Galvanized Steel Is Not One Universal Material
One of the first mistakes in galvanized steel roll forming is treating every galvanized coil as if it behaves identically.
The steel substrate can vary in:
- épaisseur,
- grade,
- limite d'élasticité,
- résistance à la traction,
- elongation,
- hardness,
- et contrainte résiduelle.
The coating can also differ in:
- coating type,
- coating mass or thickness,
- finition de surface,
- spangle condition,
- lubrification,
- and other specification details.
These variables influence both forming behavior and surface condition.
A tooling setup developed using one galvanized steel specification may not automatically behave identically when a different grade or thickness is introduced.
For this reason, manufacturers should provide the actual material specification during roll forming line and tooling development rather than simply stating “galvanized steel.”
Material Thickness Affects Roll Gap
The thickness of the galvanized strip influences how it fits between the upper and lower forming rolls.
Roll tooling is normally developed around a defined material-thickness range.
If the material becomes significantly thicker than expected, tooling contact changes. The profile may experience greater forming force, different bend geometry, or excessive roller pressure.
If the strip is thinner, the tooling may provide less control than intended.
Normal thickness variation can also contribute to finished dimensional changes.
Before production begins, operators should therefore verify that the incoming coil falls within the material range for which the tooling has been developed.
Roll gap should then be set according to the tooling procedure rather than tightened simply to force the profile toward its nominal dimensions.
Yield Strength Influences Springback
Galvanized steel still follows the mechanical behavior of its steel substrate during bending.
After the strip passes through a forming roll, part of the imposed deformation can recover elastically. This is known as springback.
A material with higher yield strength may respond differently from a softer steel even when both materials have the same thickness and zinc coating.
Springback can influence:
- angle de courbure,
- position de la bride,
- largeur hors tout,
- hauteur de section,
- and final corner geometry.
Tooling design may compensate through controlled over-forming or calibration.
However, these corrections should be based on the material range rather than treated as fixed values for every galvanized coil.
If profile dimensions change after switching steel grades, material behavior should be checked before operators begin making major tooling adjustments.
The Zinc Coating Changes Surface-Contact Requirements
With uncoated steel, a small roller scratch may mainly be a surface-quality issue.
With galvanized steel, excessive scratching can also remove or disturb part of the protective coating.
This makes tooling surface condition especially important.
Forming rolls should be checked for:
- rough areas,
- bavures,
- rayures,
- rouille,
- embedded particles,
- damaged edges,
- and coating buildup.
Guides and feeder rolls should receive similar attention.
A small piece of trapped metal can repeatedly mark every meter of strip passing through the machine.
Because roll forming is continuous, one contaminated roller can produce a long sequence of identical surface defects before the problem is discovered.
Avoid Excessive Roll Pressure
A common response to dimensional problems is to tighten the roll stands.
With galvanized material, excessive pressure can create additional risks.
Too much pressure may:
- mark the zinc coating,
- increase friction,
- create local surface polishing,
- accelerate tooling wear,
- change material flow,
- or introduce unnecessary forming stress.
Roll forming should guide the strip progressively into shape rather than rely on excessive compression.
If a profile is outside the required dimension, operators should first determine whether the cause is:
- variation matérielle,
- strip alignment,
- tooling position,
- incorrect roll gap,
- retour élastique,
- usure d'outillage,
- or another process variable.
Simply increasing pressure can hide the original issue while creating a new surface problem.
Bend Radius Matters
Every roll formed profile contains a relationship between material thickness, bend radius, angle, and steel properties.
Very severe bending can place greater strain on both the steel and its coating.
This becomes more relevant where a profile requires tight corners.
The tooling designer should therefore avoid treating the smallest possible bend radius as automatically desirable.
The American Galvanizers Association notes in its guidance on bending galvanized steel that bend severity and bend speed can affect coating integrity when galvanized steel is formed after coating.
Roll formed coil products and batch hot-dip galvanized fabricated parts are not identical manufacturing systems, but the underlying principle remains useful: coating condition should be considered when defining severe bends and forming procedures.
The finished bend requirement should therefore reflect the actual material specification and product function.
Progressive Forming Helps Control Material Strain
Roll forming creates the profile through several forming stations rather than bending the strip completely in one operation.
This progressive approach is particularly valuable for galvanized steel.
Instead of forcing a 90-degree bend immediately, tooling can develop the bend through several intermediate angles.
A simplified progression might be:
flat → slight bend → intermediate bend → near-final bend → calibration
The actual progression depends on profile geometry.
Gradual forming helps distribute strain and gives the tooling more control over the way the coated strip moves.
Aggressive deformation in too few passes can increase:
- onde de bord,
- twist,
- contact de surface,
- coating stress,
- et variation dimensionnelle.
The correct number of forming stands therefore needs to match the actual section rather than simply minimize machine length.
Flower Pattern Design Affects Coating Contact
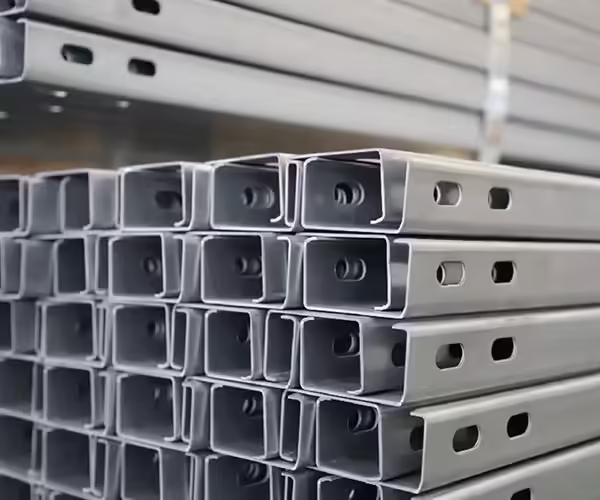
The flower pattern shows how the profile develops through each forming pass.
For galvanized steel, the designer should consider not only geometry but also where the strip contacts the rolls during each stage.
If tooling causes unnecessary sliding between the material and roller surfaces, coating wear can increase.
Good tooling attempts to guide the strip through the intended deformation path while minimizing uncontrolled rubbing.
This becomes especially important for:
- canaux profonds,
- retourne les lèvres,
- narrow internal bends,
- asymmetric profiles,
- and profiles with several nearby bends.
The most efficient forming path is not always the path with the fewest stands.
A stable progression that protects both dimensions and surface condition is generally more valuable.
Tooling Surface Finish Is Important
Roll surfaces that contact galvanized steel should be manufactured and maintained to an appropriate finish.
Surface defects on tooling can be transferred directly to the strip.
For appearance-sensitive profiles, even shallow marks may become unacceptable.
The required tooling material and surface treatment depend on:
- production volume,
- qualité de l'acier,
- épaisseur de la bande,
- revêtement,
- profile geometry,
- and machine design.
Whatever tooling specification is used, condition should be monitored throughout production.
A roller that was suitable when new can become a source of coating damage after wear or accidental contact.
Tool maintenance therefore forms part of galvanized steel quality control.
Tooling Cleanliness Should Be Checked Frequently
Galvanized steel production can generate or carry contaminants into the forming section.
Potential sources include:
- slitting burrs,
- metal particles,
- dirt,
- oil contamination,
- particles from punching,
- and debris generated by worn tools.
These particles can become trapped between the strip and roller.
The result may be a continuous scratch or repeating indentation.
Operators should clean forming rolls according to established maintenance procedures and inspect material-contact surfaces when a new mark appears.
The pattern of the defect can also provide diagnostic information.
If a mark repeats at regular intervals, its spacing may correspond with the circumference of a particular roller.
This can help maintenance teams identify the source more quickly.
Entry Guides Must Protect the Edges
Entry guides keep the strip aligned with the roll forming centerline.
They should control the strip without applying unnecessary side pressure.
If a guide rubs aggressively against a galvanized edge, it can damage the coating or create excessive friction.
Poor guide positioning can also force the strip laterally.
That can lead to:
- unequal flange dimensions,
- camber,
- twist,
- edge marking,
- and unstable tracking.
The guide should therefore establish material position rather than force an incorrectly aligned coil through the machine.
If strong guide pressure is required to keep the strip centered, the upstream material path should be investigated.
Decoiling Must Maintain Stable Strip Position
Surface protection begins before the first forming roll.
The coil should be loaded and centered correctly on the decoiler.
If the coil is substantially offset from the line center, the strip may travel laterally while entering the leveler or feeder.
This creates unnecessary guide contact.
The decoiler should also control material release according to the line design.
Unstable coil movement can introduce:
- sudden tension,
- mouvement latéral,
- loop instability,
- or surface contact.
The relationship between decoiler, leveler, feeder, and forming machine should therefore be checked as one continuous strip path.
Leveling Galvanized Steel
Coiled material may carry curvature or coil set that needs to be reduced before punching or roll forming.
A leveler uses a sequence of rollers to bend the strip alternately and improve flatness.
For galvanized material, leveling rolls should remain clean and correctly adjusted.
Excessive leveling pressure can mark the surface or introduce unwanted deformation.
Insufficient leveling can leave the strip unstable for downstream operations.
The correct setting depends on:
- épaisseur,
- steel strength,
- état de la bobine,
- largeur de bande,
- and line configuration.
When changing to a different material specification, leveling conditions may need to be verified rather than assuming one setting works for every coil.
Servo Feeding and Galvanized Surface Protection
Many automated lines use servo feeders before punching or cutting.
Feed rollers need enough pressure to move the strip without slipping.
However, excessive grip can mark coated surfaces.
This creates a balance between positioning stability and surface protection.
Operators should monitor:
- pression d'alimentation,
- roller cleanliness,
- glissement matériel,
- roller surface condition,
- accélération,
- and upstream strip tension.
A feeder that struggles to move the strip should not automatically be tightened.
The cause may be excessive resistance from the decoiler or leveler.
Stable feeding requires the complete upstream system to work together.
Punching Galvanized Steel Before Roll Forming
Many galvanized roll formed profiles contain holes or slots.
Solar mounting channels, construction profiles, and support components are common examples.
Punching is often performed while the strip is still flat because tooling access is easier.
However, the punching operation can influence both surface condition and later forming.
Important controls include:
- punch and die clearance,
- tool sharpness,
- position du trou,
- état de bavure,
- strip support,
- and lubrication where required.
Excessive burr near a future bend can interfere with tooling contact.
Loose metal particles generated during punching can also travel toward the roll forming section and create surface scratches.
The punching area should therefore include appropriate debris management and inspection.
Keep Punched Features Away From Critical Bends When Possible
When a hole or slot is positioned very close to a bend, the surrounding material can deform during roll forming.
The hole may:
- stretch,
- change shape,
- shift relative to the finished profile,
- or influence the local bend.
This is not unique to galvanized steel, but coated material adds another concern because deformation around the feature can affect the local surface.
Profile design and manufacturing sequence should therefore be reviewed together.
When hole locations are functionally fixed, the tooling design should account for their position during the forming progression.
Final inspection should measure hole location on the finished profile rather than only on the flat punched strip.
Cutting Creates Exposed Steel at the Edge
When galvanized strip is cut, the cut edge exposes the steel substrate locally because the original zinc coating does not cover the newly created surface in the same way as the broad coated faces.
This can occur at:
- punched holes,
- emplacements,
- notches,
- sheared edges,
- and final cut ends.
Whether additional protection is required depends on the material system, finished product, environment, applicable standard, and customer specification.
Manufacturers should therefore avoid assuming that the presence of galvanized coating eliminates every post-processing consideration.
Cutting quality should also remain controlled.
Large burrs or distorted ends can interfere with assembly and handling regardless of coating condition.
Cut-Off Tooling Should Avoid Crushing the Profile
A profile may leave the forming stands with an acceptable galvanized surface but become damaged during final cutting.
Complex sections require cutting tooling that supports the profile geometry appropriately.
If the cut-off system crushes or rubs the section excessively, it can create:
- coating marks,
- déformation locale,
- bavures,
- fin de la fusée éclairante,
- or dimensional changes.
Cutting should therefore be evaluated as part of the finished-profile process rather than as a separate machine function.
Both the cross-section and surface should be checked after the final cut.
Key Factors in Galvanized Steel Roll Forming
| Facteur de processus | Pourquoi c'est important | What to Monitor |
|---|---|---|
| Épaisseur du matériau | Influences roll gap and dimensions | Coil specification |
| Steel strength | Influences springback | Grade and mechanical properties |
| État de revêtement | Affects finished surface | Scratches, flaking, abrasion |
| Bend severity | Influences local coating strain | Bend radius and progression |
| Roll surface | Contacts coating continuously | Wear, roughness and debris |
| Écart de rouleau | Controls material contact | Pressure and profile geometry |
| Guides d'entrée | Establish strip position | Alignment and edge rubbing |
| Nivellement | Prepares strip for processing | Flatness and surface marks |
| Servo-alimentation | Controls longitudinal position | Slip and roller pressure |
| Perforation | Creates holes and debris | Burrs and final feature position |
| Coupe | Produces finished length | Burrs, crushing and end condition |
| Manipulation | Protects finished profile | Sliding, impact and stacking |
Common Galvanized Roll Forming Surface Problems
Long Continuous Scratches
A continuous scratch usually suggests prolonged contact with one stationary source.
Les causes possibles comprennent :
- damaged entry guide,
- rough side guide,
- debris trapped at a fixed contact point,
- or another component rubbing continuously against the strip.
The location of the scratch across the profile width can help identify the corresponding machine position.
Repeating Roller Marks
Marks occurring at regular intervals may be associated with a rotating roll.
Inspect the corresponding roller circumference for:
- embedded particles,
- bosses,
- rough areas,
- ou des dommages de surface.
Polished or Shiny Contact Areas
Local polishing may indicate excessive tooling pressure or sliding.
Check roll gap and whether the strip is moving naturally through the intended forming path.
Coating Disturbance at Bends
If damage occurs mainly around severe bends, review:
- bend radius,
- spécification du matériel,
- coating condition,
- formation de progression,
- and the amount of deformation introduced per pass.
Edge Damage
Edge marks may come from slitting, entry guides, side rolls, or lateral strip movement.
The problem should be traced from the incoming coil rather than assumed to originate in the final profile.
Distinguish Coating Damage From Normal Appearance Variation
Galvanized steel can show natural appearance variation depending on coating and material specification.
Not every visible difference indicates harmful damage.
At the same time, a production line should not dismiss genuine scratches, bare areas, or repeated abrasion simply because galvanized surfaces are not always visually uniform.
Inspection requirements should be based on:
- the relevant material specification,
- customer expectations,
- product application,
- and functional coating requirements.
For products where surface appearance is especially important, acceptable reference samples can help operators distinguish normal coating variation from process-created damage.
Material Handling Matters After Forming
A well-formed profile can still be damaged after leaving the machine.
Long galvanized profiles often pass through:
- réception de tables,
- convoyeurs,
- transfer systems,
- stacking devices,
- bundling,
- and storage.
Sliding one coated profile against another can create abrasion.
Dropping profiles onto hard metal supports can also damage surfaces or edges.
Automated handling should therefore be designed to control contact.
The objective is to move the product efficiently without undoing the surface protection maintained during roll forming.
Stacking Galvanized Profiles
Finished profiles should be stacked in a stable arrangement that minimizes uncontrolled movement.
The appropriate method depends on the section geometry.
Some profiles can nest together efficiently, while others need spacers or defined orientation.
Stacking design should consider:
- profile shape,
- poids,
- longueur,
- surface sensitivity,
- bundle stability,
- lifting method,
- and storage conditions.
If profiles slide excessively during stacking, surface marks can occur even though every upstream machine operates correctly.
Finished-product quality therefore continues beyond the cut-off station.
Galvanized Steel and Outdoor Roll Formed Components
One reason galvanized steel is common in roll forming is its suitability for products exposed to outdoor or corrosive environments.
Les exemples incluent :
- photovoltaic mounting structures,
- construction framing,
- roofing components,
- infrastructure profiles,
- outdoor support channels,
- and other structural sections.
JBLDIE solutions de machines de formage process galvanized steel alongside carbon steel, stainless steel, aluminum, and other coil materials for different profile applications.
For outdoor components, coating condition becomes an important part of manufacturing quality because the surface is intended to contribute to corrosion protection during service.
The roll forming line should therefore preserve the specified material condition as much as practical throughout processing.
Galvanized Steel for Solar Mounting Profiles
Solar mounting profiles provide a good example of galvanized steel roll forming.
A photovoltaic support channel may require:
- long continuous length,
- accurate cross-section,
- créneaux répétés,
- multiple bend features,
- consistent hole positioning,
- outdoor corrosion resistance,
- and efficient production.
The manufacturing process may combine:
décoilage → nivellement → alimentation servo → poinçonnage → formage des rouleaux → découpe → déchargement
The profile must be dimensionally correct while the zinc-coated surface passes through multiple mechanical operations.
This makes coordination between punching, tooling design, roll pressure, and automated handling particularly important.
Galvanized Steel for Construction Profiles
Construction roll formed products can include:
- pannes,
- framing members,
- sections de toiture,
- wall profiles,
- channels,
- and other structural components.
These profiles may contain wide flanges or relatively thin material, making them susceptible to edge wave or surface marking if the forming progression is poorly controlled.
JBLDIE construction formant la gamme de machines is designed for coil materials including galvanized steel and other metal types used for construction profiles.
As with other applications, the machine should be configured around the actual profile drawing and material rather than a generic material category.
How to Troubleshoot Coating Damage
When surface damage appears, begin by identifying its pattern.
Demander:
- Is the defect continuous?
- Does it repeat at regular intervals?
- Is it concentrated on one edge?
- Does it appear only after a specific forming stand?
- Is it limited to a bend?
- Does it occur only after punching?
- Does it appear during handling rather than forming?
Then inspect the material upstream.
Confirm whether the coil already contained the defect before entering the machine.
Follow the strip through each processing stage.
When the first new damage appears, the likely source becomes much easier to identify.
Avoid adjusting unrelated roller stands before determining where the coating is actually being affected.
Do Not Ignore Slitting Quality
The quality of the incoming slit coil influences roll forming.
Poor strip edges can contain:
- bavure excessive,
- onde de bord,
- width variation,
- or damage.
Burrs can scratch guides and tooling or generate particles that travel into the forming section.
Width variation can also affect final flange dimensions and strip tracking.
For galvanized steel, slitting should therefore be considered part of material preparation.
If coating damage is concentrated at the profile edges, inspect the original strip before changing the roll forming machine.
Changeover Requires Surface Inspection
A production line processing several materials should include surface inspection during changeover.
After running uncoated carbon steel, tooling may contain particles or residue that could mark the next galvanized coil.
Rollers and guides should therefore be inspected and cleaned as required before introducing an appearance-sensitive or coated material.
Likewise, changing thickness may require roll-gap verification.
Changing grade may alter springback.
The production recipe should therefore include both control-system settings and physical machine conditions.
A material change should not be treated only as changing the coil.
Maintenance Is Especially Important for Coated Material
Routine maintenance helps preserve both profile accuracy and coating quality.
Important inspection areas include:
- former des rouleaux,
- rouleaux latéraux,
- guides d'entrée,
- feeder rolls,
- leveler rolls,
- outillage de poinçonnage,
- cutting tooling,
- convoyeurs,
- and stacking contact surfaces.
Damaged bearings or shaft movement can also change roller contact and increase surface pressure.
Cleaning should be part of normal maintenance.
Waiting until a visible scratch appears means a significant length of product may already have been affected.
Quality Control Should Include Both Geometry and Surface
A galvanized profile should not be approved based only on dimensions.
Inspection should consider two main categories.
Geometric Quality
Check features such as:
- largeur,
- hauteur,
- dimensions de la bride,
- angles de courbure,
- position du trou,
- rectitude,
- twist,
- et longueur finie.
Surface Qualité
Vérifier pour:
- rayures,
- repeated tool marks,
- coating disturbance,
- contamination,
- bosses,
- handling damage,
- and unacceptable edge condition.
The required acceptance criteria depend on the applicable product and material specification.
Inspection frequency should be sufficient to identify process drift before a large production batch is affected.
First-Piece Testing After a Material Change
When a different galvanized steel specification is introduced, first-piece verification becomes useful even when the same profile tooling remains installed.
Check whether the new coil changes:
- angle de courbure,
- largeur de la bride,
- retour élastique,
- suivi de bande,
- contact de surface,
- punching quality,
- or cutting behavior.
If the new material behaves differently, machine adjustments should be made systematically and recorded.
This provides a repeatable setup if the same material is used again.
Material-related settings should not depend solely on operator memory.
What Information Should Be Provided Before Configuring the Line?
Before developing equipment for galvanized steel roll forming, manufacturers should provide detailed production information.
Les informations importantes comprennent notamment
Dessins de profil
Show the complete cross-section, bends, lips, holes, slots, and critical dimensions.
Spécification matérielle
Identify the steel grade and galvanized coating specification.
Plage d'épaisseur
Provide both minimum and maximum material thickness.
Largeur de bande
Confirm the material range entering the line.
Exigences de surface
Indicate whether the finished profile is appearance-sensitive.
Punching pattern
Provide hole dimensions, spacing, and relationship with bend locations.
Longueurs terminées
Define required profile lengths and tolerance.
Gamme de production
Identify how many profile sizes will run on the machine.
Production requirements
Provide expected output and changeover frequency.
Handling requirements
Explain how finished profiles will be received, stacked, or transferred.
With this information, tooling and machine configuration can be developed around the actual material and product.
How to Evaluate a Roll Forming Line for Galvanized Steel
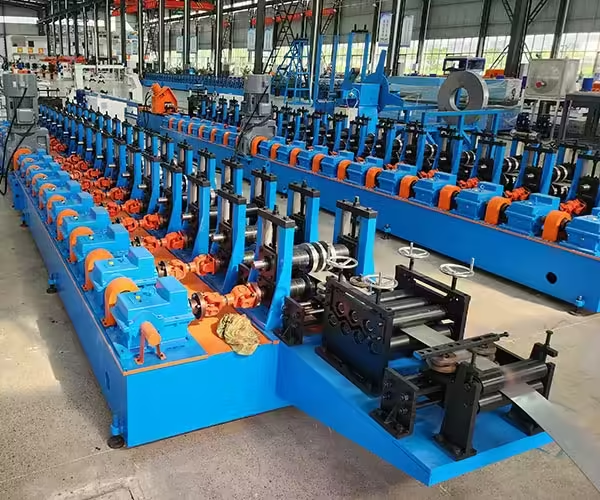
When evaluating equipment, do not focus only on maximum material thickness or forming speed.
Ask how the machine controls the coated strip through the complete process.
Les questions importantes comprennent :
- How is the coil centered?
- How are leveler rolls adjusted?
- What surfaces contact the strip?
- How are entry guides designed?
- How is roll gap established?
- How is tooling cleaned and maintained?
- How are punched particles controlled?
- How is strip feeding managed?
- How does the cut-off system support the profile?
- How are finished parts transferred?
- How are surface defects inspected?
A machine can produce the correct cross-section while still creating unacceptable surface damage.
Equipment evaluation should therefore consider both geometry and coating condition.
Conclusion
Galvanized steel roll forming requires coordinated control of both profile geometry and coated-surface condition.
The zinc-coated strip passes through numerous contact points from decoiling and leveling to feeding, punching, forming, cutting, and stacking. Tooling condition, roller cleanliness, bend progression, roll gap, material properties, guides, and handling can all influence the final result.
Material variation is equally important. Thickness and steel strength affect forming behavior and springback, while the coating influences how carefully the strip needs to be handled throughout production.
The most stable process begins with a clearly defined profile drawing and a complete galvanized steel specification. Tooling can then be developed around the required bends and material behavior, while machine settings and handling systems protect the surface from unnecessary abrasion.
For manufacturers producing construction profiles, photovoltaic mounting components, roofing sections, or other galvanized products, the goal should not simply be to form the steel into the correct shape. The objective is to produce a dimensionally consistent profile while preserving the material condition required for its intended application.
FAQ
What is galvanized steel roll forming?
Galvanized steel roll forming is a continuous cold-forming process that passes zinc-coated steel strip through multiple roller stations to create a specified metal profile.
Can galvanized steel be roll formed without damaging the coating?
Galvanized steel can be roll formed successfully when tooling design, roller surfaces, bend progression, roll pressure, guides, punching, and material handling are properly controlled. Surface condition should still be inspected throughout production.
Why does galvanized steel get scratched during roll forming?
Common causes include damaged or dirty rollers, trapped metal particles, excessive guide contact, inappropriate roll pressure, punching debris, and poor downstream handling.
Does galvanized steel spring back after roll forming?
Yes. Springback is mainly influenced by the mechanical properties of the steel substrate, material thickness, bend geometry, and forming process. Different galvanized steel grades can therefore require different forming adjustments.
What information is needed to configure a roll forming machine for galvanized steel?
Important information includes the finished profile drawing, steel grade, galvanized coating specification, thickness range, strip width, bend geometry, punching pattern, surface requirements, finished length, and expected production range.
Need to Evaluate Galvanized Steel Roll Forming?
Galvanized profile production should be developed around the actual steel grade, coating, thickness, profile geometry, punching requirements, surface expectations, and production process. If you are planning a new forming line, contactez JBLDIE to discuss your material specifications and finished-profile requirements.
 French
 English
 Arabic
 Russian
 Spanish