
دليل شراء آلة الأقواس الكهروضوئية 2027
جدول المحتويات
أهم النقاط
- يجب اختيار آلة الأقواس الكهروضوئية وفقًا للملف النهائي ودرجة المواد ونمط الثقب وحجم الإنتاج ومستوى الأتمتة المطلوب.
- يجب على المشترين مقارنة المخرجات النهائية المؤهلة بدلاً من الاعتماد فقط على سرعة التشكيل القصوى المذكورة في عرض الأسعار.
- قد تتطلب منتجات القناة C، والقناة U، والقناة Z، والسكك الحديدية، والبريد، والموصل تكوينات مختلفة للتشكيل والتثقيب.
- يمكن أن يؤدي التفكيك المتكامل والتسوية والتثقيب وتشكيل اللف والقطع والتكديس إلى تقليل المعالجة اليدوية وتنوع العملية.
- يعد التعديل التلقائي ذا قيمة بالنسبة للمصانع التي تقوم بشكل متكرر بالتبديل بين أبعاد الملف الشخصي أو طلبات العملاء.
- لا تقل قوة خضوع المادة ونوع الطلاء عن سمك المادة عند تصميم البكرات والأعمدة والمحركات وقوالب التثقيب.
- يجب أن يتحقق اختبار قبول المصنع من أبعاد الملف الشخصي ومواقع الفتحات ودقة القطع والاستقامة وجودة السطح والتشغيل المستمر.
- قد لا توفر الآلة الأقل سعرًا أقل تكلفة لكل شريحة مؤهلة.
- يجب على المشترين تأكيد التثبيت والتدريب والتشخيص عن بعد وقطع الغيار والوثائق الفنية قبل تقديم الطلب.
- توفر Jinbolida حلول تشكيل وتثقيب الأقواس الكهروضوئية التي يمكن تخصيصها حول الرسومات والمواد والسعة ومتطلبات المكونات النهائية.
مقدمة
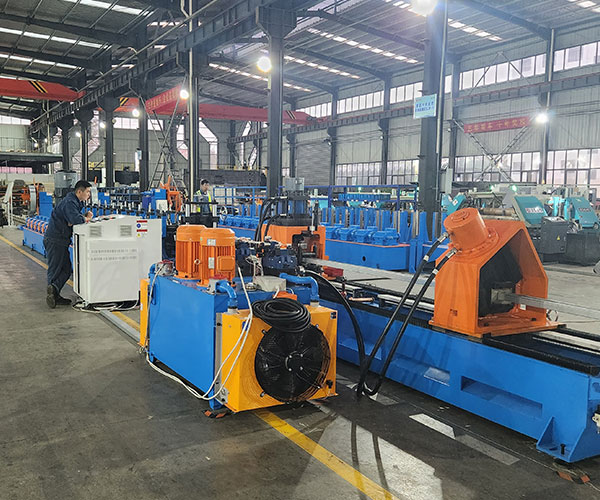
تعتمد أنظمة التركيب الكهروضوئية على مكونات الفولاذ أو الألومنيوم المصنعة بدقة لدعم وحدات الطاقة الشمسية تحت أحمال الرياح والثلوج والاهتزازات والأحمال البيئية طويلة المدى. مع توسع نشر الطاقة الشمسية، يحتاج مصنعو قضبان التثبيت والأعمدة والمدادات والقنوات والموصلات إلى معدات إنتاج يمكنها توفير أبعاد قابلة للتكرار مع التحكم في نفايات المواد ومتطلبات العمالة.
أفادت وكالة الطاقة الدولية للطاقة الكهروضوئية أنه تم تركيب ما يقرب من 698 جيجاوات من القدرة الكهروضوئية الجديدة في جميع أنحاء العالم في عام 2025، مما يجعل القدرة الكهروضوئية العالمية التراكمية تقترب من 3 تيراواط. يؤدي هذا التوسع المستمر في السوق إلى زيادة الطلب في جميع أنحاء سلسلة توريد الطاقة الشمسية، بما في ذلك المعدات المستخدمة لتصنيع مكونات نظام التركيب.
ومع ذلك، فإن شراء آلة قوس كهروضوئية لا يقتصر ببساطة على اختيار أعلى سرعة أو أقل عرض أسعار. قد تكون الآلة التي تعمل بشكل جيد لملف تعريف قناة C واحدة غير مناسبة لمصنع ينتج عدة أحجام لقنوات U، أو مواد عالية القوة، أو فتحات معقدة، أو طلبات مخصصة قصيرة.
يجب أن يتوافق خط الإنتاج المناسب مع مجموعة المنتجات الفعلية للمشتري، ومواصفات المواد، ومساحة المصنع المتاحة، وظروف العمل، ومتطلبات الجودة، وخطة التوسع.
جينبوليدا فئة آلة تشكيل القوس الكهروضوئي الشمسي يتضمن معدات مصممة لمعالجة الفولاذ الكربوني والفولاذ المجلفن والألمنيوم في مقاطع لتطبيقات التركيب بالطاقة الشمسية. يقدم الموقع أيضًا مخصصًا معدات تثقيب الرفوف الشمسية الكهروضوئية بالنسبة للمنتجات التي تتطلب فتحات تثبيت أو فتحات ممدودة أو ميزات الموصل.
يشرح هذا الدليل كيف يمكن للمشترين تقييم تكوينات الماكينة والقدرة الإنتاجية والأدوات والأتمتة والاختبار وقدرة الموردين قبل الاستثمار في عام 2027.
ما هي آلة القوس الكهروضوئية؟
آلة الأقواس الكهروضوئية هي نظام إنتاج صناعي يستخدم لتصنيع المكونات المعدنية لهياكل تركيب الوحدات الشمسية.
اعتمادًا على المنتج النهائي، قد ينتج النظام ما يلي
- قنوات دعم على شكل حرف C
- قضبان تثبيت على شكل حرف U
- مدادات على شكل حرف Z
- ملفات تعريف سيجما
- قنوات تبختر مشقوقة
- مشاركات التثبيت الأرضي
- قضبان التثبيت على السقف
- الأقواس والعوارض
- لوحات موصل
- مكونات القوس الثلاثي
- ملفات تعريف القسم المفتوح المخصصة
يتم تصنيع معظم المقاطع الهيكلية الطويلة من خلال تشكيل اللفة الباردة. يمر شريط معدني مسطح عبر محطات أسطوانية متعددة، وتقوم كل محطة بتغيير الشريط تدريجيًا حتى يتم تشكيل المقطع العرضي المطلوب.
تشكيل لفة باردة
تشكل اللفة الباردة تشكيل المعدن في درجة حرارة الغرفة من خلال تسلسل مستمر من البكرات. إنها مناسبة بشكل خاص للمقاطع الطويلة التي تتطلب مقطعًا عرضيًا ثابتًا.
يمكن أن توفر العملية إمكانية تكرار عالية واستخدامًا فعالاً للمواد عندما يكون تصميم الأسطوانة ونظام التغذية والمحاذاة وطريقة القطع متطابقًا بشكل صحيح مع المنتج.
اللكم
يؤدي التثقيب إلى إنشاء فتحات مستديرة أو فتحات ممدودة أو تحديد موقع الثقوب أو فتحات المسامير أو فتحات مخصصة في المادة.
قد تتم العملية قبل التشكيل، أو أثناء عملية الخط، أو بعد تشكيل الملف الشخصي. يعتمد الترتيب الصحيح على إمكانية الوصول والتسامح وهندسة الثقب وسرعة الإنتاج.
القطع
يقوم نظام القطع بفصل المظهر الجانبي المستمر إلى أطوال محددة.
تشمل الترتيبات المشتركة أنظمة ما قبل القطع، وما بعد القطع، وأنظمة التوقف للقطع، وأنظمة القطع الطائرة. تخلق كل طريقة متطلبات مختلفة للسرعة والتحكم في تشوه الملف الشخصي وتكلفة الأدوات وتنسيق الخط.
كيف يعمل خط إنتاج الأقواس الكهروضوئية؟
قد يقوم خط الإنتاج الكامل بإجراء عدة عمليات دون نقل المادة بشكل متكرر بين آلات منفصلة.
دليل جينبوليدا ل تخطيطات خط آلة تشكيل قوس الدعم الشمسي يصف الخط بأنه نظام قد يشمل إزالة اللف، والتسوية، والتغذية، والتثقيب، والتشكيل، والقطع، ووضع العلامات، والتفريغ، والخراطة، والتكديس.
الخطوة 1: تحميل الملف
يتم وضع ملف من الفولاذ أو الألومنيوم على آلة فك اللفائف.
يدعم جهاز فك اللف الملف ويحرر الشريط بمعدل متحكم فيه. يجب أن تتوافق سعة وزنها ونطاق التمدد مع أبعاد الملف الخاص بالمشتري.
الخطوة 2: إزالة التربة
يتم فك الملف تدريجيًا وتغذيته باتجاه قسم التسوية.
قد يتم تفضيل آلة فك اللف التي تعمل بالطاقة للملفات الأثقل أو خطوط الإنتاج الأسرع، في حين أن الوحدة السلبية يمكن أن تكون كافية للتطبيقات الأخف والأبطأ.
الخطوة 3: التسوية
يزيل جهاز التسوية جزءًا من انحناء الملف ويساعد في إنشاء شريط ثابت قبل التثقيب أو التشكيل.
قد يؤثر ضعف التسوية على دقة التغذية، وموضع الثقب، واستقامة المظهر الجانبي، واستقرار التشكيل.
الخطوة 4: التغذية المؤازرة
يقوم نظام التغذية بتحريك المادة بمسافة مبرمجة.
يعد التحكم المؤازر مهمًا بشكل خاص عندما يحتوي ملف التعريف على أنماط فتحات متعددة أو عدة أطوال للمكونات ضمن ترتيب واحد.
الخطوة 5: اللكم
تنتج وحدات التثقيب الهيدروليكية أو الميكانيكية الفتحات المطلوبة.
قد يستخدم الخط قالبًا واحدًا لنمط متكرر بسيط أو عدة محطات للثقوب والفتحات المتعددة.
الخطوة 6: تشكيل لفة
يمر الشريط عبر سلسلة من محطات التشكيل.
يعتمد عدد المحطات على تعقيد المظهر الجانبي وخصائص المواد والسمك والتسامح وجودة السطح المطلوبة.
الخطوة 7: الاستقامة
يقوم جهاز التقويم بإجراء التعديلات النهائية لتقليل حركة القوس أو الالتواء أو الجانب.
لماذا الاستقامة النهائية مهمة
Even accurately designed rollers may require final correction because material properties can vary between coils.
A practical straightening mechanism allows trained operators to compensate for normal material variation without rebuilding the tooling.
الخطوة 8: القطع حسب الطول
The profile is cut according to programmed order data.
A measuring encoder and control system coordinate the cutting position to reduce length errors.
الخطوة 9: الاستلام والتكديس
Finished profiles move onto a receiving table or automatic stacking system.
This section can reduce scratches, prevent long profiles from falling, improve bundle consistency, and lower manual handling requirements.
الأنواع الرئيسية لآلات الأقواس الكهروضوئية
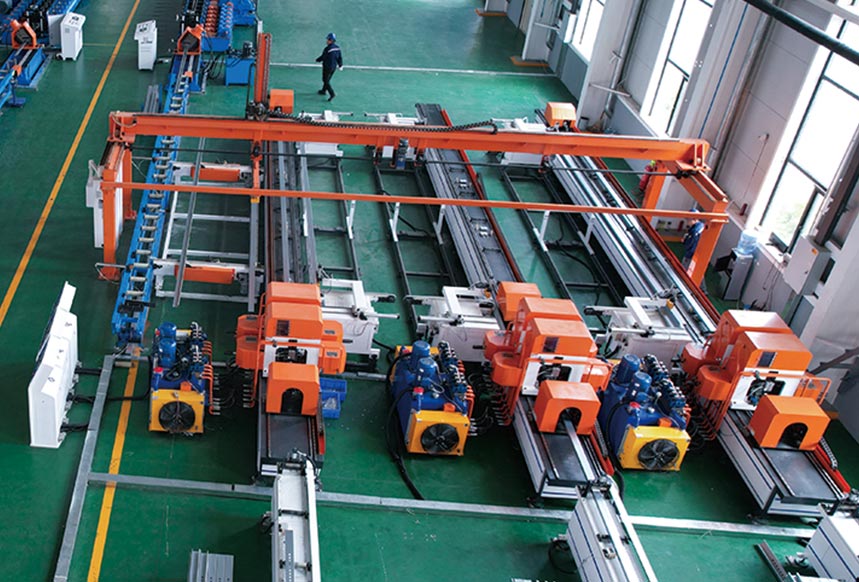
The machine type should follow the finished product rather than a general industry label.
آلة القوس الكهروضوئية ذات القناة C
A C-channel profile includes a web, two flanges, and sometimes return lips.
These profiles are commonly used as structural rails, posts, purlins, or support members. The forming process must control flange height, lip angle, opening width, twist, and straightness.
إنتاج قناة C قابل للتعديل
An adjustable system can produce a range of web and flange sizes.
This configuration is useful when a factory serves several solar-project customers, but the buyer should confirm which dimensions adjust automatically and which still require tooling changes.
آلة القوس الكهروضوئية على شكل حرف U
A U-channel generally has a base and two side walls without inward lips.
Although the geometry may appear simpler than a lipped C section, the line must still control side-wall angle, internal width, base width, and straightness.
آلة تشكيل القناة Z
A Z profile uses offset flanges on opposite sides of the web.
These profiles may be selected when overlapping, nesting, or structural connection requirements favor a Z-shaped cross-section.
آلة قناة تبختر
Strut channels may include inward edges, serrations, repeated slots, and specialized connection surfaces.
Because these products often contain dense hole patterns, punching capacity can become the limiting factor in the overall production speed.
آلة تثقيب وتشكيل الموصل
Short connector components may require stamping, punching, cutting, and forming rather than continuous roll forming alone.
Jinbolida’s photovoltaic bracket connector punching machine is presented as a solution capable of producing components within approximately three to five seconds, with stated accuracy of ±0.5 mm for the referenced configuration. Exact performance should be reconfirmed against the buyer’s material, component drawing, and acceptance requirements.
آلات القوس الكهروضوئية ذات القناة C مقابل القناة U
Choosing between C- and U-profile equipment requires more than comparing the visible profile shape.
| عنصر المقارنة | آلة القناة C | آلة القناة على شكل حرف U |
|---|---|---|
| Typical profile | Lipped or unlipped C section | Open U section |
| Common applications | المشاركات والمدادات والقضبان والعوارض | القضبان والإطارات والدعم |
| تشكيل التعقيد | Often higher with return lips | Often simpler, depending on design |
| الأبعاد الرئيسية | الويب والشفة والشفة والفتح | Base width, wall height and angle |
| موقف اللكم | Web, flange or multiple faces | Base or side walls |
| Adjustment options | Width, flange and lip adjustment | Width and wall-height adjustment |
| Main quality risks | Twist, lip-angle error and flare | Side-wall angle and spreading |
| Best purchasing basis | Exact product family and tolerance | Exact product family and tolerance |
Jinbolida has published a dedicated comparison of C- and U-profile solar mounting bracket machines. The article emphasizes that machine selection also depends on material, hole patterns, adjustment requirements, and target capacity rather than profile shape alone.
اللكم المسبق مقابل اللكم اللاحق
The location of the punching process can affect line speed, tooling design, and dimensional accuracy.
اللكم المسبق
Pre-punching creates holes while the material remains flat.
The punching die can access the strip easily, and flat material is usually simpler to position. However, the forming process may slightly influence the final relationship between the holes and the formed profile.
بعد اللكم
Post-punching creates openings after the profile has been formed.
This arrangement can reference the final profile geometry, but the punching tools may need to reach several faces of a three-dimensional section.
ما هي الطريقة الأفضل؟
Neither arrangement is universally better.
The supplier should evaluate:
- شكل ثقب
- حجم الثقب
- تباعد الثقب
- هندسة الملف الشخصي
- سمك المادة
- التسامح المطلوب
- تردد اللكم
- سرعة الخط
- يموت إمكانية الوصول
- Potential profile deformation
اللكم الهجين
Some production lines use both pre-punching and post-punching.
For example, repeated base slots may be punched in the flat strip, while a specialized side hole is created after forming.
خطوط الإنتاج الأوتوماتيكية مقابل شبه الأوتوماتيكية
Automation should be evaluated through the buyer’s production model.
| عامل | خط شبه أوتوماتيكي | Automatic Line |
| Initial equipment cost | أقل عموما | أعلى عموما |
| العمالة المباشرة | أعلى | أدنى |
| اعتماد المشغل | أكبر | مخفض |
| طريقة التحول | Mostly manual | Motorized or recipe-based |
| بيانات الإنتاج | أساسي | أكثر شمولا |
| Line coordination | Partially connected | Centrally coordinated |
| Traceability | محدود | Easier to implement |
| Technical complexity | أدنى | أعلى |
| الإنتاج المناسب | Lower volume or stable profiles | Higher volume or varied orders |
| إمكانية التوسع | معتدل | Usually stronger |
متى تختار آلة شبه أوتوماتيكية
A semi-automatic photovoltaic bracket machine may be suitable when the factory produces a limited number of stable profiles and has sufficient operators.
It can also be a practical entry-level choice for a manufacturer testing a new market before investing in full automation.
متى تختار الآلة الأوتوماتيكية
An automatic line is more suitable when order volume is high, labor availability is limited, changeovers occur frequently, or customers require detailed production records.
The financial decision should consider cost per qualified profile rather than equipment price alone.
الحجم الثابت مقابل الآلات القابلة للتعديل
This is one of the most important choices for a buyer.
آلة ذات حجم ثابت
A fixed-size line is designed for one profile or a narrow range of similar dimensions.
It usually has simpler tooling, fewer adjustment mechanisms, and a lower initial cost.
أفضل تطبيق
A fixed-size machine is a strong option when the factory has a long-term contract for one standardized product.
It may provide high stability because operators do not frequently change roller positions.
آلة قابلة للتعديل
An adjustable line changes selected profile dimensions through manual screws, motorized positioning, servo systems, interchangeable spacers, or replaceable cassettes.
It is suitable for factories that produce several related sizes.
قيود مهمة
“Adjustable” does not necessarily mean that every dimension can change automatically.
The buyer should request an adjustment matrix showing:
- Adjustable web range
- Adjustable flange range
- نطاق الشفاه القابل للتعديل
- Supported thickness range
- Required roller replacement
- Required spacer replacement
- Punching-die changes
- Cutting-die changes
- وقت التغيير المتوقع
كيفية حساب الطاقة الإنتاجية المطلوبة
Purchasing an oversized line increases investment, while purchasing an undersized line may prevent the factory from meeting delivery schedules.
ابدأ بالطلب السنوي
Determine the expected number of profiles or total linear meters required each year.
Separate confirmed demand from potential demand so that the equipment decision is not based only on an optimistic sales forecast.
حساب وقت الإنتاج المتاح
Available hours should exclude:
- Planned maintenance
- تحولات المنتج
- استبدال الملف
- فحص الجودة
- فواصل المشغل
- Tool cleaning
- التأخير المادي
- Unexpected stoppages
تحويل سرعة التشكيل إلى الإخراج النهائي
A line speed of 30 meters per minute does not always produce 30 meters of qualified product every minute.
Punching cycles, stop-to-cut operations, short product lengths, stacking delays, and operator intervention can reduce effective output.
استخدم الإخراج المؤهل
Qualified output refers to finished components that meet all dimensional and appearance requirements.
منطق القدرات البسيط
A practical estimate can be based on:
Qualified output per shift = effective line speed × operating minutes × utilization rate
The utilization rate should be realistic rather than theoretical. Factories with frequent product changes should use a lower utilization assumption than factories producing one continuous profile.
المعلومات المادية المطلوبة قبل تصميم الماكينة
A reliable machine quotation requires more than a PDF drawing.
درجة المواد
The material grade affects strength, springback, forming load, and tooling wear.
Two coils with the same thickness may behave differently if their yield strengths are significantly different.
نطاق السماكة
The supplier must know the minimum, normal, and maximum material thickness.
A very wide thickness range may require additional adjustment, roller clearances, or separate tooling.
قوة الخضوع
Yield strength indicates how much stress is required before the material begins permanent deformation.
Higher yield strength can increase forming force and springback.
قوة الشد
Tensile strength describes the maximum stress the material can withstand before fracture.
It helps the engineering team understand the overall behavior of the strip during forming and punching.
طلاء السطح
Common materials may include pre-galvanized steel, hot-dip galvanized steel, zinc-aluminum-magnesium-coated steel, stainless steel, carbon steel, or aluminum.
حماية الأسطح المطلية
Roller finish, material guidance, lubrication, and handling systems must be selected carefully when the coating must remain visually and functionally intact.
A poorly aligned line can scratch the surface even when the final dimensions are correct.
مواصفات الآلة الأساسية للمقارنة
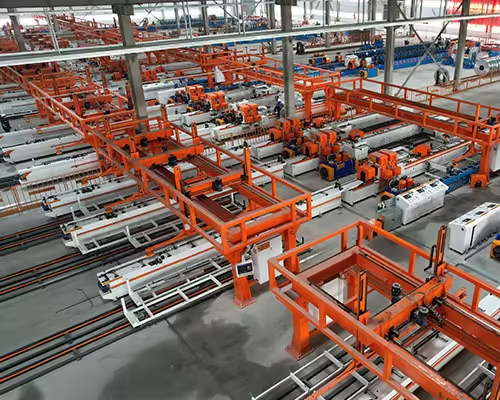
A machine quotation may contain many numbers, but buyers should identify which specifications determine real production performance.
سرعة التشكيل
Ask whether the stated speed refers to:
- Empty machine speed
- Forming-only speed
- Speed without punching
- Speed without cutting
- Maximum short-duration speed
- Continuous qualified production speed
عدد محطات التشكيل
More stations do not automatically guarantee better quality.
The correct number depends on the amount of deformation, material strength, profile shape, surface requirements, and available factory length.
قطر رمح
Shaft diameter affects rigidity and load capacity.
However, it should be evaluated together with shaft material, bearing arrangement, station spacing, frame structure, and profile load.
مادة الأسطوانة
Common tooling materials may be selected according to wear resistance, machinability, heat treatment, and product surface requirements.
The buyer should ask for the roller material specification and hardness rather than accepting a general description such as “high-quality steel.”
قوة المحرك الرئيسي
Motor power must support the actual forming load with an appropriate safety margin.
An unnecessarily large motor may increase energy use, while an undersized motor can reduce production stability.
دقة القطع
Cutting accuracy depends on the measuring system, encoder installation, control logic, material slip, and cutting method.
دقة اللكمة
Punching accuracy should be defined by a measurable reference.
For example, the contract should explain whether hole position is measured from the profile end, profile centerline, previous hole, or another datum.
تفاوتات المنتج التي ينبغي تحديدها
General statements such as “high precision” are not sufficient for machine acceptance.
أبعاد المقطع العرضي
Define acceptable tolerances for:
- عرض الويب
- ارتفاع شفة
- طول الشفاه
- عرض الافتتاح
- Internal width
- Profile height
الدقة الزاوية
Specify allowable deviation for flange, side-wall, and lip angles.
الاستقامة
Straightness may be measured over the full profile length or over a specified shorter distance.
تطور
Twist refers to rotational deviation along the length of the profile.
لماذا يعتبر الالتواء مهمًا
A twisted mounting rail can create installation difficulty even when every individual cross-sectional measurement appears acceptable.
The acceptance procedure should define both the measuring method and the maximum permissible twist.
موقف الحفرة
Specify longitudinal and transverse hole-location tolerance.
For slotted holes, also define slot length, width, orientation, and distance from the reference edge.
طول القطع
Define permissible positive and negative length deviation.
For installation systems using repeated modular spacing, accumulated length error can become particularly important.
كيف تؤثر قدرة التثقيب على سرعة الخط
Many buyers focus on the roll former, but punching is often the true production bottleneck.
كمية الحفرة لكل ملف تعريف
A profile containing one hole every meter requires less punching capacity than a slotted channel containing several openings every few centimeters.
عدد محطات التثقيب
Multiple stations can distribute different hole types or process several surfaces.
Jinbolida presents three-station, six-station, and nine-station photovoltaic rack punching equipment for varying processing needs. Buyers should select the arrangement based on actual hole combinations rather than station count alone.
التثقيب الهيدروليكي مقابل الميكانيكي
Hydraulic systems provide controllable force and flexible integration.
Mechanical presses may be appropriate for high-frequency repetitive punching, depending on the product and tooling arrangement.
اللكم أثناء التحرك
A flying punching system processes material without fully stopping the line.
هل اللكم الطائر ضروري دائمًا؟
لا.
Flying punching adds cost and control complexity. It creates the most value when punching would otherwise significantly limit production and when the buyer’s order volume justifies the additional investment.
كيفية تقليل الخردة ونفايات المواد
Material cost has a direct impact on bracket profitability.
تحسين عرض الشريط
The required strip width should be calculated from the finished profile and forming allowance.
Using an unnecessarily wide coil creates continuous edge waste across every meter of production.
محاذاة ملف التحكم
Sideways strip movement can create uneven profiles and damaged edges.
Guiding devices should hold the material accurately without scratching the coating.
استخدم تغذية مؤازرة دقيقة
Controlled feeding reduces hole-position and cutting errors.
It also makes it easier to change between component lengths through the control program.
أداة المراقبة
Worn punches and cutting blades can create burrs, deformation, and rejected parts.
الخردة هي إشارة عملية
A sudden increase in scrap may indicate coil variation, tooling wear, incorrect adjustment, sensor contamination, feed slip, or operator error.
Recording the reason for each rejected part helps the factory identify recurring losses.
الضوابط الذكية وبيانات الإنتاج
Industrial buyers are increasingly interested in data that supports production planning and maintenance.
إدارة الوصفات
A recipe stores relevant settings for a specific profile or order.
Depending on the line, a recipe may include length, quantity, hole spacing, punching sequence, and adjustable profile dimensions.
إدارة النظام
Operators can enter the required product quantity and monitor completed and remaining pieces.
سجلات الإنذار
Alarm history helps maintenance teams identify repeated failures.
التشخيص عن بعد
Authorized remote access can allow the supplier to inspect control parameters, sensor status, and fault records.
الأمن السيبراني والتحكم في الوصول
Remote access should be controlled by the machine owner.
The buyer should confirm how connections are approved, when access is enabled, and how passwords or user permissions are managed.
اعتبارات كفاءة الطاقة ودورة الحياة
Energy use is becoming a more visible part of industrial equipment evaluation.
The IEA’s clean-technology manufacturing research examines production costs, supply-chain concentration, investment, and manufacturing performance across the solar value chain. The IEA PVPS also released updated photovoltaic lifecycle inventory data in July 2026, reflecting greater industry attention to transparent environmental assessment.
أنظمة قيادة فعالة
Properly sized motors and efficient transmissions can reduce unnecessary energy consumption.
إدارة الاستعداد
Pumps, fans, and auxiliary units do not always need to operate at full output during extended production pauses.
كفاءة المواد
For many bracket factories, reducing steel waste may create a larger financial benefit than reducing electricity consumption alone.
قياس الطاقة لكل منتج مؤهل
Total machine power does not explain production efficiency by itself.
A useful metric is the energy consumed per meter, kilogram, or qualified finished component.
تخطيط تخطيط المصنع
The buyer should plan the production area before the machine is manufactured.
طول الخط
A complete line may require space for:
- Coil storage
- تحميل الملف
- إزالة التربة
- Forming equipment
- خزائن كهربائية
- Hydraulic stations
- Receiving tables
- التراص
- فحص
- التعبئة والتغليف
- الوصول إلى الصيانة
تدفق المواد
Raw coils and finished bundles should move through the factory without repeated crossing or turning.
الوصول إلى الرافعة والرافعة الشوكية
The layout must allow safe coil loading and finished-product removal.
متطلبات التأسيس
Some machines require anchor bolts, foundation pits, or reinforced flooring.
لا تتجاهل مساحة الصيانة
Operators may need access to rollers, motors, chains, hydraulic units, electrical cabinets, and cutting dies.
A line installed too close to a wall can make routine maintenance unnecessarily difficult.
كيفية تقييم مورد آلة القوس الكهروضوئية
The supplier should be evaluated as an engineering and service partner, not only as a machine seller.
تحليل الملف الشخصي
A capable supplier should review whether the profile can be formed continuously and identify areas that may create cracking, springback, twisting, or difficult punching access.
تصميم الأدوات
Ask whether rollers and dies are designed internally.
Internal engineering can make future modifications and technical communication more efficient.
تصنيع المكونات
Review how rollers, shafts, frames, cutting tools, and punching dies are manufactured and inspected.
التجميع والاختبار
The complete line should be assembled and tested before shipment.
تجربة مشروع مماثلة
Ask for examples involving comparable profiles, materials, thicknesses, punching patterns, and automation requirements.
مماثلة لا تعني متطابقة
A supplier may have produced a C-channel line before, but your product could still require a different forming sequence because of material strength, dimensions, lip geometry, or tolerance.
The supplier should explain both the relevant experience and the required customization.
الأسئلة التي يجب طرحها أثناء تقييم المورد
Use practical questions that reveal how the proposed line will work.
أسئلة هندسية
- Has the supplier reviewed the full profile drawing?
- Has the material yield strength been confirmed?
- Which dimensions can be adjusted?
- Which parts require replacement during changeover?
- كيف يتم تعويض الربيع؟
- How will profile twist be corrected?
- Where will punching take place?
- What limits the actual line speed?
أسئلة التصنيع
- What materials are used for rollers and shafts?
- How are rollers heat-treated?
- How are shafts and rollers measured?
- Is the frame welded or cast?
- How is frame stress handled?
- Which electrical and hydraulic components are used?
أسئلة الاختبار
- Will testing use the customer’s real material?
- How long will the continuous test run last?
- How will profile tolerances be measured?
- Will every hole pattern be tested?
- Will changeover be demonstrated?
- Will production data be recorded?
أسئلة الخدمة
- هل يتوفر الدعم الفني عن بعد؟
- Is on-site installation available?
- ما هي قطع الغيار المدرجة؟
- How quickly can replacement parts be shipped?
- Are manuals supplied in the required language?
- Are electrical and hydraulic diagrams included?
قائمة مراجعة اختبار قبول المصنع
A formal factory acceptance test helps prevent disagreements before shipment.
| عنصر الاختبار | ما يجب التحقق منه | الأدلة الموصى بها |
| تغذية المواد | Stable entry and alignment | Continuous operating video |
| اللكم | Hole size, shape and position | Inspection report |
| أبعاد الملف الشخصي | Web, flange, lip and angles | Measured sample records |
| الاستقامة | القوس والانحراف الجانبي | Straightness measurement |
| تطور | Rotation along profile length | Full-length sample check |
| طول القطع | Programmed vs actual length | Multiple measured pieces |
| جودة السطح | Scratches, dents and coating damage | الفحص البصري |
| سرعة الإنتاج | Qualified output under real conditions | Timed production test |
| التحول | Adjustment procedure and duration | Demonstration video |
| نظام التحكم | Recipes, alarms and order quantities | اختبار وظيفي |
| أجهزة السلامة | Guards, emergency stops and interlocks | قائمة التحقق من السلامة |
| التشغيل المستمر | Stability over an agreed period | تقرير الاختبار |
استخدم المادة الصحيحة
Testing a high-strength production line with thin, soft steel does not prove that it will process the customer’s real coil.
The test material should match the agreed grade, thickness, width, and coating whenever practical.
قياس أكثر من عينة واحدة
One qualified component is not enough to demonstrate process stability.
Samples should be taken from different stages of the continuous test run.
أخطاء شائعة في شراء آلة الأقواس الكهروضوئية
الاختيار حسب السعر وحده
A low quotation may exclude essential items such as punching dies, automatic adjustment, loading equipment, receiving tables, installation, spare parts, or electrical upgrades.
Compare the full technical scope.
الاختيار بأقصى سرعة
Maximum speed may refer only to the roll former without punching or cutting.
Ask for the estimated number of qualified finished profiles per shift.
تجاهل القوة المادية
Thickness alone is not sufficient.
A line designed for low-strength steel may not perform correctly with a higher-yield-strength coil of the same thickness.
تتطلب الكثير من المرونة
A machine designed to produce an extremely wide range of unrelated profiles may become expensive and difficult to adjust.
Sometimes two focused lines are more practical than one overly complex line.
ترك التسامح غير محدد
Without written acceptance criteria, the supplier and buyer may use different definitions of acceptable quality.
تجاهل دعم ما بعد البيع
A machine may operate for many years, while the initial purchase process lasts only a few months.
Service capability should therefore be evaluated before the order is placed.
كم تكلفة آلة القوس الكهروضوئية؟
There is no single standard price because production-line configurations vary significantly.
The quotation may be affected by:
- عدد أحجام الملف الشخصي
- قوة المادة
- نطاق السماكة
- وزن الملف
- Forming-station quantity
- Roller and shaft materials
- Punching-station quantity
- Hole complexity
- طريقة القطع
- Adjustment system
- التراص التلقائي
- Electrical component brands
- Hydraulic configuration
- متطلبات السلامة
- شهادة
- وجهة التثبيت
- Training and service scope
قارن إجمالي الاستثمار
The machine price is only one part of the investment.
Buyers should also consider freight, customs, installation, foundation work, lifting equipment, power supply, compressed air, tooling, spare parts, training, and initial raw material.
قارن التكلفة لكل مكون مؤهل
A more expensive line may provide a lower manufacturing cost when it reduces labor, changeover time, scrap, and rejected products.
طلب عرض أسعار مفصل
An itemized quotation makes it easier to understand what is included and compare suppliers fairly.
It also allows the buyer to identify optional equipment that can be added during a later expansion.
كيفية إعداد طلب عرض أسعار دقيق
A detailed request for quotation can significantly improve the quality of the proposal.
تقديم المعلومات التالية:
- Finished profile drawing
- Several profile sizes, when applicable
- درجة المواد
- العائد وقوة الشد
- الحد الأدنى والحد الأقصى للسمك
- عرض الملف
- الحد الأقصى لوزن الملف
- طلاء السطح
- رسومات الثقب والفتحة
- أطوال المنتج
- التحمل الأبعاد
- Required pieces per hour or shift
- Expected working hours
- Number of changeovers
- مستوى الأتمتة المطلوب
- متطلبات الاستلام والتكديس
- جهد وتردد المصنع
- بلد التثبيت
- Required certifications
- العلامات التجارية للمكونات المفضلة
- Factory-layout restrictions
- Sample products, when available
جينبوليدا photovoltaic support manufacturing guide provides additional information about C- and U-channel production equipment and related support-component manufacturing.
لماذا تفكر في جينبوليدا لآلة الأقواس الكهروضوئية؟
Jinbolida provides equipment for forming and punching structural components used in photovoltaic mounting systems.
التكوين على أساس المنتج
The proposed line can be configured around the customer’s finished profile, material type, size range, hole pattern, and capacity requirement.
معدات التشكيل
The company’s photovoltaic forming-machine category covers equipment for producing C-shaped, U-shaped, and related mounting profiles from metal coil.
معدات اللكم
Dedicated rack punching systems can be considered for products containing repeated installation holes, elongated slots, or multi-face features.
تكامل خط الإنتاج
Forming, punching, cutting, and auxiliary handling can be evaluated as one production system.
طلب اقتراح على أساس الرسم
Buyers can submit profile drawings, material information, production targets, and factory requirements through the صفحة الاتصال جينبوليدا.
A drawing-based proposal is more useful than selecting equipment only from a general catalog because it allows the engineering team to evaluate actual manufacturing conditions.
الأسئلة الشائعة حول آلات الأقواس الكهروضوئية
ما هي الآلة المستخدمة لصنع الأقواس الكهروضوئية؟
Long photovoltaic mounting profiles are commonly produced with cold roll forming machines. A complete line may include decoiling, leveling, servo feeding, punching, forming, cutting, receiving, and stacking equipment.
هل يمكن لآلة قوس كهروضوئية واحدة أن تصنع أحجامًا مختلفة للملفات الشخصية؟
Yes, some machines can produce several related sizes through manual, motorized, or servo adjustment. However, the buyer should confirm the exact adjustment range and whether rollers, spacers, punching dies, or cutting tools must be replaced.
هل يمكن لنفس الجهاز إنتاج قنوات C وU؟
It may be possible when the profiles are sufficiently related and the machine is designed with interchangeable or adjustable tooling. In other cases, separate tooling or separate lines may be more efficient.
ما هي المادة التي يمكن لآلة القوس الكهروضوئية معالجتها؟
Depending on its design, the line may process carbon steel, galvanized steel, coated steel, stainless steel, or aluminum. The material grade, yield strength, thickness, width, and coating must be confirmed before machine design.
ما مدى سرعة خط إنتاج الأقواس الكهروضوئية؟
Actual speed depends on profile complexity, hole frequency, punching method, material properties, cut length, and stacking arrangement. Buyers should ask for qualified finished output under their real production conditions.
كم عدد المشغلين المطلوبين؟
A basic line may require operators for coil loading, machine control, product collection, inspection, and packaging. Automatic feeding and stacking can reduce direct labor, but staffing still depends on the factory layout and production process.
هل تعديل العرض التلقائي ضروري؟
Automatic adjustment is useful when profile sizes change frequently. It may not be economically necessary when the factory continuously produces one standard profile.
هل يجب ثقب الثقوب قبل التشكيل أم بعده؟
Both arrangements are used. Pre-punching provides easier access to flat material, while post-punching can reference the final formed shape. The best method depends on geometry, tolerance, speed, and tooling access.
ما مدى دقة آلة القوس الكهروضوئية؟
Accuracy depends on the machine design, material consistency, tooling, control system, measuring method, and product length. Buyers should specify tolerances for profile dimensions, angles, straightness, twist, holes, and cutting length.
كيف يمكنني منع الخدوش على المقاطع المجلفنة؟
Use smooth and correctly aligned rollers, suitable material guidance, clean equipment, appropriate lubrication where permitted, and controlled receiving systems. The factory acceptance test should include a surface-quality inspection.
ما الذي يسبب التواء الملف الشخصي؟
Possible causes include uneven material properties, incorrect roller alignment, poor forming-sequence design, unequal deformation, feeding misalignment, or improper straightener settings.
ما الفرق بين سرعة التشكيل وسرعة الإنتاج؟
Forming speed describes material movement through the roller section. Production speed includes punching, cutting, acceleration, deceleration, stacking, coil replacement, and other process delays.
هل يمكن للآلة معالجة الفولاذ عالي القوة؟
Yes, but the line must be designed for the specified yield strength and thickness. Higher-strength steel may require stronger frames, larger shafts, greater motor power, revised tooling, and more springback compensation.
كم من الوقت يستغرق تغيير الملف الشخصي؟
It may take a few minutes for an automated adjustment or much longer when rollers and dies must be replaced. The supplier should demonstrate the complete procedure during testing.
ما هي المستندات التي يجب أن تأتي مع الجهاز؟
Typical documents include an operation manual, electrical diagram, hydraulic diagram, foundation drawing, maintenance schedule, spare-parts list, parameter backup, and tooling information.
ما الذي يجب تضمينه في خدمة ما بعد البيع؟
Buyers should confirm installation guidance, operator training, remote diagnostics, spare-parts support, warranty terms, technical-response procedures, and access to electrical and control documentation.
كيف يمكنني الحصول على عرض أسعار دقيق للآلة؟
Provide complete profile drawings, material specifications, hole patterns, tolerance requirements, product lengths, output targets, voltage, factory layout, and required automation level.
خاتمة
Buying a photovoltaic bracket machine in 2027 requires a detailed evaluation of products, materials, production volume, punching patterns, adjustment needs, tolerances, factory layout, and technical support.
The best machine is not automatically the fastest or cheapest option. It is the production line that can consistently manufacture qualified components at a sustainable cost while supporting the buyer’s order structure and future growth.
Before placing an order, buyers should define the finished product, submit complete material information, calculate realistic capacity, compare total line configurations, and agree on a measurable factory acceptance standard.
لوازم جينبوليدا آلات تشكيل الأقواس الشمسية الكهروضوئية و معدات تثقيب الرف الكهروضوئي for C-channel, U-channel, connector, and customized solar mounting components.
Manufacturers planning a new production line or upgrading an existing workshop can contact Jinbolida with their profile drawings, material specifications, desired output, and automation requirements to obtain a customized equipment proposal.
إذا أعجبك هذا المقال حول خبرة شركة Jinbolida في التصنيع الذكي والمصانع الرقمية، فتابعنا للحصول على المزيد من الأفكار والتحديثات:
- 📘 فيسبوك: ترقبوا أحدث مشاريع خطوط الإنتاج الذكية لدينا → فيسبوك
- 📱 WhatsApp: اتصل بنا في أي وقت للحصول على حلول إنتاج مخصصة → الدردشة الآن
- ▶️ YouTube: شاهد عروضنا التوضيحية للخطوط الآلية وتطبيقاتنا الواقعية → يوتيوب
لنواصل الابتكار وتشكيل مستقبل التصنيع الذكي - معًا!
 Arabic
 English
 Russian
 Spanish
 French