
PV Bracket Punching Machine: Control Hole Accuracy
Table of Contents
Introduction
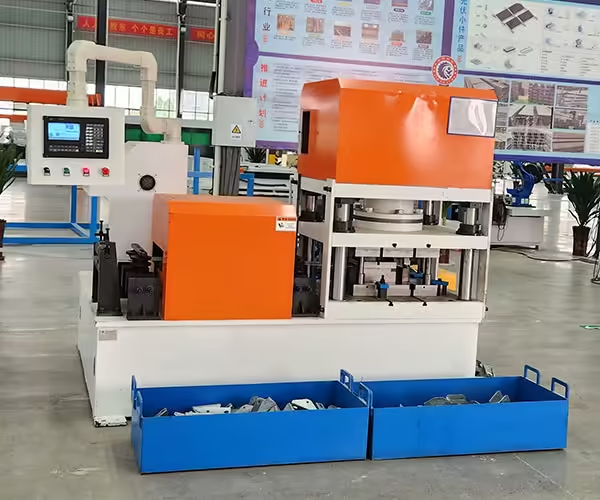
A photovoltaic mounting profile can have the correct C-channel or U-channel dimensions and still become difficult to assemble if its mounting holes are positioned incorrectly. For long solar support rails containing dozens of round holes, elongated slots, connection openings, or side holes, punching accuracy is therefore just as important as profile-forming accuracy.
The challenge is that hole accuracy does not depend on the punching die alone.
A PV bracket punching machine needs to coordinate material positioning, servo feeding, strip tension, clamping, die clearance, punching sequence, encoder feedback, material strength, temperature, cutting position, and—in many production lines—the downstream roll forming process.
This becomes increasingly important as photovoltaic manufacturing serves a broader range of markets and project formats. IEA PVPS reported that approximately 698 GW of new photovoltaic capacity was installed globally in 2025 and that 39 countries installed at least 1 GW during the year, reinforcing the continued diversification of photovoltaic deployment.
For bracket manufacturers, more markets can mean more profile dimensions, mounting interfaces, hole patterns, and project-specific requirements.
The most useful question is therefore not simply:
How accurate is the punching machine?
It is:
How does the complete production system prevent hole-position error from accumulating from the first hole to the last hole of the finished PV bracket?
This guide explains where those errors originate and what equipment buyers should verify before selecting a photovoltaic bracket punching system.
Why Hole Accuracy Matters in PV Bracket Production
Photovoltaic mounting structures connect many individual components.
Depending on the system design, holes and slots can be used for:
- rail connections,
- post connections,
- purlin attachment,
- braces,
- mounting clamps,
- fasteners,
- connector plates,
- height adjustment,
- and installation positioning.
The U.S. Department of Energy describes photovoltaic mounting structures as stable, durable systems that need to support arrays while resisting outdoor conditions including wind and corrosion over long service periods.
The exact structural design is determined by the mounting-system engineer, but the manufacturing process still needs to reproduce that design consistently.
A mounting slot positioned several millimeters away from its intended location can affect how components line up during assembly.
This becomes especially important when several brackets produced on different machines or at different times must remain interchangeable.
Hole Accuracy Is More Than One Measurement
When discussing punching accuracy, several different dimensions should be separated.
Hole Size
The actual diameter of a round hole or width and length of a slot.
Local Pitch
The distance between two neighboring holes.
Cumulative Position
The relationship between the first hole and a feature much farther along the profile.
Transverse Position
The distance between the hole and the profile centerline or side edge.
End Distance
The distance between a hole and the final cut end.
Hole-to-Bend Position
The location of a punched feature relative to the finished C-channel or U-channel geometry.
A machine can perform well in one category and still create problems in another.
For example, every adjacent pitch may appear acceptable while the last hole gradually shifts away from the intended position because small feed errors have accumulated across the complete profile.
The Most Important Punching Dimensions
| Measurement | What It Controls | Typical Error Source |
|---|---|---|
| Hole diameter | Fastener fit | Punch/die condition |
| Slot width | Connection compatibility | Tool wear and clearance |
| Slot length | Adjustment range | Tooling condition |
| Hole pitch | Local spacing | Servo feeding |
| Cumulative hole position | Whole-profile alignment | Feed accumulation |
| Transverse position | Centering across profile | Strip tracking |
| End distance | Assembly relationship | Cutting synchronization |
| Hole-to-bend distance | Finished connection geometry | Punching + roll forming |
| Side-hole height | Multi-face assembly | Profile positioning |
A good PV bracket punching machine should therefore be evaluated against the actual finished drawing rather than a single headline accuracy value.
How Servo Feeding Controls Hole Position
Servo feeding is commonly used to position strip before punching.
The production program can define a sequence such as:
feed 100 mm → punch → feed 50 mm → punch → feed 200 mm → punch
The servo motor controls feeder movement according to the programmed command.
This provides much greater flexibility than relying only on fixed mechanical pitch.
However, the motor moving the feeder by a programmed distance does not automatically prove that the steel strip moved by exactly the same distance.
Actual material movement can still be influenced by:
- roller slip,
- feeder pressure,
- coil tension,
- material surface,
- strip thickness,
- acceleration,
- guide resistance,
- and mechanical wear.
For this reason, servo accuracy and finished-hole accuracy are related but should not be treated as identical specifications.
Why Small Feed Errors Can Become Large Problems
Consider a simplified profile containing 40 repeated hole pitches.
If every feed cycle differs slightly from the intended movement and the machine always references the previous position, the error can accumulate.
A very small variation that seems insignificant between two neighboring holes can become more noticeable between:
first hole → last hole
This is why long photovoltaic rails should be evaluated using both local and long-range dimensions.
For example, quality inspection can compare:
- Hole 1 to Hole 2
- Hole 10 to Hole 11
- Hole 1 to Hole 20
- Hole 1 to Hole 40
- Hole 1 to finished cut end
This provides a much clearer picture of whether the process contains cumulative error.
Absolute Referencing vs Repeated Incremental Feeding
One way production systems can reduce cumulative error is by controlling important features from defined references rather than allowing every later position to depend entirely on all previous feed cycles.
The exact control method depends on machine design.
The principle is that critical features should be related to meaningful datum positions such as:
- product start,
- measured material position,
- encoder reference,
- or another verified reference point.
For buyers, this leads to an important question:
How does the machine control cumulative positioning error over a long PV bracket?
Do not accept only an answer about servo-motor resolution.
Ask how the complete material-positioning system is verified.
Encoder Feedback Can Improve Position Monitoring
An encoder can be used to measure movement within the production system.
Depending on the design, it may monitor:
- feeder rotation,
- measuring-wheel movement,
- material travel,
- or downstream profile position.
Encoder information can help the control system compare commanded movement with measured movement.
However, encoder installation itself matters.
For example, a measuring wheel can provide inaccurate information if it:
- slips,
- loses contact,
- becomes contaminated,
- wears,
- or is pressed incorrectly against the strip.
The feedback device should therefore be tested under real material conditions rather than only during no-load commissioning.
Feeder Roller Pressure Must Be Controlled

Servo feeder rollers need enough contact force to move the material consistently.
Too little pressure can allow the strip to slip.
Too much pressure can create other problems, particularly with galvanized or coated materials.
Excessive pressure may contribute to:
- surface marking,
- local deformation,
- roller wear,
- and unnecessary drive load.
If the strip repeatedly slips, increasing pressure should not be the only troubleshooting step.
Operators should also inspect:
- decoiler resistance,
- leveler settings,
- strip loop,
- surface contamination,
- roller condition,
- and acceleration.
Stable feeding depends on the entire entry section.
Coil Tension Can Affect Punching Position
The feeder should position the strip, but upstream equipment can influence how difficult that positioning becomes.
If the servo feeder is continuously pulling strongly against the decoiler or leveler, actual material movement can become less repeatable.
A stable production line should therefore manage material between:
decoiler → leveling → buffer/loop → servo feeding → punching
according to its equipment architecture.
The servo should control positioning rather than fight unpredictable upstream tension during every stroke.
For high-accuracy hole patterns, this relationship becomes especially important.
Strip Tracking Controls Transverse Hole Position
Longitudinal positioning is only one part of hole accuracy.
The strip also needs to remain correctly centered across its width.
If it moves laterally before entering the die, the hole can shift relative to the finished profile centerline.
This can produce:
- unequal edge distance,
- off-center slots,
- incorrect connector position,
- and asymmetric finished brackets.
Entry guides should therefore maintain strip position without forcing the material aggressively against one side.
If the strip continually presses against one guide, operators should check the upstream centerline and coil condition.
Material Width Variation Can Look Like Punching Error
Suppose a hole is punched at a perfectly consistent position relative to the machine centerline.
If incoming strip width changes, the distance from that hole to the material edge also changes.
An inspector measuring from the strip edge may then report a hole-position error.
The punching machine itself may not have moved.
This illustrates why dimensional datums need to be defined clearly.
Manufacturers should specify whether hole position is controlled from:
- strip centerline,
- one reference edge,
- finished profile edge,
- web center,
- or another datum.
Measurement methods need to match the product drawing.
Punch and Die Clearance Affect Hole Quality
Position accuracy becomes meaningless if the hole itself is poorly formed.
Punch and die clearance influences the shearing process.
Unsuitable clearance can contribute to:
- excessive burr,
- poor edge quality,
- accelerated tool wear,
- high punching load,
- and irregular hole geometry.
The appropriate clearance depends on material characteristics and tooling design.
It should therefore be established for the specified:
- steel grade,
- thickness,
- coating,
- and feature geometry.
Changing to a stronger or thicker steel can justify reviewing punching conditions rather than assuming the previous setup remains optimal.
High-Strength Steel Changes Punching Conditions
Photovoltaic bracket manufacturers increasingly need to think beyond material thickness alone.
Two strips with the same nominal thickness can have different mechanical properties.
Higher-strength material generally creates greater demands on punching force and tooling.
The line should therefore be specified using:
material grade + thickness + hole perimeter + number of simultaneous punches
rather than thickness alone.
This becomes particularly important with multi-station systems where several features may be processed during one cycle.
A machine capable of punching one round hole in a given steel does not automatically have the same process margin when several long slots are punched simultaneously.
Long Slots Are More Demanding Than Simple Round Holes
Photovoltaic profiles frequently contain elongated slots because they provide assembly adjustment.
A slot introduces several quality dimensions:
- width,
- length,
- end radius,
- orientation,
- longitudinal position,
- and transverse position.
The larger cutting perimeter can also affect punching load compared with a small round hole.
If slot tooling wears, manufacturers may see:
- larger burr,
- poor slot ends,
- dimensional change,
- or increasing punching force.
When comparing PV bracket punching equipment, provide the real hole and slot drawings rather than only stating the number of punching stations required.
Why More Punching Stations Do Not Automatically Mean Better Equipment
JBLDIE’s Solar Photovoltaic Rack Punching Equipment range includes three-, six-, and nine-station punching configurations for different processing requirements.
The number of stations should follow product complexity.
A three-station machine may be sufficient when a bracket requires a limited set of repeated hole patterns.
More stations become useful when the component contains:
- several hole types,
- different slot groups,
- multiple processing surfaces,
- or more complicated sequences.
Nine stations are not automatically superior to three stations.
Unused stations add equipment complexity without increasing actual production value.
The product drawing should determine the punching architecture.
When Multi-Station Punching Adds Real Value
A multi-station system becomes valuable when different tools can remain installed and ready for several bracket specifications.
This can reduce repeated die changes.
For example, separate stations might be configured for:
- round mounting holes,
- elongated slots,
- connector holes,
- side holes,
- and special project features.
The production recipe can then activate the required operations.
This can support factories that regularly switch between several related PV bracket specifications.
However, buyers should ask whether unused stations create additional material-handling or cycle limitations.
The machine should remain efficient for both simple and complex products.
The Slowest Punching Product Should Be Included in Capacity Planning
A common mistake is to calculate production capacity using the easiest bracket.
Consider two six-meter C-channels.
Channel A
Contains 12 simple holes.
Channel B
Contains 50 holes and slots using several stations.
The forming length is identical.
The punching workload is not.
Channel B may determine the real production bottleneck.
Equipment buyers should therefore identify:
- highest hole count,
- most complex pattern,
- strongest material,
- thickest material,
- and shortest batch size
before estimating practical line output.
Cycle Time Should Be Measured Per Finished Product
Maximum feed speed can be useful, but finished-part cycle time gives a clearer production picture.
A complete punching cycle can include:
- feed,
- deceleration,
- positioning,
- clamping where applicable,
- punch down,
- punch return,
- scrap release,
- next feed.
For complex products, this sequence repeats many times.
The production calculation should use the full sequence rather than the travel speed of the servo axis alone.
Punching Before Roll Forming
Many PV bracket production lines punch flat strip before forming.
This provides several advantages.
The flat material is easy to support.
Punching tools have straightforward access.
Scrap can be removed before the strip reaches the forming rolls.
Servo feeding can also coordinate several different longitudinal patterns.
A typical sequence may be:
decoiling → leveling → servo feeding → punching → roll forming → cutting
This configuration can be particularly efficient for high-volume C- and U-channel production.
However, the final hole position should still be inspected after forming.
Why Forming Can Change the Relationship of Punched Holes
Suppose a slot is punched close to a future bend.
When the strip is later bent:
- the surrounding material moves,
- the surface changes orientation,
- springback occurs,
- and finished profile geometry develops.
The hole may remain exactly where it was punched in the strip, but its relationship with the final C-channel dimensions can change.
This is why finished inspection should measure:
hole position relative to the completed profile
instead of relying only on:
flat strip position before forming.
The closer a hole is to a bend or deformation zone, the more important this becomes.
Post-Punching Uses a Different Reference
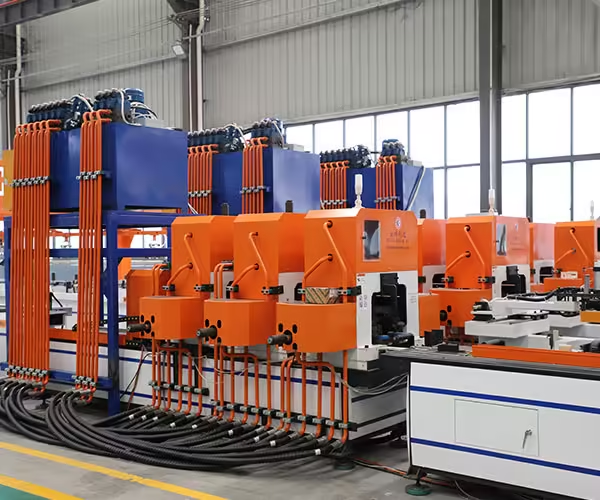
Some photovoltaic components can be punched after they are formed.
This allows the tooling to reference the finished three-dimensional section more directly.
However, it introduces other challenges.
The punch fixture must support the profile without crushing it.
Tool access may be limited by:
- flanges,
- lips,
- deep channels,
- and nearby features.
The best solution depends on the product.
Pre-punching is not automatically better because it is easier.
Post-punching is not automatically better because it references the final section.
The drawings and production volume should determine the sequence.
Side-Hole Punching Requires Stable Profile Positioning
Some brackets contain holes on more than one surface.
For example, a formed C-channel may require:
- web holes,
- flange holes,
- or side connection features.
When punching a formed profile, the machine needs to establish a repeatable three-dimensional position.
A small variation in:
- channel opening,
- flange angle,
- twist,
- or support position
can change where the side punch contacts the profile.
This means forming accuracy and punching accuracy become directly connected.
An unstable upstream profile makes accurate multi-face punching more difficult.
Connector Components Need a Different Punching Strategy
Not every photovoltaic support component is a long rail.
Mounting structures also use smaller:
- connectors,
- brackets,
- plates,
- and joining components.
These parts may require punching, cutting, and bending within a shorter production cycle.
JBLDIE’s photovoltaic bracket equipment portfolio includes connector-processing equipment in addition to long-profile forming systems. Its broader Solar Photovoltaic Bracket Forming Machine category includes both C/U profile equipment and connector-related machinery.
Long profiles and small components should therefore not always share the same production strategy.
Separating these processes can improve line balance when their cycle requirements are very different.
Cutting Synchronization Affects End-Hole Position
Even if every hole is correctly positioned relative to the material, a finished bracket can still fail its drawing if the cutter separates the profile at the wrong position.
Consider a profile requiring:
50 mm from first hole to leading end
50 mm from last hole to trailing end
Hole punching and cutting now share the same dimensional chain.
If the cutter drifts by several millimeters, the hole pattern appears shifted relative to the finished part.
For this reason, end distances should be measured after cutting.
The troubleshooting process should distinguish between:
- incorrect punching,
- incorrect feeding,
- and incorrect cutting.
Encoder and Cutting Reference Should Be Coordinated
Some lines use separate positioning information for punching and cutting.
Others use shared material-position data.
Whichever architecture is selected, the two systems need a consistent dimensional reference.
Otherwise, the hole pattern can remain stable while finished end distance varies.
Commissioning should therefore include several products with known:
- first-hole position,
- last-hole position,
- overall length,
- and cut-end allowance.
This tests whether punching and cutting operate as one coordinated production system.
Preventing Cumulative Hole Error
A practical control strategy can include several layers.
Verify Incoming Material
Check width, thickness, grade, and strip condition.
Stabilize the Entry Section
Avoid excessive upstream tension or uncontrolled strip movement.
Set Feeder Pressure Correctly
Prevent slip without marking or deforming the strip.
Verify Servo Movement
Compare programmed movement against actual finished dimensions.
Use Position Feedback
Monitor material movement using appropriate encoder or measuring systems.
Control Tooling Condition
Prevent punch wear from changing hole dimensions.
Inspect Long-Range Position
Measure first-to-last-hole relationships, not only neighboring pitch.
Coordinate Cutting
Check hole pattern against finished cut ends.
Measure After Forming
Confirm the final bracket rather than only the flat strip.
This multi-stage approach is more reliable than attempting to solve every problem through servo calibration.
A Practical Hole-Accuracy Troubleshooting Table
| Symptom | Possible Cause | First Check |
|---|---|---|
| Every hole shifted equally | Incorrect datum or starting position | Product zero/reference |
| Pitch varies randomly | Strip slip or feeder instability | Servo feeder and tension |
| Error increases along profile | Cumulative feed error | Long-range feed measurement |
| Holes shift sideways | Strip tracking | Guides and centerline |
| Hole size changes | Punch/die wear | Tooling condition |
| Burr increases | Clearance or tool wear | Punch and die |
| Slot distorted after forming | Too close to bend | Finished-profile inspection |
| First hole correct, last hole wrong | Feed accumulation | Encoder/reference logic |
| Hole pattern correct, end distance wrong | Cutting error | Cutter synchronization |
| Side holes vary | Profile position unstable | Forming and fixture |
| Error starts after coil change | Material/feeding condition | New coil specification |
How to Troubleshoot Cumulative Error
When the last holes of a profile drift but the first hole remains correct, do not immediately adjust the die.
The die determines hole shape.
The problem is more likely related to material positioning.
Begin by producing several parts using the same program.
Measure the error at several locations:
- 500 mm,
- 1,000 mm,
- 2,000 mm,
- 4,000 mm,
- and final position.
If error increases consistently with length, investigate:
- servo calibration,
- measuring-wheel condition,
- feeder slip,
- encoder feedback,
- and control-reference logic.
If the error appears randomly rather than progressively, inspect material movement and mechanical stability.
Repeatability and Accuracy Are Not the Same
A machine can be repeatable but inaccurate.
For example, every finished profile may place the first slot exactly 3 mm away from the intended position.
That is a calibration or reference issue.
A machine can also be accurate on average but poorly repeatable.
One profile may be +2 mm, the next -2 mm, and the next +1 mm.
That suggests process instability.
Equipment acceptance should therefore evaluate both:
accuracy
How close the mean result is to the target.
and
repeatability
How consistently multiple parts reproduce the same result.
A single perfect sample cannot demonstrate repeatability.
Several Consecutive Profiles Should Be Measured
During FAT or commissioning, do not inspect only one bracket.
Produce several consecutive finished components.
Measure:
- first-hole position,
- selected internal pitches,
- final-hole position,
- end distance,
- cut length,
- transverse position,
- and relevant profile dimensions.
If all parts show nearly the same deviation, calibration may be needed.
If deviations vary significantly between parts, process stability should be investigated.
This distinction saves time during troubleshooting.
FAT Should Use the Real Hole Pattern
A punching machine can look impressive when repeatedly punching one simple hole.
That test provides limited information if the buyer’s actual product contains:
- several long slots,
- multiple hole diameters,
- side holes,
- and different spacing.
A meaningful Factory Acceptance Test should use a representative product drawing.
Buyers should provide one of the more demanding patterns rather than the easiest one.
The test should verify:
- punching sequence,
- material feeding,
- hole quality,
- cumulative position,
- production cycle,
- and finished-part repeatability.
What Buyers Should Ask During FAT
Useful questions include:
- What is the material grade used during the test?
- Is the thickness representative of normal production?
- Are actual slots and hole groups being punched?
- How is the first material position established?
- How is cumulative error monitored?
- What device measures actual material movement?
- How many consecutive profiles will be inspected?
- How is hole position measured?
- How is cut-end position synchronized?
- What happens after a product recipe change?
These questions provide more useful information than watching the machine complete a short demonstration cycle.
Three, Six, or Nine Stations: Start With the Drawing
PV bracket punching equipment is often compared by the number of stations.
A better selection method begins with the hole matrix.
List every required feature:
| Feature | Product A | Product B | Product C |
|---|---|---|---|
| Round web hole | ✓ | ✓ | ✓ |
| Long web slot | ✓ | ✓ | ✓ |
| Side hole | ✓ | ✓ | |
| Large connector hole | ✓ | ||
| Alternative slot | ✓ | ✓ | |
| Special project feature | ✓ |
Then determine which tools need to remain installed simultaneously.
A three-station system may be enough for the first product family.
More stations become useful as the feature matrix expands.
The machine configuration should follow production needs rather than the idea that the largest station count is automatically the most advanced.
More Stations Can Improve Changeover Flexibility
The strongest reason for additional stations is often not raw punching speed.
It can be tooling availability.
If several dies remain mounted on separate stations, the machine may switch between products through:
- program selection,
- feeding changes,
- station activation,
- and limited mechanical adjustment
rather than removing and reinstalling dies every time.
This becomes valuable for factories serving multiple solar projects with shorter production batches.
The real benefit should therefore be measured through:
last qualified Product A → first qualified Product B
not simply by counting hydraulic cylinders.
Current PV Market Growth Increases the Value of Flexibility
IEA PVPS reported that global PV capacity approached 3 TW by the end of 2025, while deployment continued spreading across a wider number of national markets.
This does not mean every bracket manufacturer automatically needs maximum equipment flexibility.
Dedicated lines can remain highly efficient for stable high-volume products.
However, manufacturers supplying several projects or export markets may need to manage more:
- profile types,
- connection patterns,
- slot dimensions,
- finished lengths,
- and material specifications.
For these factories, programmable punching and repeatable changeover become strategically more important than maximum station count alone.
Punching Accuracy and Galvanized Surface Protection
Many photovoltaic support profiles use galvanized steel.
Punching breaks through the coated sheet and creates a new cut edge.
At the same time, feeding and clamping can mark the broad coated surface if they are not controlled properly.
The U.S. Department of Energy notes that steel and other metal components in PV racking systems can be exposed to corrosion and that material combinations and protective systems need to be considered carefully in harsh environments.
From a manufacturing perspective, the punching line should therefore avoid unnecessary coating damage around areas unrelated to the intended cut.
Check:
- feeder rollers,
- clamps,
- guides,
- support tables,
- scrap,
- and finished-product handling.
Punching accuracy and surface quality should be inspected together.
Scrap Removal Can Affect Reliability
Every punching operation produces material that needs to leave the tool safely.
Slugs and scrap that remain around the die can create:
- tool jams,
- surface marks,
- double punching,
- sensor alarms,
- or tooling damage.
High-hole-density PV profiles generate more scrap over the same profile length.
Scrap management should therefore be considered during equipment selection.
Ask:
- Where do slugs go?
- How are they discharged?
- Can scrap accumulate inside the machine?
- Is the area easy to clean?
- Can sensors detect an abnormal tool condition?
A reliable punching system needs an equally reliable waste path.
Tool Maintenance Should Be Based on Product Quality
Punches and dies are wearing components.
Maintenance should not wait until a tool breaks completely.
Finished parts often show early signs of deterioration.
Useful indicators include:
- increasing burr,
- changing slot dimensions,
- rough edges,
- greater punching noise,
- rising load,
- incomplete slug release,
- or more frequent jams.
Production teams can record tool cycles and inspection results.
This helps connect preventive maintenance with actual component quality.
Recipe Management for Multiple PV Brackets
A programmable punching system can store different product recipes.
A recipe may contain:
- first-hole location,
- hole sequence,
- pitch,
- active stations,
- cut length,
- product quantity,
- and other production settings.
This can reduce manual re-entry when repeat products return.
However, a stored recipe should not automatically be trusted after:
- tooling replacement,
- feeder maintenance,
- encoder change,
- material change,
- or major machine adjustment.
A first-piece check remains necessary.
Digital repeatability depends on mechanical repeatability.
Traceability Can Help Diagnose Hole Problems
Factories serving demanding projects may benefit from connecting production records with material and machine information.
A useful production record can contain:
- coil number,
- material grade,
- thickness,
- product recipe,
- punching-tool set,
- production date,
- dimensional inspection,
- and machine alarms.
Suppose cumulative hole error begins during one shift.
The records can help determine whether the issue coincided with:
- a new coil,
- tool maintenance,
- recipe change,
- feeder adjustment,
- or another event.
Data becomes useful when it supports troubleshooting rather than simply increasing the number of values displayed on an HMI.
How to Evaluate a PV Bracket Punching Machine
Before equipment selection, buyers should prepare complete product drawings.
Then ask the supplier to explain the production process around those drawings.
Important questions include:
- How many unique hole types are required?
- Which holes can be punched simultaneously?
- Which stations remain installed during changeover?
- How is material position measured?
- How is cumulative feed error controlled?
- How is lateral strip movement controlled?
- What material grade is included in the machine calculation?
- How does punching force change with stronger steel?
- How are slots and round holes inspected?
- How is punching coordinated with cutting?
- How is final hole-to-bend position verified?
- How is scrap removed?
- How are tools maintained?
- What representative product will be used during FAT?
The quality of these answers is more important than a single advertised precision figure.
What Information Should Be Provided Before Machine Configuration?
A complete technical package should include:
Material
Provide:
- steel grade,
- yield strength where relevant,
- thickness,
- strip width,
- coating,
- coil size.
Hole Drawing
Provide:
- round-hole diameters,
- slot dimensions,
- hole groups,
- longitudinal positions,
- transverse positions,
- side holes,
- tolerances.
Finished Profile
Provide:
- C/U/Z profile geometry,
- bends,
- lips,
- finished width,
- finished length.
Production
Provide:
- annual volume,
- common batch size,
- changeover frequency,
- required cycle time,
- expected product mix.
Quality
Define:
- local pitch tolerance,
- cumulative positioning requirement,
- end distance,
- hole size,
- burr requirement,
- and surface expectations.
This allows the punching system to be engineered around actual production instead of a generic station count.
A Practical Buyer Acceptance Checklist
Before approving a PV bracket punching machine, verify:
Material Feeding
The strip moves consistently without visible slip or uncontrolled lateral movement.
Hole Quality
Round holes and slots meet the required shape and edge condition.
Local Pitch
Adjacent features remain within the agreed requirement.
Cumulative Position
Long-range hole location remains stable.
Transverse Position
Features remain correctly centered relative to the reference datum.
Finished Profile Position
Punched features remain correct after roll forming.
End Distance
The cutter separates the profile at the intended position.
Repeatability
Several consecutive products show consistent results.
Changeover
Stored recipes and tooling changes reproduce the next product correctly.
Surface Quality
Feeders, guides, and tooling do not create unnecessary coating damage.
Scrap Removal
Punching waste leaves the tool reliably.
Fault Diagnostics
Operators can identify feeder, punch, sensor, and positioning errors clearly.
Conclusion
A PV bracket punching machine should be evaluated as a complete positioning and processing system rather than simply a hydraulic press with several dies.
Accurate holes depend on the relationship between servo feeding, strip tracking, material tension, encoder feedback, tooling condition, punching sequence, material properties, roll forming, and final cutting.
For long photovoltaic support profiles, cumulative error deserves particular attention.
A machine may produce acceptable local hole pitch while still allowing the final holes to drift relative to the beginning of the profile. Buyers should therefore measure both short-range and long-range dimensions during machine acceptance.
The number of punching stations should also be selected from the actual product matrix. Three, six, or nine stations only create value when the installed tools correspond with the bracket family’s real hole patterns and reduce practical changeover work.
As PV deployment continues expanding into more markets, manufacturers serving several projects may increasingly benefit from programmable feeding, flexible station configuration, stored recipes, repeatable changeover, and stronger production traceability.
The best equipment selection begins with the finished bracket drawing—not with a machine specification sheet.
FAQ
What is a PV bracket punching machine?
A PV bracket punching machine is equipment used to create round holes, slots, connector openings, and other features in photovoltaic mounting components. It can work with flat strip, formed profiles, or integrated roll forming production lines.
What causes cumulative hole-position error in PV brackets?
Possible causes include servo-feed calibration, strip slip, encoder error, unstable feeder pressure, upstream tension, mechanical wear, or control-reference problems. Long-range measurements are needed to distinguish cumulative error from local pitch variation.
Is a nine-station punching machine better than a three-station machine?
Not automatically. The correct station count depends on the number of hole types, processing surfaces, product variations, and changeover requirements. A simpler product may not benefit from unused stations.
Should PV bracket holes be punched before or after roll forming?
Both approaches are possible. Pre-punching provides easier tool access, while post-punching can reference finished profile geometry more directly. The correct sequence depends on hole location, profile shape, tolerance, volume, and tooling access.
What should buyers test during PV bracket punching machine FAT?
Buyers should test representative material and actual hole patterns while checking hole dimensions, local pitch, cumulative position, transverse location, cut-end distance, production cycle, repeatability, and changeover performance.
Need to Configure PV Bracket Punching Equipment?
The punching system should be developed from your actual bracket profile, material grade, thickness, round holes, slots, side features, cumulative positioning requirements, production volume, and changeover needs. Contact JBLDIE to discuss your photovoltaic bracket drawings and punching requirements.
 English
 Arabic
 Russian
 Spanish
 French