
Как управление ЧПУ улучшает линии обработки металлов
Оглавление
A modern metal processing line is no longer controlled only by motors, switches and mechanical adjustments. As factories handle more product specifications, shorter production batches and tighter dimensional requirements, the control system increasingly determines how efficiently different machines work together.
A CNC control system can coordinate feeding distance, punching position, cutting length, product quantity, servo movement and other programmable operations. In an integrated line, it may also exchange signals with roll forming equipment, hydraulic systems, material handling devices and downstream automation.
The result is not simply a machine that “runs automatically.” The real value comes from turning a series of separate mechanical actions into a repeatable production process.
This is particularly relevant to Jinbolida’s smart manufacturing applications, which include CNC feed control lines, multi-station punching equipment, automated loading and unloading, cutting systems and other production equipment used in photovoltaic, construction, power, transportation and metal-processing industries.
Что такое система управления ЧПУ?
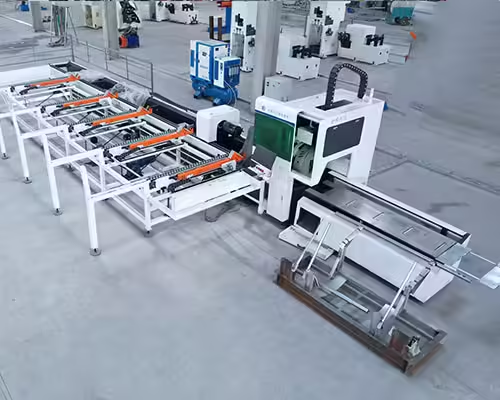
CNC stands for Computer Numerical Control.
A CNC control system interprets programmed production instructions and converts them into commands for machine movements and operations.
Depending on the equipment, the system may control:
- Servo feeding distance
- Axis position
- Последовательность перфорации
- Расстояние между отверстиями
- Длина резки
- Product quantity
- Motor speed
- Tool position
- Перенос материала
- Автоматическая разгрузка
- Выбор рецепта
In a standalone machine, CNC may control one primary operation.
In an automated production line, the control architecture may coordinate several machines and processes.
Например:
Material Feeding → Positioning → Punching → Forming → Cutting → Unloading
The control system needs to know when each operation should start, when it should stop and how each machine responds to the process before and after it.
ЧПУ отличается от простой автоматизации
Automation and CNC control are related, but they are not exactly the same thing.
A machine can be automated without having sophisticated numerical control.
For example, a basic machine may:
- Detect a part
- Activate a cylinder
- Complete one fixed operation
- Return to its starting position
That is automation.
A CNC-controlled system can additionally use numerical instructions to determine:
- Position
- Distance
- Скорость
- Sequence
- Product model
- Quantity
This flexibility makes CNC particularly useful when the same production line needs to manufacture multiple specifications.
The value increases further when the system can store production recipes.
Почему управление ЧПУ имеет значение при обработке металлов
Metal processing often requires multiple dimensions to remain coordinated.
Consider a steel profile containing several slots.
The manufacturer may need to control:
- Положение первой лунки
- Расстояние между отверстиями
- Количество отверстий
- Overall profile length
- Cutting location
If every value is manually measured and adjusted, production becomes increasingly dependent on operator experience.
A CNC control system allows those values to be entered as numerical production parameters.
This does not eliminate the importance of mechanical accuracy, tooling condition or quality inspection.
It does, however, make repeatable positioning easier to manage.
Управление ЧПУ и подача сервоприводов
One of the most important applications of CNC control in metal processing is servo feeding.
The process can be simplified as:
Programmed Distance → Servo Command → Material Movement → Position Confirmation → Processing
Suppose a profile requires holes at:
- 100 mm
- 350 mm
- 600 mm
- 850 mm
Instead of manually repositioning the material, the control system instructs the servo feeder to move the programmed distances.
This is particularly useful for products with:
- Unequal hole spacing
- Several lengths
- Multiple customer specifications
- Short production batches
Jinbolida identifies CNC feed control lines among the equipment used across several of its industrial smart manufacturing solutions.
Управление ЧПУ при автоматической штамповке
Punching provides a good example of why programmable control matters.
A simple product may need the same hole every fixed distance.
A more complicated component can require:
- Круглые отверстия
- Слоты
- Different station combinations
- Unequal spacing
- Several punched surfaces
In such applications, the CNC system can coordinate the feeding movement with individual punching stations.
Джинболида фотоэлектрическое оборудование для штамповки стоек includes multi-station punching configurations intended for products requiring different hole combinations and processing sequences.
The control logic becomes especially important when several stations share one material feed.
Одна программа может представлять один рецепт продукта
A major advantage of programmable control is recipe storage.
Instead of manually entering all settings before every production batch, operators may select a saved product program.
A recipe can contain parameters such as:
| Параметр | Example Control Function |
|---|---|
| Длина продукта | Determines cut position |
| Расстояние между отверстиями | Controls servo feed |
| Hole quantity | Determines punching cycles |
| Product quantity | Controls batch count |
| Profile specification | Selects related settings |
| Axis position | Controls automatic adjustment |
| Скорость производства | Sets operating parameters |
This can reduce the amount of manual setup required between batches.
It also makes standardized production procedures easier to maintain.
Более быстрые переключения часто более ценны, чем более высокая скорость
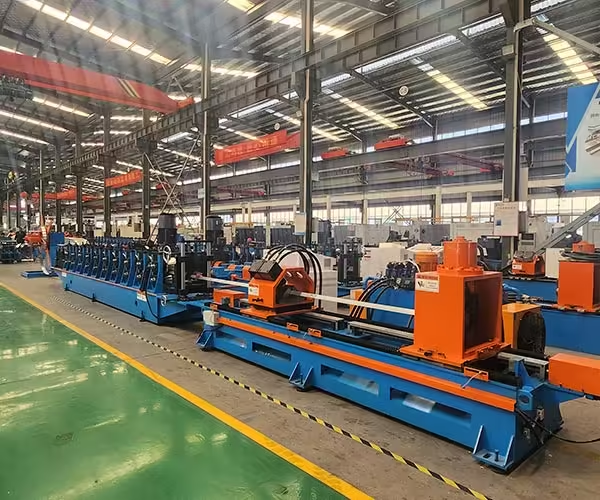
Factories frequently compare equipment using maximum production speed.
But a machine producing several product specifications may lose more time during changeovers than during normal operation.
Consider two production systems.
Система А
- Maximum speed: 35 m/min
- Changeover: 75 minutes
Система Б
- Maximum speed: 30 m/min
- Changeover: 15 minutes
If the factory changes products several times per shift, System B may produce more saleable output over the full working day despite having a lower maximum speed.
CNC recipe management can contribute to faster changeover when adjustable parameters can be recalled automatically.
However, software cannot eliminate mechanical tooling changes that are physically required.
The correct evaluation should therefore separate:
Digital changeover time
из
Mechanical changeover time.
ЧПУ не может исправить плохую механическую конструкцию
This is one of the most important points when evaluating automated equipment.
A sophisticated controller cannot fully compensate for:
- Worn rollers
- Misaligned shafts
- Incorrect tooling
- Механическая люфта
- Loose bearings
- Unstable material
- Weak machine structures
For example, if a servo feeder moves accurately by 500 mm but the strip slips inside the feeding rollers, the finished hole position can still be wrong.
Likewise, a controller may set the correct cutting command, but mechanical movement in the cutting assembly can affect actual results.
CNC accuracy therefore needs to be supported by:
Mechanical accuracy + Sensor feedback + Correct tooling + Stable material handling
Обратная связь с закрытым контуром улучшает управление
More advanced systems use feedback to confirm whether the commanded action occurred.
Possible feedback devices include:
- Кодеры
- Датчики приближения
- Фотоэлектрические датчики
- Ограничительные переключатели
- Pressure sensors
The basic control concept is:
Command → Movement → Measurement → Comparison → Correction
This differs from a system that simply sends a command and assumes the movement has been completed correctly.
Closed-loop control can be particularly important for servo motion and automated material positioning.
Точность управления движением и позиционирования с ЧПУ
A CNC motion control system coordinates one or more controlled axes.
Examples can include:
- Servo feeder axis
- Width adjustment
- Tool positioning
- Перенос материала
- Loading system
- Cutting carriage
The controller calculates the required movement and sends commands to the servo drive.
Positioning performance depends on the complete motion system:
- Controller
- Серводвигатель
- Drive
- Encoder
- Трансмиссия
- Mechanical structure
It is therefore misleading to evaluate positioning accuracy only from the controller specification.
The mechanical transmission must be capable of reproducing the commanded motion.
Повторяемость может иметь значение больше, чем одноразовая точность
A machine may hit the correct position once during testing.
Industrial manufacturing requires it to repeat that position hundreds or thousands of times.
This distinction is important.
Точность
How close the machine reaches the target position.
Повторяемость
How consistently it returns to the same position.
For high-volume metal processing, repeatability is often critical because variation accumulates across large production batches.
A reliable CNC control system should therefore be evaluated under continuous production conditions rather than only through one successful trial piece.
Управление ЧПУ на производственных линиях профилегибочного производства
A roll forming machine continuously transforms coil material through multiple forming stations.
The CNC system may not directly control the roller geometry, but it can coordinate many surrounding operations.
These can include:
- Кормление
- Штамповка
- Длина продукта
- Резка
- Подсчет
- Adjustable profile settings
- Production alarms
Джинболида Сталеформовочные машины W, L и Z-образной формы combine continuous forming with PLC-based control and can integrate punching, welding, stacking and unloading functions according to the application.
The controller therefore becomes the communication layer between several mechanical processes.
ЧПУ-контроль в строительном формовочном оборудо
Construction profile production often involves multiple product sizes.
Примеры включают:
- C profiles
- U profiles
- Z profiles
- Кровельные панели
- Steel formwork components
The construction forming machine range uses PLC and HMI control for production monitoring and adjustment.
For factories producing several specifications, stored settings can reduce the number of parameters an operator needs to reset manually.
This becomes especially valuable when products change frequently.
Точность управления ЧПУ и длины резки
Cutting is another area where control performance matters.
The system needs to know:
- Current material position
- Required finished length
- Cutting delay
- Machine speed
Depending on the cutting method, it may need to:
- Stop the line
- Trigger a hydraulic cutter
- Synchronize a moving cutting carriage
- Confirm the cut
- Restart production
If the timing between measurement and cutting is poorly coordinated, finished length can vary.
Therefore, cutting accuracy depends on more than the cutter blade itself.
Measurement and control logic are also important.
Управление ЧПУ в лазерной резке
Laser cutting is another strong application of CNC technology.
The controller converts a digital cutting path into coordinated machine-axis movement.
For industrial applications, this enables:
- Complex geometry
- Repeated components
- Different product programs
- Automated nesting
- Consistent tool paths
Jinbolida also provides laser metal cutting equipment for sheet and tube-processing applications.
Unlike fixed mechanical tooling, CNC laser processing can switch geometry primarily through programming, making it useful for flexible manufacturing.
Почему управление ЧПУ поддерживает гибкое производство
Traditional dedicated equipment is highly efficient when it produces one product for long periods.
Modern contract manufacturing often faces a different environment:
- Smaller batch sizes
- More product variants
- Shorter delivery schedules
- Frequent design changes
A programmable control system allows more product information to be changed digitally rather than mechanically.
This does not make every machine universal.
But it can reduce dependence on fixed setup procedures.
This is one of the foundations of flexible manufacturing.
Управление ЧПУ и интеллектуальное производство
Modern manufacturing increasingly connects machine controls with higher-level production information.
The U.S. National Institute of Standards and Technology discusses smart manufacturing as an environment involving advanced sensing, data management, automation and integrated control. NIST’s recent smart manufacturing research also emphasizes the importance of integrating industrial sensing and control systems with reliable data infrastructure.
At the machine level, CNC and PLC systems can provide production data such as:
- Part count
- Running status
- История тревоги
- Время производства
- Recipe
- Energy data
- Machine utilization
This information can support broader factory management when properly integrated.
Подсчет производства уменьшает ручную запись
A simple but useful CNC function is automatic quantity counting.
The operator can enter:
Required Quantity: 2,000 pieces
The system then counts completed products.
After the target is reached, it may:
- Остановить автоматически
- Generate an alarm
- Wait for the next batch
This reduces dependence on manual counting and helps prevent unnecessary overproduction.
For high-volume factories, even simple counting functions can improve order control.
Группы по техническому обслуживанию справки по записям тревог
When a machine stops, the maintenance team needs to know why.
A basic alarm may show:
Machine Fault
A better system can identify:
- Servo alarm
- Hydraulic pressure low
- Sensor not detected
- Material feed error
- Safety guard open
- Cutting cycle incomplete
Historical alarm data can help technicians identify repeated faults.
For example, if the same sensor alarm appears every day, the problem may require more than resetting the system.
Alarm history turns machine stoppage into information that can be analyzed.
Производственные данные могут выявить скрытый простой
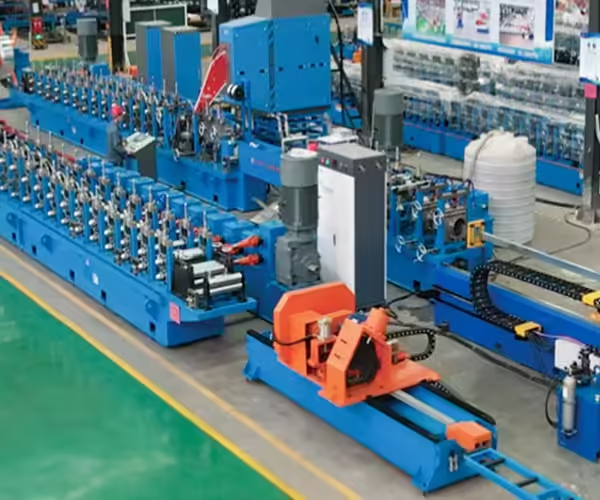
A factory may believe that a machine runs for eight hours because the operator is assigned to it for eight hours.
The actual productive time may be much lower.
Production records can reveal:
- Running time
- Время простоя
- Alarm time
- Setup time
- Количество продукции
This makes it easier to distinguish between:
Machine speed
и
Effective manufacturing output.
A machine capable of very high speed provides little value if it spends a large part of each shift waiting for material or setup.
Управление ЧПУ помогает стандартизировать операционные процедуры
Without stored programs, experienced operators may develop their own machine settings.
That can create variation between:
- Day shift
- Night shift
- Experienced operators
- New operators
Recipe-based control allows approved production parameters to be stored.
Operators can then select a validated program rather than rebuilding settings from memory.
This supports process standardization.
However, companies should still control who can modify critical parameters.
Уровни разрешений пользователя могут защитить критические настройки
Industrial HMI systems can support different access levels.
Например:
Оператор
Can:
- Start production
- Stop production
- Select approved recipes
Супервайзер
Can:
- Edit production quantities
- Modify selected process parameters
Инженер
Can:
- Modify machine configuration
- Access advanced settings
This prevents accidental changes to important control values.
It also supports more structured machine management.
Автоматическое управление по-прежнему требует правильной конструкции безопасности
Automation can reduce the need for operators to enter hazardous processing areas, but it does not eliminate machine hazards.
OSHA states that machine parts, functions or processes capable of causing injury must be safeguarded. Its machine guarding guidance covers hazards from rotating parts, points of operation and mechanical motion.
OSHA also notes that automatic feeding can reduce the need for operators to enter danger areas, while additional guarding remains necessary. Its machine safety guidance on feeding and ejection explains the role of automatic feeding in reducing operator exposure.
For CNC-controlled equipment, safety design may include:
- Аварийные остановки
- Фиксированные охранники
- Сблокированные двери
- Световые шторы
- Safety relays
- Safe-stop circuits
Control automation and safety systems should be designed together.
Предохранительные блокировки не следует рассматривать как обычные датчики
An ordinary production sensor detects whether a component is present.
A safety interlock performs a different function.
If a protected machine door is opened, the system may need to stop hazardous motion.
OSHA describes interlocked machine guards as safeguards that stop or disengage hazardous movement when the guard is opened and prevent operation until the guard is restored.
The control architecture should therefore distinguish normal production logic from safety-related logic.
Почему дизайн HMI имеет значение
The HMI is the interface between the operator and control system.
A good interface should help operators understand:
- Current product
- Необходимое количество
- Completed quantity
- Machine status
- Alarm condition
- Key production parameters
A poorly designed interface can make an advanced machine unnecessarily difficult to operate.
Good HMI design should prioritize clarity rather than filling every screen with technical values.
The operator should be able to quickly identify:
What is the machine doing?
What product is running?
Why has it stopped?
Многоязычные интерфейсы имеют значение для экспортного оборудования
International production equipment may be installed in different countries.
An appropriate HMI can support:
- English
- Local languages
- Standard symbols
- Clear alarm descriptions
This reduces dependence on translation during daily operation.
For exported equipment, language support should be confirmed during the technical specification stage rather than requested after software development is complete.
Удаленная диагностика может сократить время устранения неполадок
Some modern control systems can support remote diagnostic access.
This may allow technical personnel to inspect:
- Alarm status
- PLC conditions
- Неисправности сервоприводов
- Production parameters
Remote diagnostics can be particularly useful for international equipment because not every software issue requires an engineer to travel to the factory.
However, remote access should be implemented with appropriate cybersecurity and permission controls.
Machine connectivity should never be treated as unlimited public access.
Подключение к данным создает новые требования
As machines become connected, manufacturers should consider:
- Network architecture
- Разрешения пользователя
- Резервные процедуры
- Software version control
- Cybersecurity
Connecting every machine to a network without a management plan can create new risks.
Production equipment should maintain reliable local control even while exchanging useful manufacturing information with higher-level systems.
Резервное копирование имеет решающее значение для оборудования, управляемого ЧПУ
The control program is an important machine asset.
Factories should maintain backups of:
- PLC program
- CNC parameters
- HMI project
- Servo settings
- Product recipes
Without backups, replacing a failed controller or storage device can become much more complicated.
A proper equipment handover should therefore include confirmation of:
- Backup method
- Password management
- Program ownership
- Parameter records
This issue is often overlooked during equipment purchasing.
контроль ЧПУ не устраняет необходимости проверки качества
Automation can improve consistency, but the finished product still needs to be checked.
Quality inspection may include:
- Длина
- Положение отверстия
- Размеры профиля
- Прямолинейность
- Качество поверхности
The CNC system controls machine instructions.
Inspection confirms whether the process actually produced the intended result.
The two functions complement each other.
Проверка первой статьи по-прежнему важна
Whenever a product recipe changes, the first finished part should normally be verified before full-volume production begins.
A first-article check can confirm:
- Correct program selected
- Correct material loaded
- Позиции отверстий
- Длина разреза
- Размеры профиля
This prevents a programming or setup mistake from being repeated across an entire production batch.
Automation makes production fast.
That also means an incorrect program can produce scrap quickly.
Как контроль ЧПУ снижает измерения человеком
Manual production can require an operator to repeatedly:
- Measure material
- Mark hole positions
- Reposition the workpiece
- Count finished products
CNC automation moves more of these repetitive positioning tasks into programmed control.
The operator’s role then shifts toward:
- Loading material
- Selecting programs
- Monitoring production
- Performing quality checks
- Responding to alarms
This can improve efficiency while also making operator training more focused.
Управление ЧПУ и обращение с материалами
The value of programmable control increases when processing equipment is connected to automated material handling.
A production cell might include:
Feed → Process → Transfer → Flip → Stack
Sensors and controllers coordinate whether each stage is ready to receive the next part.
Jinbolida’s smart manufacturing applications include automated loading and unloading workstations, CNC material transfer systems and robotic processing cells across several industries.
This connects naturally with broader metal processing automation solutions вместо того, чтобы рассматривать каждую машину как изолированную рабочую станцию.
Когда управление ЧПУ обеспечивает наибольшую ценность
CNC control is particularly useful when:
- Hole positions vary
- Product lengths vary
- Several SKUs share one machine
- Changeovers occur frequently
- Tight positioning repeatability is required
- Production quantities need tracking
- Multiple machines must operate together
- Manufacturing data is required
The value is lower when a machine performs only one fixed operation with virtually no variation.
The control level should therefore match the manufacturing problem.
Не переусердствуйте с простым процессом
More control functions mean:
- More programming
- More electrical components
- More sensors
- More maintenance skills
- Более высокие первоначальные инвестиции
A factory producing one fixed part continuously may not benefit from every available CNC feature.
The correct question is:
Which control functions reduce measurable production cost or risk?
Not:
How many automated features can be added?
Вопросы, которые следует задавать при покупке оборудования, управляемого ЧПУ
Before purchasing a machine or production line, ask:
- Which operations are CNC controlled?
- Which operations still require manual adjustment?
- How many product recipes can be stored?
- Which servo axes are included?
- How is position feedback measured?
- Which controller platform is used?
- Are replacement components available locally?
- Can production data be exported?
- Are alarm records stored?
- Is remote diagnosis available?
- Which user permission levels are supported?
- Which safety functions are independent of normal control?
- Are PLC and HMI backups provided?
- Can future production programs be added?
- What training is included?
These questions reveal much more than simply asking whether the machine has “CNC.”
Контрольный список выбора системы управления ЧПУ
| Требование | What to Confirm |
| Разнообразие продуктов | Number of recipes required |
| Позиционирование | Required tolerance and repeatability |
| Motion axes | Number of servo-controlled movements |
| Штамповка | Station and sequence control |
| Резка | Length measurement and synchronization |
| Данные производства | Counting and history |
| HMI | Language and usability |
| Сигнализации | Fault identification and records |
| Безопасность | Guard and emergency-stop integration |
| Connectivity | Data interface requirements |
| Обслуживание | Backup and diagnostic access |
| Expansion | Future products and equipment |
The control specification should be developed together with the mechanical machine specification.
Распространенные ошибки управления ЧПУ
Выбор контроллера перед определением процесса
Control architecture should follow actual machine functions.
Предполагая, что ЧПУ автоматически означает высокую точность
Mechanical accuracy remains essential.
Игнорирование удобства использования оператором
A powerful system can still reduce productivity if the HMI is difficult to operate.
Забывание резервных копий программ
Control programs and machine parameters should be protected as production assets.
Смешивание логики безопасности и обычного управления
Safety-related functions need appropriate hardware and engineering.
Покупка функций, которые никогда не будут использоваться
Automation should solve defined production problems.
Игнорирование будущих рецептов продуктов
Factories expecting more SKUs should consider expansion during initial design.
Часто задаваемые вопросы
Что такое система управления ЧПУ?
A CNC control system uses programmed numerical instructions to control machine position, movement and production operations such as feeding, punching or cutting.
ЧПУ то же самое, что ПЛК?
No. A PLC primarily controls machine logic and sequence, while CNC specializes in numerical motion and machining commands. Many industrial machines use both functions together.
Что такое управление движением ЧПУ?
CNC motion control coordinates servo-driven axes to move to programmed positions, distances or speeds.
Может ли ЧПУ повысить точность штамповки?
It can improve programmable material positioning when combined with an appropriate servo feed and mechanically stable punching system.
Does CNC make a machine fully automatic?
Not necessarily. Full automation also depends on material loading, processing, unloading and other operations.
Can one CNC machine store different products?
Yes. Many control systems support multiple product recipes containing information such as lengths, hole positions and quantities.
Does CNC reduce changeover time?
It can reduce the digital setup portion of changeover by recalling saved parameters. Mechanical tooling changes may still be required.
Can CNC control be integrated with roll forming?
Yes. CNC or PLC-based systems can coordinate feeding, punching, cutting and other operations around the roll forming process.
Why is feedback important in CNC motion control?
Feedback devices such as encoders confirm actual movement and allow the system to compare commanded and measured position.
Is CNC control useful for smart manufacturing?
Yes. CNC and PLC systems can provide machine status, production counts, alarms and other data that can be integrated into broader manufacturing systems.
Заключение
A CNC control system is most valuable when it solves a real manufacturing problem: accurate positioning, frequent product changes, coordinated machine movement or better production visibility.
Its role extends beyond simply replacing manual buttons with a touchscreen.
In a well-designed metal processing line, CNC control can coordinate servo feeding, punching, cutting, product recipes, quantity counting and machine communication. When connected with mechanical equipment and appropriate sensors, it helps transform separate operations into a repeatable production process.
However, sophisticated software cannot compensate for poor tooling, unstable material handling or weak machine construction. The best results come from combining reliable mechanical engineering with appropriate motion control, feedback, safety systems and operator-friendly interfaces.
Manufacturers evaluating automation can explore Jinbolida’s smart manufacturing industry solutions, W, L and Z-shaped steel forming equipment, construction profile forming machines и автоматические системы пробивки to understand how CNC and PLC control can be integrated into different metal-processing applications.
For a customized system, prepare your product drawings, material specifications, required processing sequence, positioning tolerance, production capacity and automation requirements, then свяжитесь с Джинболидой to evaluate the control system together with the complete production line.
 Russian
 English
 Arabic
 Spanish
 French