
Что упрощает сборку кронштейнов для крепления фотоэлектрических панелей?
Оглавление
PV panel mounting brackets may look like simple metal components, but small manufacturing variations can create significant installation problems. Incorrect hole spacing, profile twist, uneven flange dimensions or distorted cut ends can prevent rails, posts, connectors and fasteners from aligning correctly.
A mounting bracket that is easy to assemble is not defined only by its appearance. It must consistently match the approved drawing, fit related components and maintain the required geometry along its full length.
The manufacturing factors that have the greatest influence on assembly include:
- Consistent cross-sectional dimensions
- Accurate hole and slot positions
- Controlled straightness and twist
- Stable bend angles
- Repeatable cut length
- Clean punched and cut edges
- Protected coating surfaces
- Compatibility with connectors and fasteners
- Reliable production traceability
For manufacturers, assembly performance should be considered when selecting roll forming, punching, cutting and inspection equipment. The objective is not simply to produce a profile that looks correct. It is to produce components that connect without unnecessary force, drilling, trimming or field adjustment.
Как работают кронштейны для крепления фотоэлектрических панелей
PV panel mounting brackets form part of the structure that positions and supports solar modules. Depending on the system design, they may connect modules to rails, rails to posts, profiles to roofs or structural members to foundations.
А photovoltaic mounting system may be installed on rooftops, ground structures, building façades or tracking systems. Each application uses a different combination of rails, brackets, clamps, posts, fasteners and connectors.
The U.S. Department of Energy’s overview of проектирование солнечной фотоэлектрической системы notes that mounting structures support and position PV arrays. Although structural design depends on the project, every mounting system relies on components that fit together according to the approved engineering requirements.
Common manufactured components include:
- С-канальные рельсы
- U-channel profiles
- Каналы со щелевыми стойками
- Z-образные прогоны
- Рельсы для крепления крыши
- Посты наземного обеспечения
- Брекет-члены
- Разъемные пластины
- Module clamps
- Базовые пластины
- Tracker-support components
Джинболида Машина для формовки кронштейнов для солнечных фотоэлектрических систем range includes equipment for producing C-channel, U-channel and related photovoltaic mounting profiles from coil material.
Начните с полной сборки
A bracket should not be evaluated as an isolated component. Its dimensions interact with other parts of the mounting system.
Before production begins, manufacturers should review:
- Bracket drawing
- Mating component drawings
- Fastener sizes
- Connector geometry
- Module clamping zones
- Assembly sequence
- Allowable adjustment
- Structural tolerances
- Coating requirements
- Installation environment
A profile may meet its individual width tolerance but still be difficult to assemble if the connector was designed around a different datum or tolerance condition.
Используйте функциональные данные
Inspection points should relate to how the bracket is assembled.
For example, a hole may be dimensioned from:
- The cut end
- The profile centerline
- One flange
- A previously punched hole
- A formed edge
- A connector reference surface
The datum used in manufacturing should match the drawing. Otherwise, several individually acceptable dimensions may combine into an assembly problem.
Рассмотрим накопление толерантности
A mounting assembly may contain a rail, connector, post and several fasteners. Each part has its own variation.
If every component reaches the same extreme of its permitted tolerance, the combined result may prevent proper alignment. This is known as tolerance accumulation or tolerance stack-up.
Manufacturing teams should therefore identify which dimensions are functionally critical rather than applying the same tolerance to every feature.
1. Последовательные поперечные размеры
The cross-section determines whether a connector, clamp or fastener can enter and seat correctly.
Important dimensions may include:
- Ширина паутины
- Высота фланца
- Длина губы
- Открытие канала
- Радиус изгиба
- Угол изгиба
- Толщина материала
- Глубина раздела
- Slot position relative to the profile
A small dimensional change can affect the way a nut, connector or clamp sits inside the channel.
Открытие канала
For slotted strut and C-channel components, the channel opening must remain consistent. If it is too narrow, a connector nut may not enter or rotate. If it is too wide, the connector may not engage as intended.
Opening variation can result from:
- Incorrect roller gap
- Material-thickness variation
- Спрингбек
- Worn tooling
- Shaft movement
- Incorrect straightening
- Setup changes
The production line should inspect the opening at several positions along the profile, not only at one end.
Размеры фланца и губ
Flanges and lips often provide stiffness or retain internal connectors. Unequal flange dimensions can move the profile centerline and make hole alignment more difficult.
The forming process should produce balanced geometry on both sides where the drawing requires symmetry.
Угол изгиба
Incorrect bend angles may change the effective width and height of the section. A small angular error along a tall flange can create a larger positional difference at the edge.
The roller design should account for material strength, thickness and springback. One setup may not produce the same angle across several different steel grades.
2. Точные положения отверстий и слотов
PV panel mounting brackets often use repeated holes or elongated slots to connect related components. Their positions directly affect assembly speed.
A hole can have the correct diameter but still cause problems if its center is displaced.
Key measurements include:
- Диаметр отверстия
- Ширина слота
- Длина слота
- Расстояние от отверстия до отверстия
- Расстояние от отверстия до края
- Ориентация слота
- Pattern repetition
- Position relative to the formed section
- Position relative to the cut end
Джинболида Оборудование для штамповки солнечных фотоэлектрических стоек includes multi-station systems for producing different mounting-bracket holes, slots and connector features.
Почему используются удлиненные слоты
Elongated slots may provide controlled installation adjustment. However, they should not be treated as a way to hide poor manufacturing accuracy.
Slot dimensions and adjustment direction must follow the engineered connection design. An oversized or incorrectly positioned slot can affect fastener seating and connection performance.
Избегайте кумулятивной ошибки позиционирования
When a long rail contains repeated holes, small feeding errors can accumulate.
Suppose the feeder advances slightly too far at every cycle. The first holes may appear acceptable, but later holes can move progressively away from the intended positions.
Controls may include:
- Сервопитание
- Обратная связь с кодером
- Periodic reference correction
- Non-cumulative programming
- Датчики регистрации
- First-article inspection
- Full-length pattern measurement
The quoted accuracy of one feeder movement is not necessarily the same as the final accuracy over a long profile.
Сопоставьте перфорацию с формовкой
Holes are often produced while the strip is still flat. During roll forming, the strip changes shape and may experience longitudinal or transverse movement.
Tooling engineers must calculate where a hole should be punched on the flat strip so that it reaches the correct final location after forming.
The existing article Солнечная перфорационная машина: встроенная или отдельные системы explains how punching may be connected with or separated from the main forming line.
3. Контролируемая прямолинейность
A long profile can meet its cross-sectional dimensions but remain difficult to install if it is bowed or curved.
Straightness affects whether the profile can:
- Align with adjacent rails
- Sit flat against the supporting structure
- Match repeated fastener locations
- Maintain the intended module position
- Connect without forced adjustment
Straightness variation may appear vertically, horizontally or in both directions.
Причины Лука и Камбера
К числу возможных причин относятся
- Residual coil curvature
- Poor leveling
- Uneven material stress
- Incorrect roller alignment
- Asymmetrical deformation
- Improper cut-off support
- Uncontrolled product handling
A final straightening head can make controlled corrections, but it should not be used to conceal unstable material or incorrectly aligned tooling.
Измерьте по всей длине
Checking only a short section may not reveal gradual curvature.
A defined straightness inspection should state:
- Длина продукта
- Reference surface
- Support method
- Measurement instrument
- Maximum permitted deviation
- Sampling frequency
Longer products may require more inspection points.
4. Ограниченный поворот профиля
Twist occurs when the profile rotates along its longitudinal axis. Even a small rotation can cause mounting surfaces and holes to face different directions at opposite ends.
A twisted rail may require installers to force it into position. This creates additional work and may introduce unwanted stress into the assembled structure.
Общие причины поворота
- Unequal roller gaps
- Off-center strip feeding
- Asymmetrical tooling pressure
- Material-property variation
- Uneven residual stress
- Incorrect straightening
- Poorly supported cutting
- Improper stacking
The investigation should begin at the coil and entry guides, then move through each forming station.
Не судите об поворотах только глазом
A long profile may look straight when viewed from one direction but still rotate along its length.
Twist measurement should use agreed reference surfaces and a defined product length. The same method should be used by the equipment manufacturer, bracket factory and customer.
5. Повторяемая длина реза
Cut length determines whether holes, slots and profile ends align with the installation layout.
A product may contain accurately spaced holes but remain unusable if the cutting system places the end too close to or too far from the final feature.
Положение резки и рисунок отверстий
The control system should coordinate:
- Сервопитание
- Последовательность перфорации
- Длина продукта
- Cut command
- Blade movement
- Material stop or tracking system
If the cutting reference and punching reference use different datums, a cumulative error may appear between the final hole and product end.
Стоп-то-кот и летная отсечка
A stop-to-cut system temporarily stops the profile before cutting. It can provide a straightforward control method but interrupts material movement.
A flying cut-off follows the moving profile. It can support continuous operation but requires accurate synchronization with line speed.
The correct method depends on:
- Геометрия изделия
- Required end condition
- Скорость
- Допуск длины
- Дизайн инструментов
- Объем производства
Поддерживайте профиль во время резки
An unsupported profile may move, rotate or collapse when the cutting tool acts. This can create an angled cut or deform the section near the end.
The cutting die and receiving equipment should support the completed geometry.
6. Очистите отверстие и вырежьте края
Burrs can interfere with fasteners, connectors and manual handling.
Heavy burrs may prevent a bracket from seating flat or make a bolt difficult to insert. They can also damage protective coatings on mating components.
Пробивая заусенцы
Punching burrs are affected by:
- Punch-to-die clearance
- Износ инструмента
- Прочность материала
- Толщина материала
- Tool alignment
- Punch sharpness
- Stripping action
A worn tool may continue producing holes, but the edge quality can deteriorate gradually.
Заусенцы на концах
Cutting burrs can develop from worn blades, unsuitable clearance or unsupported movement.
Inspection should cover:
- Высота заусенца
- Острые края
- Cut squareness
- Деформация торца
- Повреждение покрытия
- Loose metal fragments
If deburring is required, it should be included in production planning rather than left as an uncontrolled manual correction.
Производственные характеристики и эффекты сборки
| Manufacturing feature | Possible deviation | Assembly effect |
|---|---|---|
| Ширина паутины | Too wide or narrow | Connector does not fit correctly |
| Открытие канала | Excessive variation | Nut or clamp cannot engage properly |
| Высота фланца | Unequal sides | Profile centerline moves |
| Угол изгиба | Open or closed angle | Mating surface does not sit flat |
| Диаметр отверстия | Undersized | Fastener cannot pass through |
| Положение отверстия | Offset | Parts require forced alignment |
| Длина слота | Too short | Insufficient designed adjustment |
| Длина разреза | Incorrect | End and hole pattern do not match |
| Прямолинейность | Лук или развал | Rail does not follow the support line |
| Твист | Rotated section | Mounting surfaces misalign |
| Состояние заусенца | Sharp or raised edge | Fastener seating and handling problems |
| Coating surface | Scratched or marked | Surface-quality rejection or corrosion concern |
7. Stable Coating and Surface Condition
PV panel mounting brackets are frequently used outdoors. Their surface condition matters for corrosion protection, appearance and safe handling.
Общие материалы включают:
- Предварительно оцинкованная сталь
- Hot-dip galvanized steel components
- Zinc-aluminum-magnesium-coated steel
- Алюминий
- Нержавеющая сталь
- Painted or powder-coated steel
The manufacturing process should avoid:
- Continuous scratches
- Pressure marks
- Flaking at bends
- Zinc buildup
- Coating damage around holes
- Sharp exposed edges
- Обработка вмятин
- Мокрое окрашивание
For pre-galvanized coil, smooth guides, clean rollers and controlled forming pressure help protect the coated surface. Additional details are covered in the related guide Формирование катушки из оцинкованной стали: как предотвратить повреждение покрытия.
Before publishing, the anchor above should be updated to the final URL assigned to the galvanized steel coil article.
Prevent Damage During Stacking
Profiles should not be dragged across one another. Receiving tables and automatic stackers should support the product without allowing uncontrolled impact.
Stacked galvanized components should be stored in dry, ventilated conditions. Moisture trapped between closely packed surfaces can create staining.
8. Compatibility with Connectors and Fasteners
Dimensional inspection alone may not reveal every assembly issue. A functional fit test should also be performed.
The test can use representative:
- Bolts
- Nuts
- Spring nuts
- Clamps
- Разъемные пластины
- Splice components
- Базовые пластины
- Брекет-члены
Use a Controlled Assembly Fixture
An assembly fixture can reproduce the main connection geometry without building a complete solar array.
A fixture may verify:
- Connector entry
- Bolt insertion
- Hole alignment
- Clamp seating
- Rail-to-rail connection
- Profile orientation
- Splice fit
The fixture should be based on approved drawings and controlled reference components.
Separate Fit from Structural Approval
A successful fit test confirms assembly compatibility, but it does not replace structural analysis or project-specific testing. Load capacity, wind resistance and connection strength must follow the relevant engineering requirements.
9. First-Article and In-Process Inspection
A production line should not wait until the final batch inspection to discover an assembly problem.
Проверка первой статьи
After setup or a product changeover, inspect:
- Complete cross-section
- Углы изгиба
- Hole sizes
- Позиции отверстий
- Длина продукта
- Прямолинейность
- Твист
- Burrs
- Состояние покрытия
- Connector fit
The first article should be approved before continuous production begins.
Внутрипроцессный осмотр
Tool wear, coil changes and temperature variation can affect the process after the first product has passed.
Inspection frequency should consider:
- Скорость производства
- Размер партии
- Износ инструмента
- Вариация материала
- Критические размеры
- Previous defect history
Measurements should also be repeated after:
- Замена катушки
- Замена удара или штампа
- Roll adjustment
- Регулировка выпрямителя
- Cutting-tool change
- Production interruption
- Maintenance work
Окончательная инспекция
Final inspection should confirm:
- Product identity
- Quantity
- Dimensional records
- Состояние поверхности
- Упаковка
- Batch traceability
- Protection during transport
10. Прослеживаемость производства
When assembly problems occur, traceability helps identify whether they relate to material, tooling, setup or a specific production period.
Полезные записи включают в себя
- Coil batch
- Material certificate
- Рецепт продукта
- Machine operator
- Время производства
- Punching tool set
- Forming tool set
- Результаты инспекций
- Техническая деятельность
- Rejected-product reason
Digital production systems can store batch quantities, alarms, material use and inspection information.
Traceability is particularly valuable when the same bracket specification is ordered again months later. The factory can reuse verified settings and compare new material with previous production.
How Roll Forming Equipment Influences Assembly
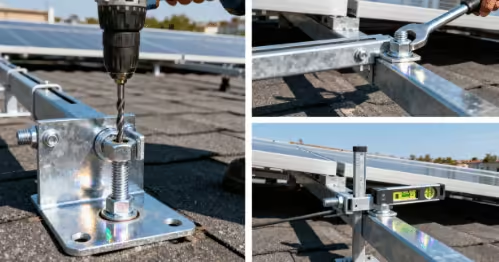
The roll forming machine determines the basic geometry of long photovoltaic profiles.
A suitable system should control:
- Выравнивание полос
- Progressive deformation
- Roller gaps
- Bend sequence
- Спрингбек
- Симметрия профиля
- Прямолинейность
- Cutting coordination
Factories producing different bracket profiles can compare the machine requirements in Солнечная машина для формирования крена монтажного кронштейна: профили C и U.
More Roller Stations Do Not Automatically Mean Better Quality
The forming sequence matters more than the number of stations alone.
Too few stations can create severe deformation and coating stress. Too many unnecessary stations increase setup complexity and machine length.
The roller design should be based on:
- Actual profile
- Свойства материала
- Диапазон толщины
- Required angles
- Состояние поверхности
- Скорость производства
- Tolerances
Adjustable Tooling Needs Repeatable References
When one machine produces several profile sizes, adjustment systems should have measurable reference positions.
К возможным методам относятся
- Calibrated spacers
- Position scales
- Motorized screws
- Servo axes
- Stored recipes
- Replaceable cassettes
Every changeover should be followed by first-article inspection and an assembly fit test where required.
How Punching Equipment Influences Assembly
The punching system determines whether mounting holes and slots appear at the required positions.
A complete evaluation should include:
- Точность сервоподачи
- Encoder calibration
- Зазор инструмента
- Station arrangement
- Удаление слизней
- Время переключения
- Full-length pattern accuracy
- Cutting synchronization
Статья 7 проверок перед добавлением автоматической перфоратора на фотоэлектрическую линию provides a more detailed equipment-integration checklist. Update this internal link to the final published URL when available.
Assembly-Focused Quality Plan
A practical quality plan can divide characteristics according to their effect on installation.
| Control level | Example characteristics | Recommended control |
|---|---|---|
| Критический | Structural connection features | Drawing-based inspection and traceability |
| Assembly-critical | Hole position, channel opening, cut length | First article plus scheduled in-process checks |
| Process-critical | Strip alignment, feeder calibration, roller gap | Setup verification and machine monitoring |
| Surface-critical | Scratches, coating damage, burrs | Visual standard and contact-surface inspection |
| General | Non-functional appearance variation | Defined sampling and acceptance criteria |
The exact classification should be agreed by the product engineering and quality teams.
Common Reasons Brackets Are Difficult to Assemble
Hole Patterns Use the Wrong Datum
The hole dimensions may be individually correct but measured from a different reference than the mating component.
Profile Opening Changes Along the Length
Roller gaps, material thickness or springback may cause the opening to vary.
Straightness Is Checked Only at the Ends
A profile can meet end measurements while curving through the middle.
Twist Is Not Included in Inspection
The rail appears straight from the side but rotates along its length.
Cut Length and Punching Are Not Synchronized
The last hole appears at the wrong distance from the cut end.
Connectors Are Not Included in First-Article Approval
Dimensional inspection passes, but the actual nut or connector does not fit.
Tool Wear Is Detected Too Late
Burrs and hole dimensions gradually deteriorate during a long production batch.
Information Needed Before Designing the Production Line
Manufacturers should provide the equipment supplier with:
- All bracket drawings
- Mating component drawings
- Спецификации материала
- Диапазон толщины
- Coating requirements
- Диапазон длины продукта
- Hole and slot details
- Допуски размеров
- Требование прямолинейности
- Twist requirement
- Expected batch sizes
- Частота переключения
- Целевой выход
- Assembly samples
- Inspection standards
- Планировка завода
This information allows the forming, punching and cutting systems to be evaluated as one production process.
Jinbolida’s existing PV Panel Brackets Production Line Guide provides additional information about the equipment stages used in modern bracket manufacturing.
Заключение
PV panel mounting brackets become easier to assemble when every important dimension is controlled according to its function in the complete mounting system.
Cross-sectional dimensions determine connector fit. Hole and slot positions control fastener alignment. Straightness and twist affect whether long profiles can be installed without force. Cut length determines the relationship between profile ends and punched features. Burr and coating control support safe handling and finished-product quality.
The production line should therefore be designed from the completed assembly backward. Roll forming, servo feeding, punching, cutting, inspection and traceability must work together.
Джинболида поставки фотоэлектрическое оборудование для формирования кронштейнов, multi-station punching systems and automated production-line solutions. Manufacturers can submit bracket drawings, material data, assembly requirements and output targets through the Контактная страница Джинболида for a customized production evaluation.
Часто задаваемые вопросы
Which dimensions matter most for PV panel mounting brackets?
The most important dimensions are those that affect connections: channel opening, web and flange dimensions, bend angles, hole and slot positions, cut length, straightness and twist. The exact priorities depend on the mounting-system design. Manufacturers should identify assembly-critical dimensions with the product engineer before production.
Why do mounting-bracket holes fail to align during installation?
Misalignment can result from servo-feeding error, cumulative pitch error, incorrect drawing datums, strip movement, tool wear or poor synchronization between punching and cutting. The inspection method should measure the complete hole pattern from the agreed functional reference, not only the spacing between two nearby holes.
How does profile twist affect solar-bracket assembly?
Twist rotates the profile along its length, causing mounting surfaces and holes at opposite ends to face different directions. Installers may need to force the rail into position, increasing work and introducing stress. Twist should be measured over a specified length using agreed reference surfaces rather than judged only by appearance.
Are elongated slots enough to compensate for manufacturing variation?
Slots can provide controlled adjustment when included in the engineered connection, but they should not be used to conceal uncontrolled manufacturing errors. Slot length, width, orientation and edge distance must follow the drawing. Excessive variation can still affect fastener seating, connection geometry and structural performance.
How should a factory verify that brackets are easy to assemble?
The factory should combine dimensional inspection with a functional fit test using representative connectors, nuts, bolts, clamps or splice parts. Check first articles after setup and repeat key measurements during production. A controlled assembly fixture can identify compatibility problems before a complete batch reaches installation.
 Russian
 English
 Arabic
 Spanish
 French